For agricultural operations that rely on efficient and reliable handling of potash fertilizer, the potash fertilizer powder conveying system is a critical component. This system is designed to transport bulk potash fertilizer from storage silos or production facilities to application points with precision and minimal loss. The technology behind these systems ensures that the fertilizer remains in a dry, free-flowing state, which is essential for maintaining its effectiveness and preventing caking or clumping. By understanding the working principle and key features of such systems, users can make informed decisions about their material handling needs.
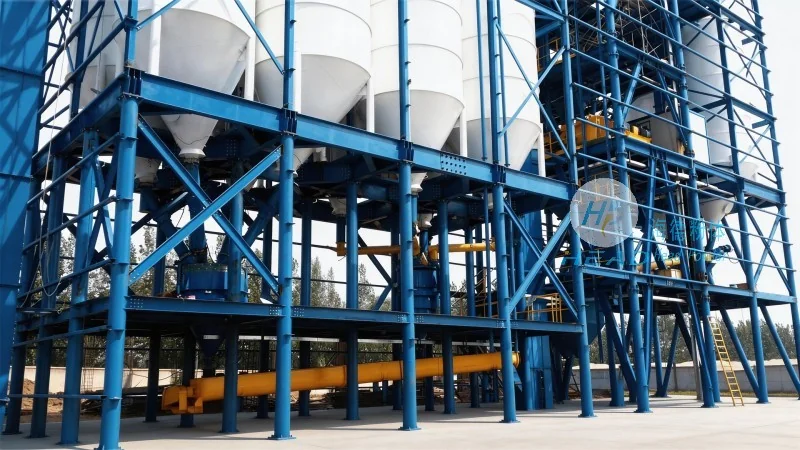
Working Principle of the Potash Fertilizer Powder Conveying System
The core of the potash fertilizer powder conveying system lies in its ability to move dry bulk materials through a network of pipes or hoses using air pressure or mechanical force. The system typically operates on the principle of pneumatic conveying, where compressed air is used to create a flow that propels the fertilizer particles through the system. This method is particularly effective for potash fertilizer, which is a fine powder that can be easily suspended in air. The process begins with the fertilizer being loaded into a hopper or storage container. From there, it is fed into a conveyor line where it is mixed with a controlled amount of air. The air-fertilizer mixture is then transported through the pipeline system to the desired destination, such as a spreader or storage tank. The system may include components like rotary valves, airlocks, and filters to ensure a smooth and continuous flow. The air pressure is carefully regulated to maintain the right velocity for the particles, preventing them from settling or causing blockages. This controlled air flow also helps in maintaining the quality of the fertilizer by keeping it dry and preventing moisture absorption, which could lead to degradation or caking.
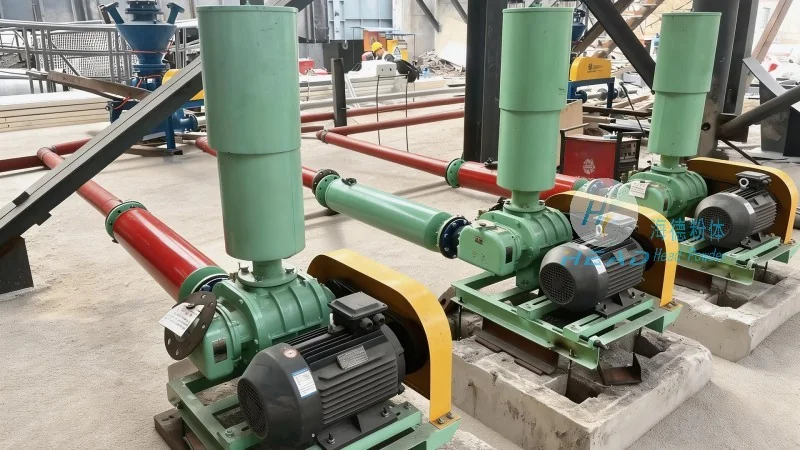
Key Features of the Potash Fertilizer Powder Conveying System
Several key features distinguish the potash fertilizer powder conveying system from other material handling solutions. First, the system is designed for high efficiency in transporting large volumes of fertilizer with minimal energy consumption. The pneumatic conveying method allows for a continuous flow, reducing the need for manual handling and improving operational safety. Second, the system is highly adaptable to different application scenarios, from small-scale farm operations to large industrial facilities. It can be customized with different pipe sizes, lengths, and components to suit specific site requirements. Third, the system is built with durability and reliability in mind, using materials that can withstand the corrosive nature of potash fertilizer and the rigors of continuous operation. This includes the use of stainless steel or other corrosion-resistant materials for the conveyor components. Fourth, the system incorporates advanced control systems that allow for real-time monitoring and adjustment of the conveying process. This ensures that the flow rate, pressure, and temperature are maintained within optimal parameters, preventing issues like overloading or air leaks. Additionally, the system is designed to minimize dust emissions, which is important for environmental compliance and worker safety. The use of sealed containers and efficient filtration systems helps in keeping the environment clean and reducing the risk of respiratory issues associated with handling fine powders.
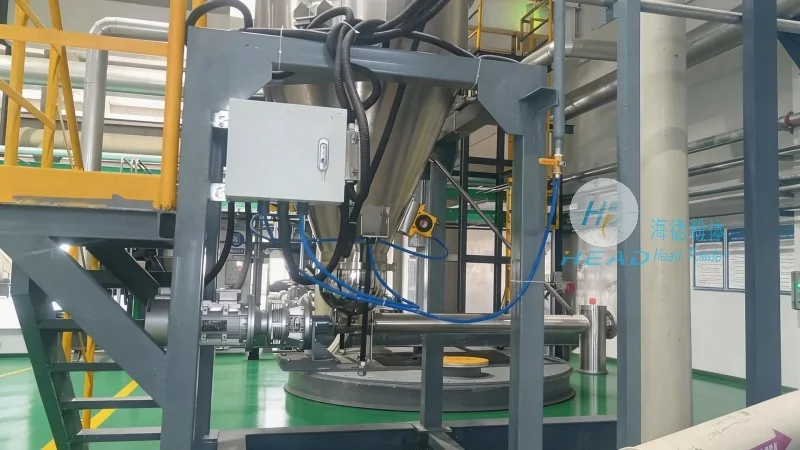
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in designing and supplying high-quality potash fertilizer powder conveying systems. With years of experience in the industry, the company has developed a reputation for producing reliable and efficient equipment that meets the needs of agricultural and industrial clients. HeadPowder's systems are engineered to handle the unique challenges of potash fertilizer, such as its fine particle size and potential for caking. The company's commitment to quality is reflected in its use of advanced materials and rigorous testing processes. HeadPowder's facilities are located in Shandong, China, where the company has a strong presence in the regional market. The company's team of engineers and technicians work closely with clients to understand their specific requirements and provide tailored solutions that enhance operational efficiency and reduce costs. By choosing HeadPowder's potash fertilizer powder conveying systems, clients can benefit from improved productivity, reduced downtime, and enhanced safety in their material handling operations.




