HeadPowder Engineering Co., Ltd., a leading provider in the field of powder handling technology, specializes in the design and implementation of advanced sugar powder conveying systems. With a strong presence in Shandong, China, the company has established itself as a trusted partner for industries requiring reliable and efficient bulk material transport solutions. This article delves into the working principle and key characteristics of such systems, offering insights into how they enhance operational efficiency and product quality in sugar processing applications.
Working Principle of Sugar Powder Conveying Systems
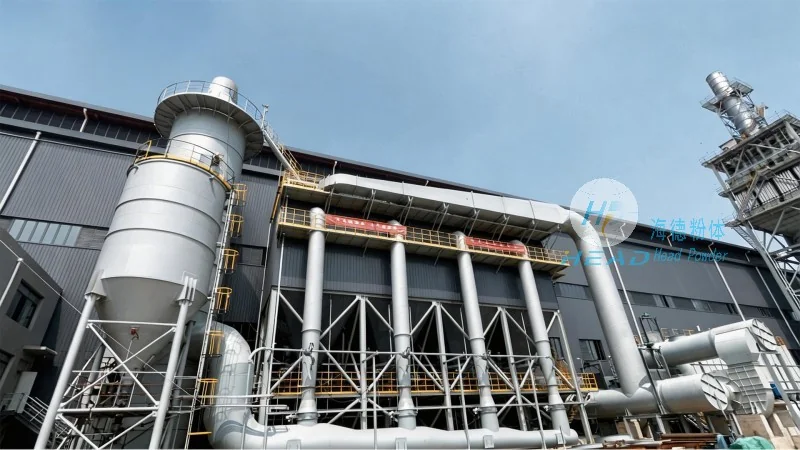
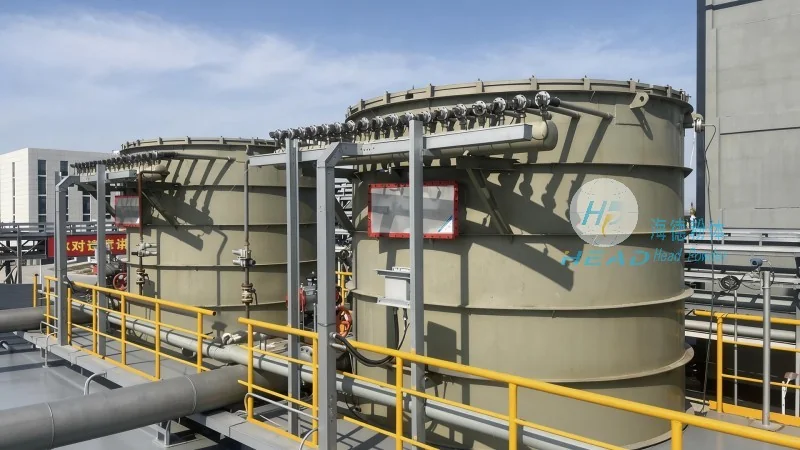
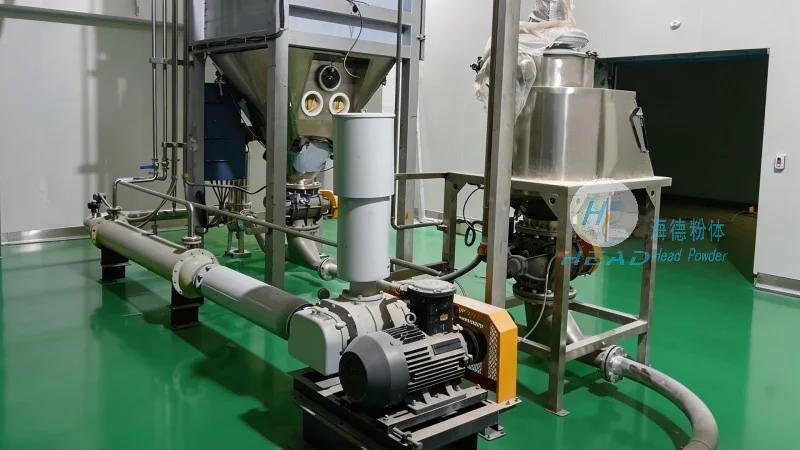
The core of a sugar powder conveying system lies in its ability to transport granular or powdered materials, such as sugar, from one location to another with precision and minimal loss. The system typically operates through a combination of mechanical components and control mechanisms that work in tandem to ensure smooth and consistent flow. At the heart of the system is the conveyor itself, which may include screw conveyors, pneumatic conveyors, or belt conveyors, depending on the specific requirements of the application. For sugar powder, which is often hygroscopic and requires careful handling, a screw conveyor is commonly used due to its ability to maintain product integrity and prevent segregation. The screw conveyor consists of a rotating helical screw within a cylindrical tube, which pulls the powder forward through the system. This mechanism is complemented by a series of control valves, sensors, and a central control unit that monitors and adjusts the flow rate, pressure, and temperature as needed. The control unit may be integrated with a programmable logic controller (PLC) or a more advanced digital control system, allowing for real-time adjustments based on process parameters. Additionally, the system may incorporate dust collection and filtration components to maintain air quality and prevent product contamination, which is crucial for sugar products that are sensitive to moisture and impurities. The entire process is designed to be automated, reducing the need for manual intervention and minimizing the risk of human error. The working principle thus involves a seamless integration of mechanical transport, precise control, and environmental management to achieve efficient and reliable powder handling.
Key Features of the Sugar Powder Conveying System
HeadPowder Engineering Co., Ltd.'s sugar powder conveying systems are characterized by several key features that set them apart in the industry. Firstly, the systems are engineered for high efficiency, ensuring that the conveying process is both rapid and energy-efficient. This is achieved through optimized screw designs and variable speed drives that adjust the conveyor speed based on the material load and required flow rate. The result is a system that minimizes energy consumption while maximizing throughput, making it cost-effective for large-scale sugar processing operations. Secondly, the systems are built for durability and reliability, using high-quality materials such as stainless steel and corrosion-resistant components to withstand the harsh conditions of sugar processing environments. This durability ensures long service life and reduces maintenance costs, which is a critical consideration for industrial applications. Thirdly, the systems are designed with product integrity in mind. The enclosed conveyor design prevents exposure to air and moisture, which helps maintain the quality and freshness of the sugar powder. Additionally, the system includes features such as airlocks and sealing mechanisms to prevent product leakage and cross-contamination, ensuring that the final product meets the highest standards of purity and quality. Fourthly, the systems offer flexibility and adaptability, allowing for customization to suit different production needs. Whether the application requires horizontal or vertical transport, or involves multiple stages of processing, the system can be configured to meet the specific requirements. This flexibility makes the system suitable for a wide range of sugar processing facilities, from small-scale operations to large industrial plants. Finally, the systems are equipped with advanced monitoring and diagnostic tools that provide real-time data on system performance. These tools include sensors for temperature, pressure, and flow rate, as well as alarms and alerts for any deviations from normal operation. This allows for proactive maintenance and quick troubleshooting, minimizing downtime and ensuring continuous operation. Overall, the key features of the system reflect a commitment to excellence in design, functionality, and user experience, making it an ideal solution for sugar powder handling in various industrial settings.
Conclusion
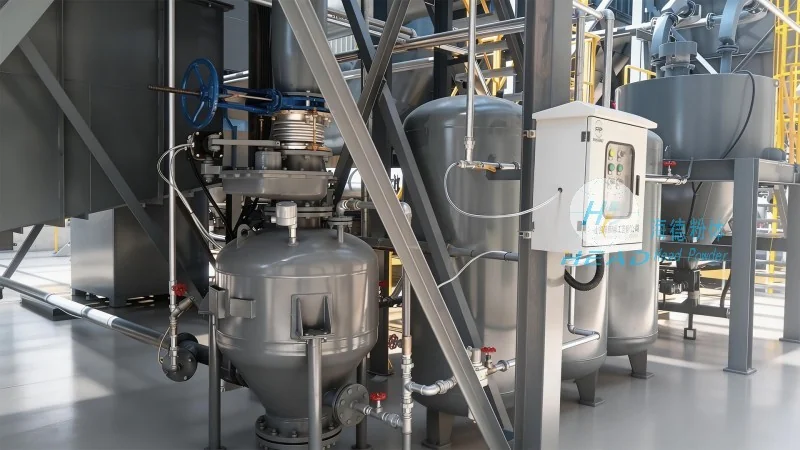
HeadPowder Engineering Co., Ltd.'s sugar powder conveying systems represent a sophisticated solution for the efficient and reliable transport of sugar powder. By integrating advanced mechanical design, precise control technology, and robust construction, the system addresses the unique challenges of sugar processing, such as maintaining product quality and ensuring operational efficiency. With its high efficiency, durability, and adaptability, the system is well-suited for a wide range of applications, from small-scale production to large industrial operations. As a company based in Shandong, China, HeadPowder Engineering Co., Ltd. continues to innovate and provide cutting-edge solutions that meet the evolving needs of the industry. The working principle and key features of the system underscore its effectiveness in enhancing productivity and product quality in sugar processing, making it a valuable asset for any facility handling bulk sugar powder.




