Urea powder handling systems are critical components in industrial processes where the efficient and safe transport of urea, a key agricultural and industrial fertilizer, is required. These systems are designed to manage the flow, storage, and distribution of urea powder, ensuring optimal performance and reliability in various applications.
Working Principle of Urea Powder Handling Systems
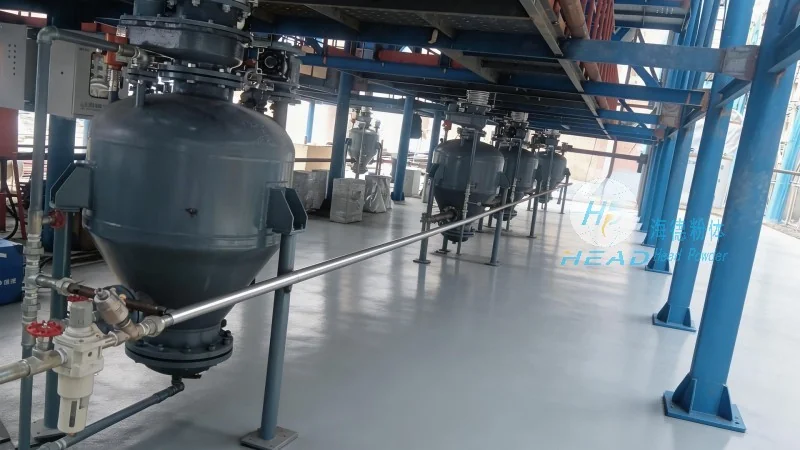
The core working principle of a urea powder handling system involves several integrated steps to ensure the seamless movement of urea from storage to end-use. The process typically begins with the storage of urea in bulk silos or containers. From there, the system uses a combination of equipment such as feeders, conveyors, and pneumatic or mechanical transport mechanisms to move the urea. Feeders, often rotary or vibratory types, regulate the flow rate of urea from the storage silo to the conveyor system. The conveyor, which can be a belt conveyor, screw conveyor, or pneumatic conveyor, then transports the urea to the processing or packaging area. Pneumatic conveying systems, in particular, use compressed air to create a flow of urea particles through pipes, allowing for long-distance transport with minimal maintenance. The entire system is controlled by a centralized control panel that monitors and adjusts parameters like pressure, flow rate, and temperature to maintain optimal operation. This integrated approach ensures that the urea is handled efficiently, with minimal risk of caking or degradation, which is crucial for maintaining product quality.
Key Features of Urea Powder Handling Systems
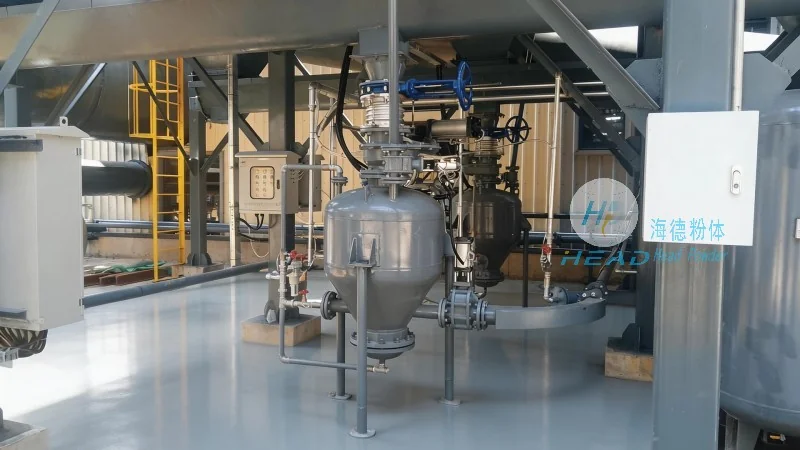
Urea powder handling systems are characterized by several key features that enhance their performance and reliability. One of the primary features is the ability to handle large volumes of urea efficiently, with systems designed to process up to several thousand tons per hour in industrial settings. The systems are also equipped with advanced control technologies, including PLC (Programmable Logic Controller) systems, which allow for precise regulation of the flow and pressure within the system. This ensures consistent product quality and reduces the risk of overloading or underflow. Another important feature is the integration of safety mechanisms, such as pressure relief valves and dust suppression systems, to prevent accidents and comply with industrial safety standards. The systems are also designed for easy maintenance, with modular components that can be replaced or serviced without disrupting the entire operation. Additionally, modern urea powder handling systems are equipped with monitoring and diagnostic tools that provide real-time data on system performance, allowing for proactive maintenance and troubleshooting. These features collectively contribute to the high efficiency, reliability, and safety of urea powder handling systems, making them essential in industries where urea is a primary product.
About Shandong HeadPowder Engineering Co., Ltd.
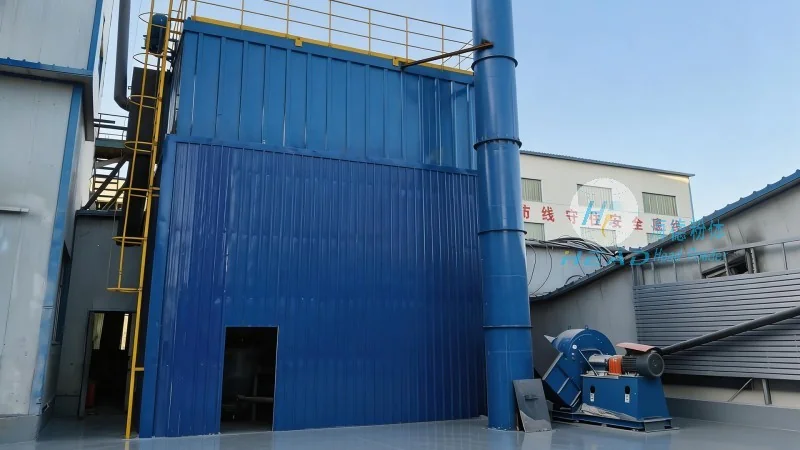
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of powder handling systems, specializes in the design, manufacturing, and installation of advanced urea powder handling solutions. With a strong focus on innovation and quality, the company has established itself as a trusted partner for industries requiring reliable and efficient urea handling systems. HeadPowder's systems are engineered to meet the specific needs of clients, ensuring optimal performance in various operational conditions. The company's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering high-quality products that meet international standards. HeadPowder's facilities are located in Shandong, China, where the company leverages its local expertise and resources to provide comprehensive support to its clients worldwide.




