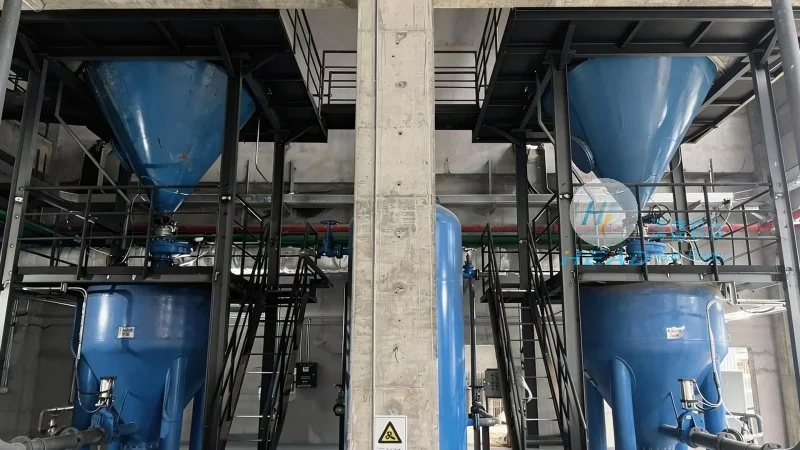
Pharmaceutical powder handling equipment is a critical component in the pharmaceutical manufacturing process, ensuring the safe, efficient, and controlled transfer of powders from one stage to another. This equipment is essential for maintaining product quality, consistency, and compliance with regulatory standards. The design and operation of these systems are tailored to meet the stringent requirements of the pharmaceutical industry, where precision and reliability are paramount.
Introduction to Pharmaceutical Powder Handling Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced pharmaceutical powder handling solutions. The company's equipment is engineered to address the unique challenges of powder processing in pharmaceutical applications, such as maintaining particle integrity, preventing contamination, and ensuring consistent flow rates. With a focus on innovation and quality, HeadPowder provides tailored solutions that enhance operational efficiency and product safety.
Working Principles of Pharmaceutical Powder Transport Systems
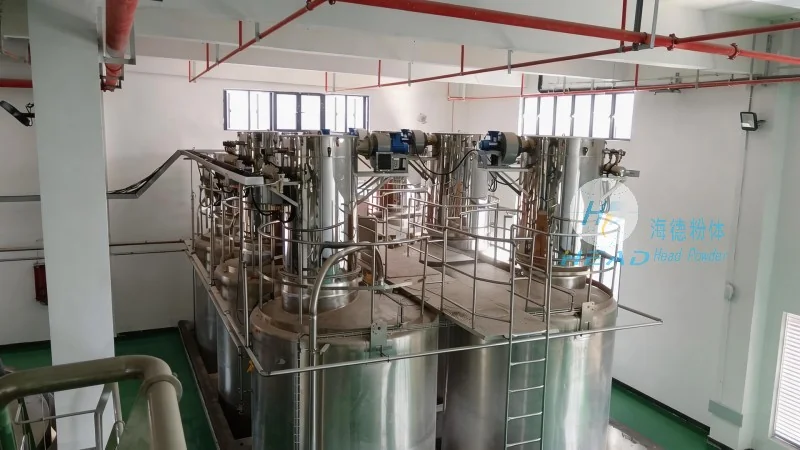
The core working principle of pharmaceutical powder handling equipment revolves around the efficient transfer of powders through various mechanisms. Common methods include pneumatic conveying, mechanical conveying, and vacuum systems, each tailored to specific powder characteristics and process requirements. Pneumatic conveying systems utilize air or gas to move powders through pipelines, leveraging pressure differentials to transport materials. Mechanical conveying, such as screw conveyors and belt conveyors, relies on mechanical components to move powders through enclosed or open channels. Vacuum systems, on the other hand, use suction to draw powders into collection or processing areas. The selection of a specific conveying method depends on factors like powder density, flowability, and the need for containment or dust control.
Key Features of Pharmaceutical Powder Handling Equipment
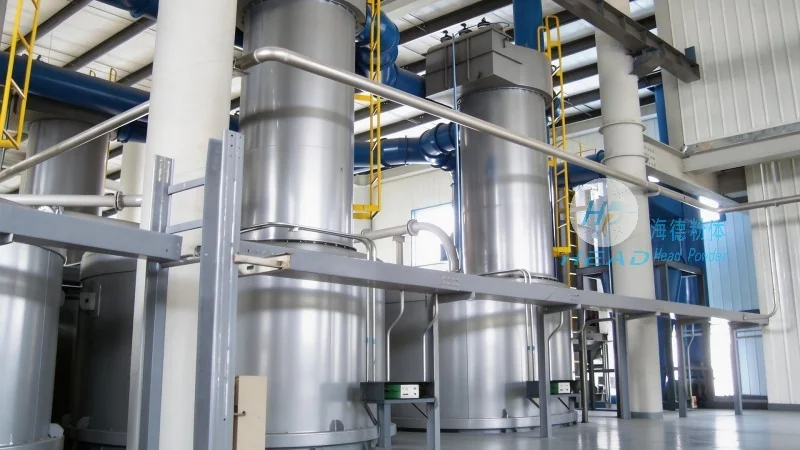
Pharmaceutical powder handling equipment from Shandong HeadPowder Engineering Co., Ltd. is characterized by several key features that distinguish it from conventional industrial equipment. Firstly, these systems are designed with strict adherence to GMP (Good Manufacturing Practice) standards, ensuring that all components are constructed from materials that are non-reactive, easy to clean, and resistant to contamination. This includes the use of stainless steel, PTFE-coated surfaces, and other hygienic materials that meet regulatory requirements. Secondly, the equipment offers precise control over powder flow rates, which is critical for maintaining consistent dosages and preventing overloading or underloading of processing equipment. Advanced control systems, often integrated with sensors and feedback mechanisms, allow operators to adjust flow rates in real-time, ensuring optimal performance. Thirdly, the equipment is engineered for low product loss and minimal particle degradation. This is achieved through gentle handling mechanisms, such as low-speed augers or smooth, non-abrasive surfaces, which prevent attrition and agglomeration of powders. Additionally, many systems incorporate dust suppression and containment features, such as closed-loop designs and filtration, to minimize environmental impact and ensure operator safety. The equipment also offers flexibility in terms of integration with other processing equipment, allowing seamless integration into existing production lines without disrupting workflow.
Applications and Benefits in Pharmaceutical Manufacturing
The application of pharmaceutical powder handling equipment is widespread across various stages of the pharmaceutical manufacturing process. In the raw material handling stage, these systems are used to transfer raw powders from storage silos to processing units, ensuring that materials are delivered in a controlled manner. During the formulation stage, the equipment facilitates the precise mixing of active pharmaceutical ingredients (APIs) with excipients, maintaining uniformity in the final product. In the packaging stage, powder handling systems ensure that the correct dosage is dispensed into containers, reducing errors and improving product consistency. The benefits of using advanced powder handling equipment extend beyond operational efficiency. By minimizing product loss and contamination, these systems help reduce waste and improve overall product quality. Additionally, the precise control over flow rates and the hygienic design of the equipment contribute to regulatory compliance, reducing the risk of non-compliance and associated penalties. The use of automated control systems also enhances operational safety by minimizing human intervention in potentially hazardous powder handling processes.
Conclusion
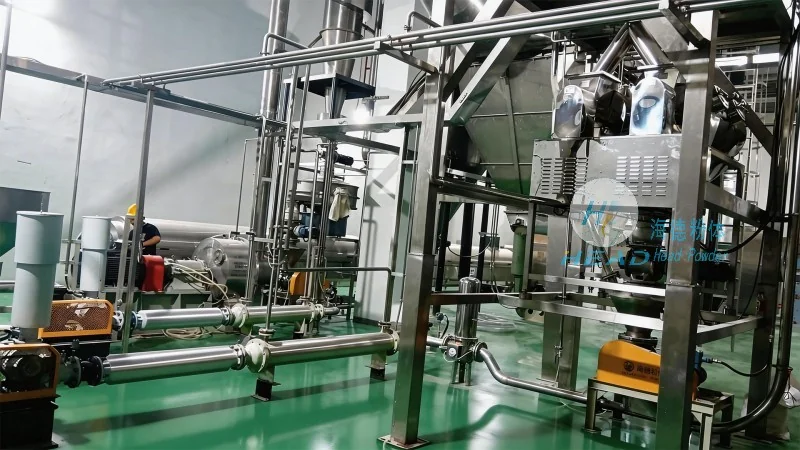
Pharmaceutical powder handling equipment from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the challenges of powder processing in the pharmaceutical industry. By combining advanced engineering principles with strict adherence to regulatory standards, these systems ensure the safe, efficient, and reliable transfer of powders throughout the manufacturing process. The working principles and features of these equipment, such as pneumatic conveying, precise flow control, and hygienic design, are tailored to meet the unique demands of pharmaceutical applications. As the pharmaceutical industry continues to evolve, the importance of reliable powder handling equipment will only increase, making it a critical investment for manufacturers seeking to maintain quality, compliance, and operational excellence.




