Intelligent tonne bag loading stations equipped with powder conveying equipment are essential for efficient handling of bulk powder materials in industrial settings. These systems are designed to streamline the process of receiving, transferring, and managing powder from large tonne bags, ensuring a seamless workflow from arrival to processing. The technology behind such equipment is tailored to meet the demands of modern manufacturing, where reliability and precision are critical.
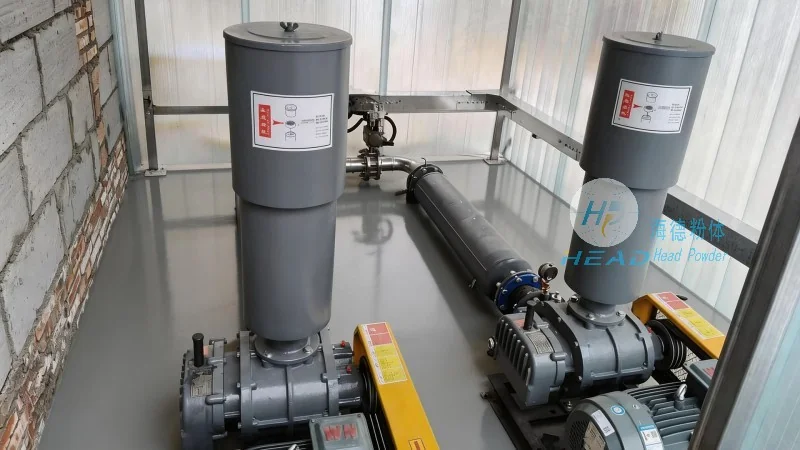
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced powder handling solutions. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries requiring robust and efficient powder conveying systems. The company’s headquarters and primary operations are located in Shandong, providing a strategic base for serving clients across the region and beyond.
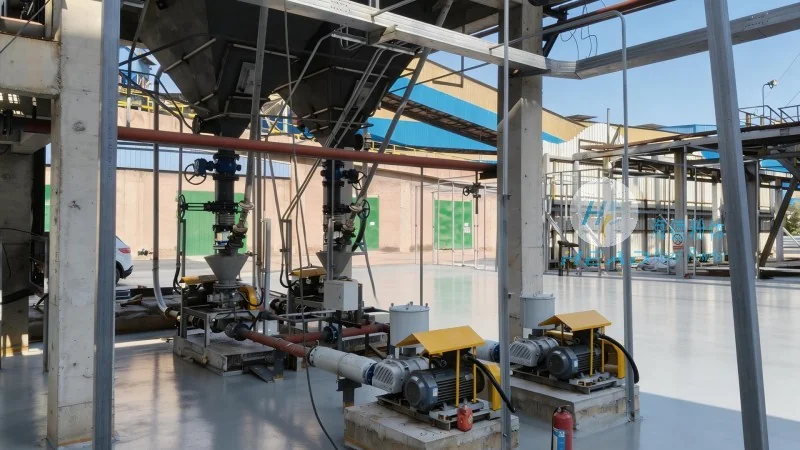
Working Principle of the Intelligent Tonne Bag Loading Station
The intelligent tonne bag loading station operates through a series of automated steps that ensure optimal performance and minimal human intervention. The process begins with the arrival of a tonne bag, which is then positioned on a dedicated loading platform. A mechanical system, typically consisting of a hopper and a discharge valve, is activated to open the bag and allow the powder to flow into the hopper. The equipment is equipped with sensors and control systems that monitor the flow rate and volume, ensuring accurate measurement and transfer. Once the powder is fully transferred, the system automatically closes the discharge valve and prepares the hopper for the next bag. This automated sequence minimizes downtime and maximizes throughput, making it ideal for high-volume production environments. The system also includes a dust collection and filtration unit to maintain a clean and safe working environment, which is crucial for industries where powder handling must comply with strict safety regulations.
Key Features of the Powder Conveying Equipment
The powder conveying equipment integrated with the tonne bag loading station offers several distinctive features that enhance its functionality and reliability. Firstly, the system incorporates advanced level sensors and weight measurement technology, which provide real-time monitoring of the material level in the hopper and the exact quantity of powder transferred. This ensures precise control over the conveying process, reducing material loss and preventing overfilling or underfilling. Secondly, the equipment is designed with a robust and durable construction, capable of handling a wide range of powder types, including fine powders, granules, and bulk materials. The use of high-quality materials and precision engineering ensures long-term performance and minimal maintenance requirements. Thirdly, the system is equipped with an automated control panel that allows for easy operation and adjustment, enabling operators to customize the conveying parameters according to specific production needs. The control panel features user-friendly interfaces and intuitive controls, reducing the learning curve for new operators. Additionally, the equipment is designed with safety features such as emergency stop buttons and overload protection, ensuring a secure working environment. The system also includes a self-diagnostic function that alerts operators to any potential issues, allowing for timely maintenance and preventing unexpected downtime.
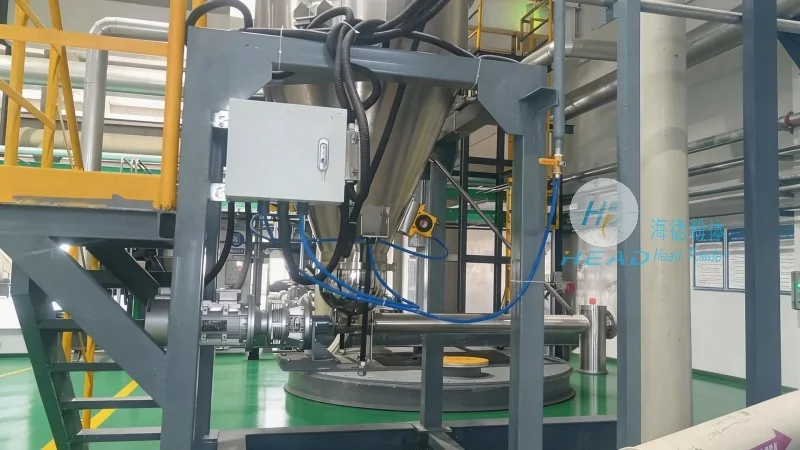
Benefits and Applications
The intelligent tonne bag loading station and powder conveying equipment offer numerous benefits to industries that rely on bulk powder handling. The primary advantage is the significant improvement in operational efficiency, as the automated process reduces the time and labor required for manual handling. This leads to increased production capacity and reduced costs. The equipment also enhances product quality by minimizing material contamination and ensuring consistent powder flow. Furthermore, the system’s adaptability allows it to be integrated into existing production lines, making it a versatile solution for various applications. Industries such as pharmaceuticals, food processing, chemical manufacturing, and mining can all benefit from the reliable and efficient performance of this equipment.




