Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the material handling industry, specializes in the design and production of efficient systems for conveying shredded paper materials. This article provides a detailed overview of the working principle and key features of such systems, highlighting their importance in modern waste management and recycling processes.
Working Principle of Shredded Paper Material Conveying Systems
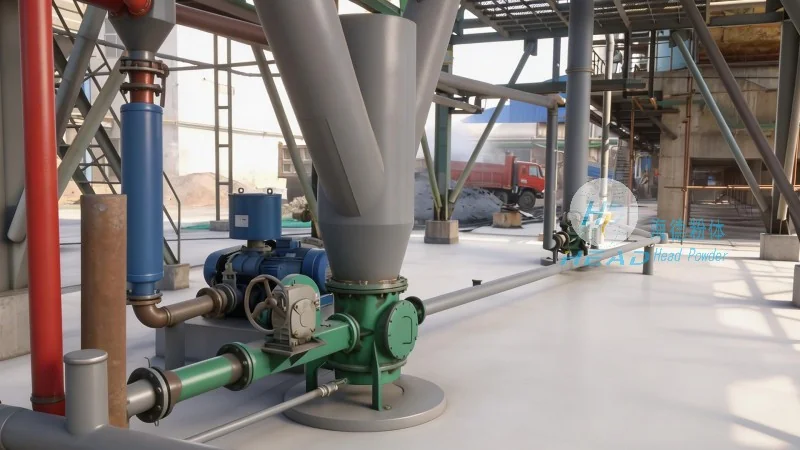
The core working principle of shredded paper material conveying systems involves the use of specialized equipment to transport shredded paper from one location to another within a facility or between different processing stages. These systems typically consist of components such as feed hoppers, conveyor belts or rollers, control mechanisms, and discharge units. The process begins when shredded paper is loaded into the feed hopper. From there, the material is transferred to the conveyor system, which moves it through the system using mechanical force, often in combination with gravity or auxiliary power. Control mechanisms ensure the smooth operation of the conveyor, regulating the speed and direction of material flow. Finally, the shredded paper is discharged at the end of the system, ready for further processing or disposal.
Key Features of Shredded Paper Material Conveying Systems
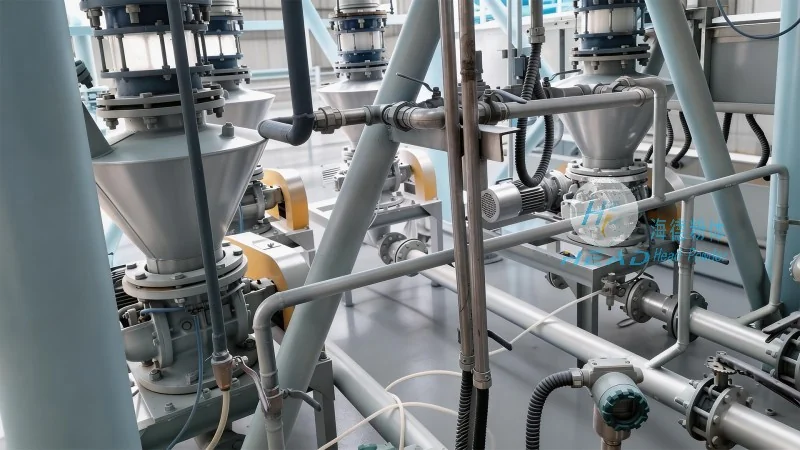
Shredded paper material conveying systems are designed with several key features that enhance their efficiency and reliability. One of the primary features is the ability to handle large volumes of material with minimal maintenance. The robust construction of these systems, often using durable materials like stainless steel or heavy-duty plastics, ensures long-term performance even under heavy operational loads. Another important feature is the adjustable speed and capacity, allowing users to customize the system to meet specific production requirements. Additionally, these systems are equipped with safety features, such as emergency stop buttons and overload protection, to prevent accidents and ensure operator safety. The modular design of many systems also facilitates easy integration with existing facilities and allows for future expansion as needed.
Application and Benefits in Waste Management
Shredded paper material conveying systems play a crucial role in the waste management and recycling industry. By efficiently transporting shredded paper, these systems help streamline the processing of paper waste, reducing the time and labor required for manual handling. This not only improves operational efficiency but also contributes to cost savings for businesses. Furthermore, the consistent and controlled movement of material reduces the risk of jams or blockages, which can be common in traditional manual handling methods. The use of automated conveying systems also promotes a cleaner and safer working environment, as operators are less exposed to heavy lifting and manual sorting tasks.
Technical Specifications and Customization Options
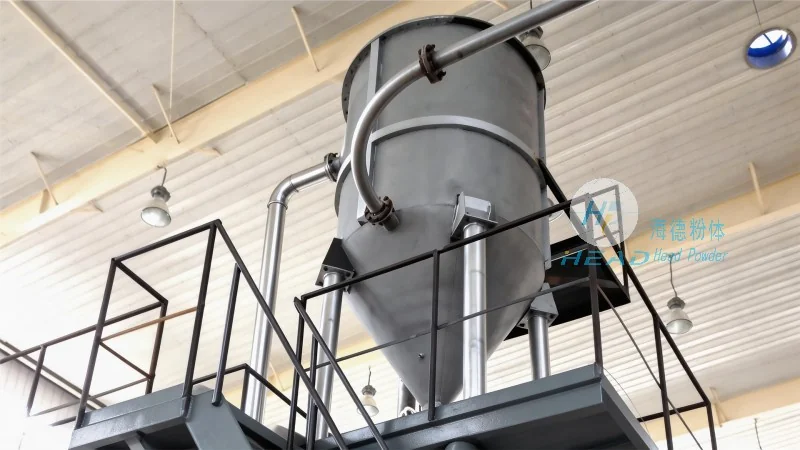
Shandong HeadPowder Engineering Co., Ltd. offers a range of shredded paper material conveying systems with customizable technical specifications to suit various applications. These systems can be tailored in terms of conveyor length, width, and speed to accommodate different volumes of shredded paper. The company also provides options for different types of conveying mechanisms, including belt conveyors, screw conveyors, and chain conveyors, depending on the specific requirements of the user. Additionally, the systems can be equipped with sensors and monitoring devices to provide real-time data on material flow and system performance, enabling proactive maintenance and optimization.




