For industries seeking efficient and reliable material handling solutions, vacuum material conveying systems offer a versatile approach to transporting bulk materials. This article explores the fundamental working principle and key characteristics of vacuum material handling conveying lines, highlighting how they enhance operational efficiency and product integrity in various industrial applications.
Understanding the Working Principle of Vacuum Material Conveying Systems
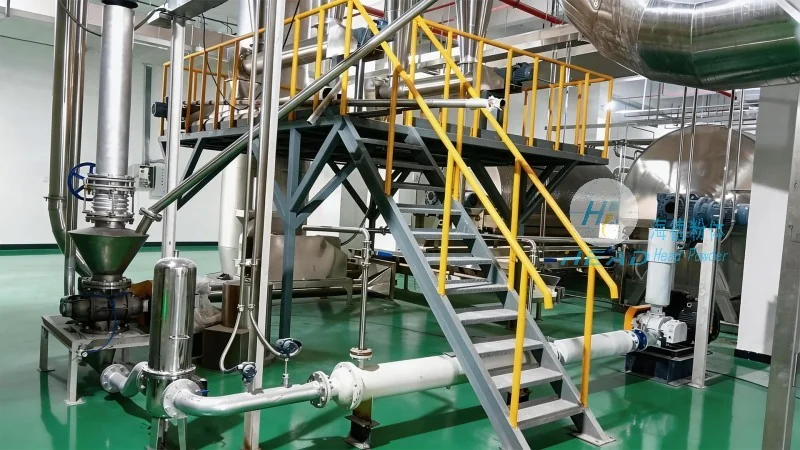
The core mechanism of vacuum material conveying lines relies on the creation of a pressure differential between the material source and the receiving point. By generating a negative pressure (vacuum) at the inlet, the system draws material particles into the conveying tube. This process typically involves a combination of suction and pressure control to ensure consistent material flow. The vacuum is maintained by a vacuum pump, which extracts air and material particles from the system, while the material is transported through the pipeline to the discharge point. The system often incorporates components such as a hopper for material collection, a filter to separate particles from air, and a control valve to regulate the flow rate. This mechanism allows for the seamless transfer of dry, free-flowing materials like powders, granules, and small particles without the need for mechanical contact, reducing wear and maintenance costs.
Key Features of Vacuum Material Handling Conveying Lines
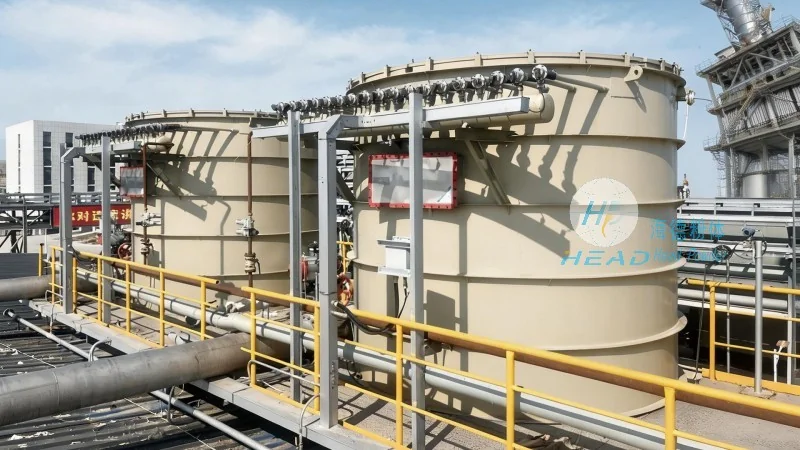
Vacuum material conveying systems are distinguished by several advantageous features that make them suitable for diverse industrial needs. Firstly, they provide a dust-free and clean transfer process, which is critical for maintaining product quality and compliance with environmental regulations. The enclosed pipeline design prevents material spillage and contamination, ensuring a hygienic handling environment. Secondly, these systems offer flexibility in layout, as the conveying lines can be installed in various configurations, including vertical, horizontal, or inclined paths, adapting to the spatial constraints of different facilities. This adaptability allows for customized solutions tailored to specific production requirements. Thirdly, vacuum conveying is energy-efficient compared to other bulk material handling methods, as it minimizes energy consumption by using a vacuum pump rather than mechanical force to move materials. Additionally, the system reduces product degradation by avoiding high-speed impacts or friction, which can damage sensitive materials. The modular design of vacuum conveying systems also facilitates easy maintenance and component replacement, extending the operational lifespan of the equipment.
Applications and Benefits in Industrial Settings
The versatility of vacuum material handling conveying lines makes them indispensable in numerous industries, including pharmaceuticals, food processing, chemical manufacturing, and powder coating. In pharmaceutical applications, the dust-free and hygienic nature of the system ensures compliance with stringent quality standards, preventing cross-contamination and maintaining product purity. Similarly, in food processing, the enclosed design protects food products from environmental contaminants and microbial growth, while the gentle handling minimizes product damage. Chemical manufacturers benefit from the system's ability to handle hazardous materials safely, as the sealed pipeline prevents exposure to workers and the environment. The efficiency and reliability of vacuum conveying also contribute to increased production throughput, reduced downtime, and lower operational costs, making it a preferred choice for industries focused on optimizing material handling processes.
Conclusion and Company Overview
Vacuum material handling conveying lines represent a sophisticated solution for efficient bulk material transport, combining advanced technology with practical design to meet the demands of modern industrial operations. The working principle, centered on pressure differential and enclosed transport, ensures reliable and clean material movement, while the key features—such as dust-free operation, flexibility, and energy efficiency—enhance overall performance and user experience. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized vacuum conveying systems tailored to the unique needs of various industries. With a commitment to quality and innovation, the company delivers solutions that improve operational efficiency, product quality, and environmental compliance. Based in Shandong, China, HeadPowder Engineering Co., Ltd. leverages its expertise to support businesses in achieving their material handling goals, providing reliable and effective solutions for a wide range of applications.




