HeadPowder, a leading provider of industrial conveying solutions, specializes in equipment designed for the efficient handling of silicate powders. This article explores the fundamental principles behind silicate powder conveyors and highlights the key characteristics that define their performance in various industrial applications.
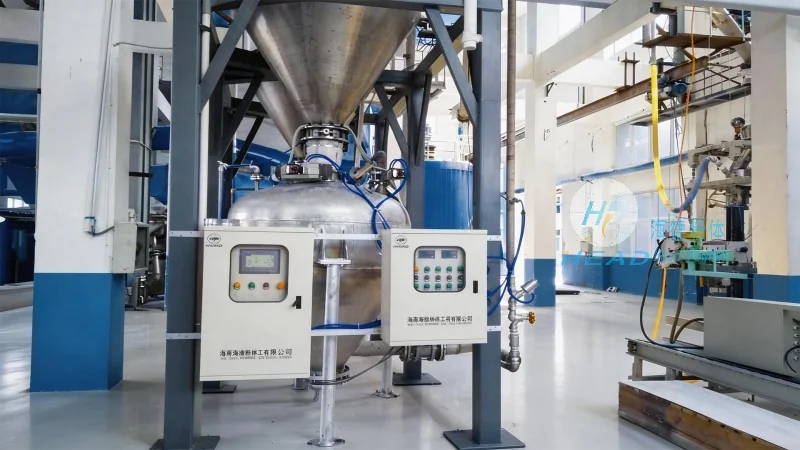
Introduction to Silicate Powder Conveying Equipment
Silicate powder conveying equipment is engineered to transport fine or bulk powders that are derived from silicate materials, such as those used in cement, ceramics, and glass production. These systems are critical in manufacturing processes where consistent and reliable material flow is essential for maintaining production efficiency and product quality. The design of silicate powder conveyors must account for the unique properties of silicate powders, including their particle size, moisture content, and potential for caking or abrasiveness.
Principle of Silicate Powder Conveyors
The core principle of silicate powder conveyors revolves around the mechanical or pneumatic movement of powder particles. Mechanical conveyors, like screw conveyors, utilize rotating helical screws to push powders forward through a closed tube or trough. This method is particularly effective for handling dry, free-flowing silicate powders and offers advantages such as low maintenance and the ability to operate in vertical or inclined configurations. Pneumatic conveyors, on the other hand, employ compressed air to create a flow of material through a pipeline. This approach is ideal for transporting fine powders over longer distances or in environments where dust containment is a priority. Both types of systems are designed to minimize material degradation and ensure consistent delivery to downstream processes.
Working Scene Characteristics of Silicate Powder Conveyors
The working scene characteristics of silicate powder conveyors are tailored to the specific demands of industrial environments. These systems are typically installed in manufacturing facilities where silicate powders are processed, such as cement plants, ceramic factories, and glass production lines. The equipment is often integrated into larger production lines, working in tandem with other machinery like mixers, crushers, and kilns. The characteristics that define their performance in these scenes include high throughput capacity, durability against abrasive materials, and the ability to handle varying powder compositions without compromising efficiency. Additionally, modern silicate powder conveyors are equipped with advanced control systems that allow for real-time monitoring and adjustment of conveying parameters, ensuring optimal operation under different production conditions.
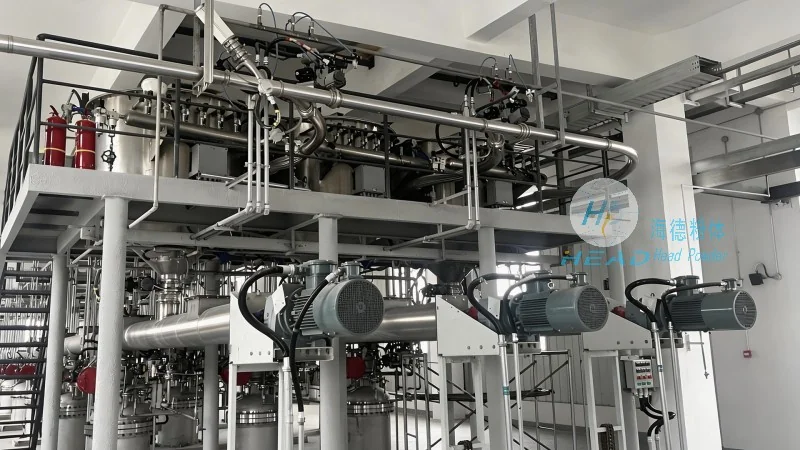
Application in the Cement Industry
In the cement industry, silicate powder conveyors play a vital role in the transportation of raw materials and finished products. Raw materials such as limestone, clay, and iron ore are often in the form of fine powders and require efficient conveyance to the kiln. The conveying systems must be capable of handling high volumes of material while maintaining low energy consumption. Moreover, the equipment must be resistant to the high temperatures and abrasive nature of the materials, ensuring long service life and minimal downtime. HeadPowder's silicate powder conveyors are specifically designed to meet these challenges, featuring wear-resistant components and robust construction that are essential for continuous operation in cement production.
Application in Ceramic Manufacturing
Ceramic manufacturing relies heavily on the precise handling of silicate powders, including clays, feldspars, and silica sands. These materials are often processed into fine powders that require careful transportation to mixing and molding equipment. The silicate powder conveyors used in ceramic plants must be able to maintain the integrity of the powder, preventing agglomeration or degradation that could affect the final product quality. The systems are typically designed with gentle handling mechanisms, such as low-speed screw conveyors or air slides, to minimize particle breakage. Furthermore, the conveyors are integrated with dust collection systems to ensure a clean and safe working environment, which is critical in ceramic production facilities.
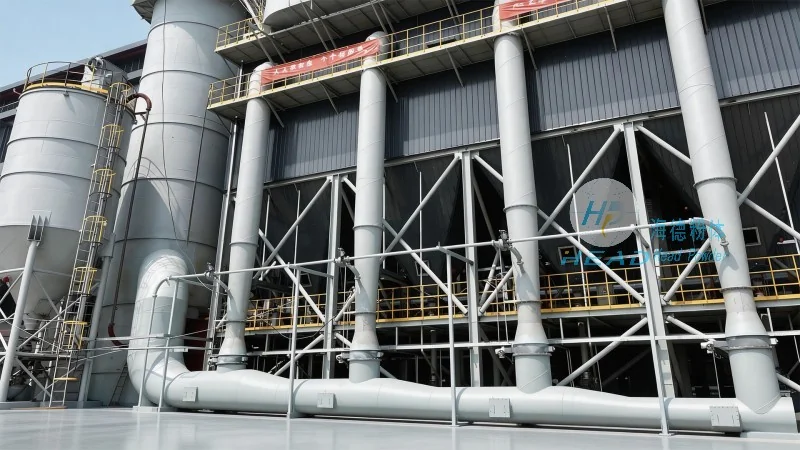
Application in Glass Processing
For glass processing, silicate powder conveyors are used to transport raw materials like quartz sand, soda ash, and limestone. These powders are often high in purity and require strict control over moisture and particle size to ensure the quality of the final glass product. The conveying systems must be able to handle materials that are sensitive to moisture and temperature changes, as well as those that may tend to clog or build up in the equipment. HeadPowder's solutions for glass processing include specialized designs with anti-clogging features and temperature-controlled environments to maintain the material's properties. The conveyors are also equipped with high-precision flow control mechanisms to ensure accurate dosing of raw materials, which is crucial for achieving consistent glass quality.
Key Features of Silicate Powder Conveying Systems
HeadPowder's silicate powder conveying systems are characterized by several key features that enhance their performance and reliability. One of the primary features is the use of wear-resistant materials, such as hardened steel or special alloys, to protect the conveyor components from the abrasive nature of silicate powders. This extends the service life of the equipment and reduces maintenance costs. Another important feature is the incorporation of advanced sealing and dust containment systems, which prevent material leakage and protect the working environment from dust exposure. The systems also include automated control and monitoring capabilities, allowing operators to adjust conveying speed, pressure, or other parameters in real time based on production needs. Additionally, the design of the conveyors is optimized for energy efficiency, minimizing power consumption while maintaining high throughput. These features collectively contribute to the overall effectiveness of silicate powder conveyors in industrial applications.
Conclusion
Silicate powder conveyors are essential equipment in industries that rely on the efficient handling of silicate-based materials. The principles behind these systems, combined with their tailored working scene characteristics, make them indispensable for maintaining production efficiency and product quality. HeadPowder, with its expertise in industrial conveying solutions, provides high-quality silicate powder conveyors that are designed to meet the specific demands of various applications, ensuring reliable and effective material transport in manufacturing processes.




