At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and manufacturing of advanced copper oxide powder conveying systems. Our equipment is engineered to handle the unique challenges associated with transporting copper oxide powder, a critical material in various industrial applications. This article delves into the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in modern industrial operations.
Core Principles of Copper Oxide Powder Conveying Systems
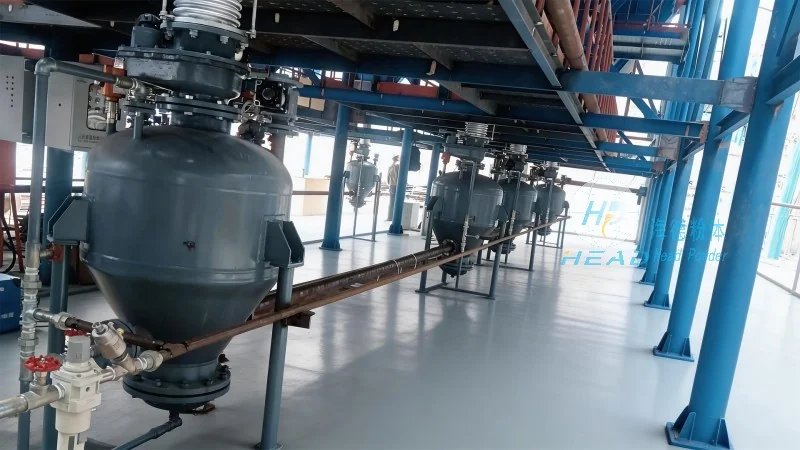
The operation of copper oxide powder conveying systems is based on several core principles that ensure efficient and reliable material transport. Firstly, the system utilizes a combination of mechanical and pneumatic components to move the powder from one location to another. The primary mechanism often involves a screw conveyor or a pneumatic conveying line, which can be tailored to the specific properties of copper oxide powder, such as its density, flowability, and potential for dust generation. Additionally, the system incorporates advanced control technologies to regulate the flow rate, pressure, and temperature, ensuring optimal performance and preventing material degradation or blockages.
Working Scene Characteristics and Applications
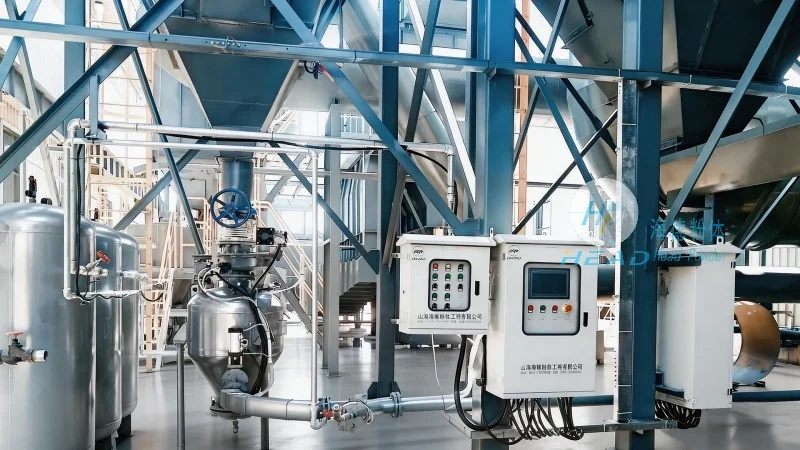
Copper oxide powder conveying systems are widely used in diverse industrial settings, each with distinct characteristics that influence the system's design and functionality. For instance, in the mining and processing industry, these systems are crucial for transporting copper oxide from ore processing facilities to storage or further processing units. The working scene often involves high-volume material handling, requiring robust and durable equipment capable of withstanding heavy usage and potential abrasion from the powder. In the chemical and pharmaceutical sectors, the systems are employed to convey copper oxide in controlled environments, where precision and contamination control are paramount. The working scene may include cleanroom conditions or enclosed systems to maintain product purity. Furthermore, in the manufacturing of electronic components, copper oxide powder is used as a raw material, and the conveying system must ensure consistent quality and minimal particle size variation, which directly impacts the final product's performance.
Key Features and Advantages
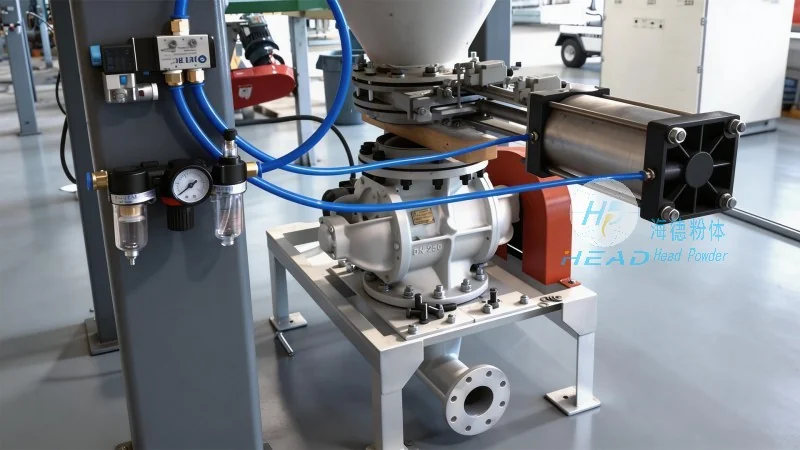
Our copper oxide powder conveying systems are equipped with several key features that enhance their performance and reliability. One of the primary advantages is the ability to handle abrasive materials like copper oxide without significant wear and tear on the equipment components. This is achieved through the use of high-quality materials, such as stainless steel or specialized coatings, which resist corrosion and abrasion. Another critical feature is the integration of dust suppression and filtration systems, which are essential for maintaining a safe and compliant working environment. These systems help in controlling dust emissions, reducing the risk of respiratory issues among workers and complying with environmental regulations. Furthermore, the systems are designed for easy maintenance and cleaning, with accessible components that allow for quick inspection and replacement of parts, minimizing downtime and operational costs.
Customization and Integration Capabilities
At Shandong HeadPowder Engineering Co., Ltd., we understand that each industrial application has unique requirements. Therefore, our copper oxide powder conveying systems are highly customizable to meet specific needs. Clients can choose from various configurations, including different conveyor types, material handling capacities, and control systems. The systems can also be integrated with existing production lines or facilities, ensuring seamless operation and minimal disruption to current workflows. Our engineering team works closely with clients to assess their specific requirements and develop a tailored solution that optimizes performance, efficiency, and cost-effectiveness. This customization approach ensures that the conveying system is perfectly matched to the client's operational needs, whether it's for high-volume production or specialized processing requirements.
Conclusion and Company Overview
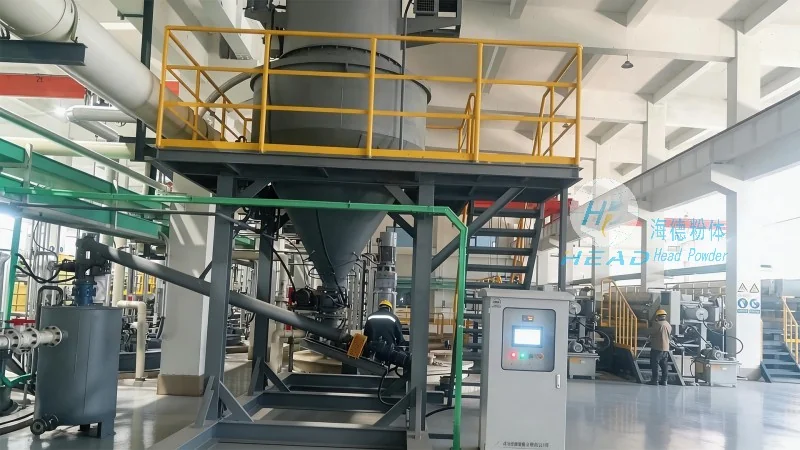
In conclusion, copper oxide powder conveying systems are essential equipment for efficiently and safely transporting copper oxide powder in various industrial applications. The principles behind these systems, combined with their working scene characteristics, make them a reliable choice for industries ranging from mining and chemicals to electronics manufacturing. At Shandong HeadPowder Engineering Co., Ltd., we are committed to providing high-quality, customized solutions that meet the diverse needs of our clients. With our expertise in powder handling technology and commitment to quality, we continue to deliver systems that enhance operational efficiency, ensure product quality, and promote a safe working environment. Our company, based in Shandong, China, is dedicated to advancing the field of powder conveying technology and supporting the growth of industries that rely on copper oxide powder.




