HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and supply of equipment tailored for handling silica fume—a critical component in concrete production. This article delves into the fundamental principles behind silica fume material handling equipment and explores the key characteristics of its operational environments.
Understanding Silica Fume and Its Handling Requirements
Silica fume, also known as microsilica, is a byproduct of silicon metal or ferrosilicon production. It consists of extremely fine particles with a high surface area, making it highly reactive and valuable in enhancing concrete strength and durability. Due to its fine texture and cohesive properties, transporting silica fume requires specialized equipment to ensure efficient and safe handling. The primary challenges in silica fume handling include controlling dust generation, maintaining consistent material flow, and preventing clogging in conveying systems. These factors necessitate the use of advanced material handling technologies designed specifically for this application.
The Core Principles of Silica Fume Material Handling Equipment
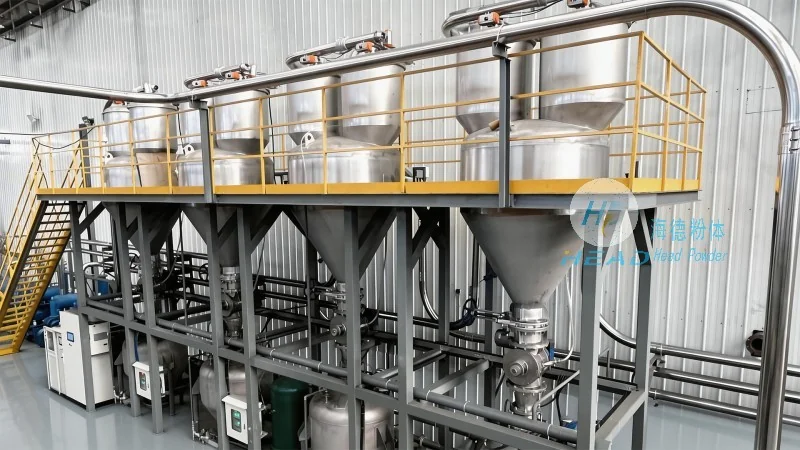
The design of silica fume material handling equipment is guided by several fundamental principles aimed at optimizing performance and reliability. First, the equipment must be capable of handling extremely fine particles without causing excessive wear or degradation. This is achieved through the use of materials with high corrosion resistance and low friction coefficients, such as stainless steel or specialized alloys. Second, the system must minimize dust generation to comply with environmental regulations and ensure workplace safety. This is typically accomplished through enclosed conveying systems, efficient dust collection mechanisms, and sealed transfer points. Third, the equipment needs to maintain a consistent and controlled flow rate to prevent overloading or underloading of downstream processing units. Variable speed drives and adjustable feed mechanisms are commonly employed to achieve this balance. Finally, the design must prioritize ease of maintenance and cleaning to prevent material buildup and ensure long-term operational efficiency.
Key Working Scene Characteristics of Silica Fume Handling Equipment
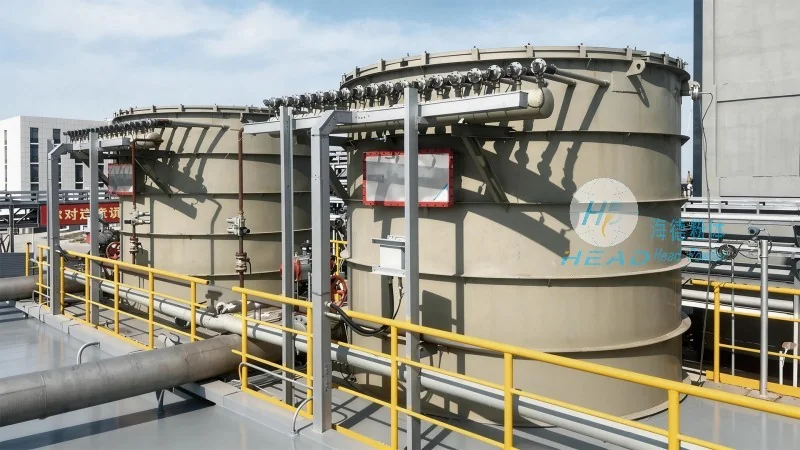
The operational environments where silica fume material handling equipment is deployed exhibit distinct characteristics that influence equipment selection and performance. First, the industrial settings are often characterized by high ambient temperatures and humidity, which can affect the material's properties and equipment performance. The equipment must be designed to withstand these conditions without compromising its structural integrity or material handling capabilities. Second, the working environments may involve high dust concentrations, requiring robust filtration and ventilation systems to maintain air quality and protect personnel. Third, the equipment is typically integrated into large-scale production lines, necessitating seamless coordination with other processing units such as storage silos, mixers, and packaging systems. This integration demands precise control systems and standardized interfaces to ensure smooth material flow. Fourth, the operational scale varies from small-scale batch processing to continuous large-scale production, requiring equipment that can be scaled up or down to meet different production demands. The equipment must therefore be modular and adaptable to accommodate changes in production volume and material flow rates.
HeadPowder's Expertise in Silica Fume Material Handling Solutions
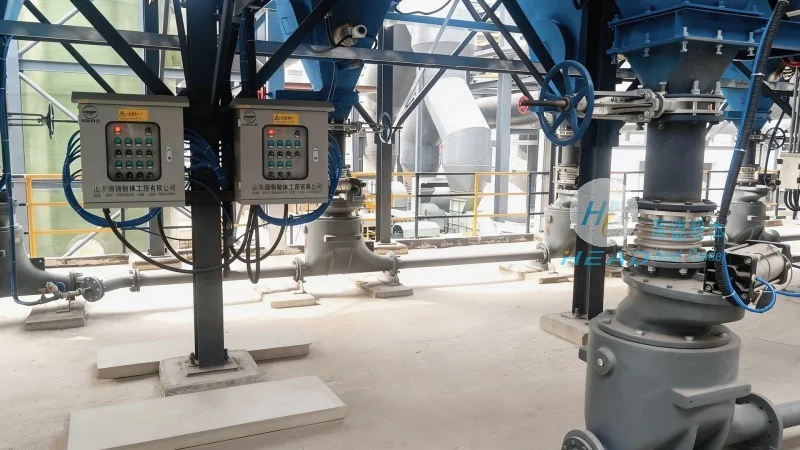
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a prominent manufacturer of silica fume material handling equipment. The company combines advanced engineering expertise with years of industry experience to deliver high-quality, reliable solutions tailored to the specific needs of clients. HeadPowder's product line includes a range of equipment such as pneumatic conveying systems, screw conveyors, and bulk material handling units, all designed to handle silica fume efficiently and safely. The company's commitment to innovation is evident in its use of cutting-edge technologies, including automated control systems, real-time monitoring, and predictive maintenance features. These technologies enhance the operational efficiency and longevity of the equipment, reducing downtime and maintenance costs for clients. HeadPowder also provides comprehensive after-sales support, including installation, training, and technical assistance, ensuring that clients can maximize the performance of their silica fume handling systems. The company's reputation for quality and reliability has made it a trusted partner for businesses in the construction and concrete industries, helping them improve productivity and maintain compliance with environmental standards.




