Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier of material handling equipment. With a focus on industrial applications, the company specializes in designing and producing efficient conveying solutions for various bulk materials, including cement, powders, and granules. HeadPowder is headquartered in Shandong, China, and has established a strong reputation for delivering high-quality, reliable equipment tailored to meet the specific needs of clients in different industries.
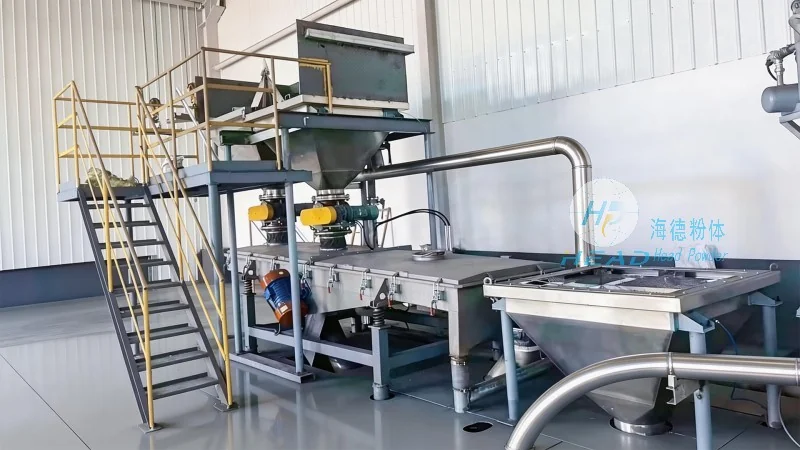
Principles of Cement Gray Material Conveying Equipment
The cement gray material conveying equipment operates based on mechanical principles to transport bulk materials over long distances or vertical heights. The core components typically include a drive system, a conveyor belt or chain, and a hopper or feeding mechanism. The drive system, often powered by electric motors, provides the necessary force to move the material along the conveyor path. The conveyor belt, made from durable materials such as rubber or synthetic fabrics, is designed to handle the weight and abrasiveness of cement and similar powders. The feeding mechanism ensures that the material is evenly distributed onto the conveyor, preventing blockages and ensuring smooth operation. The entire system is engineered to maintain consistent material flow, minimizing downtime and maximizing productivity. The equipment may also incorporate features like variable speed control and overload protection to enhance operational safety and efficiency.
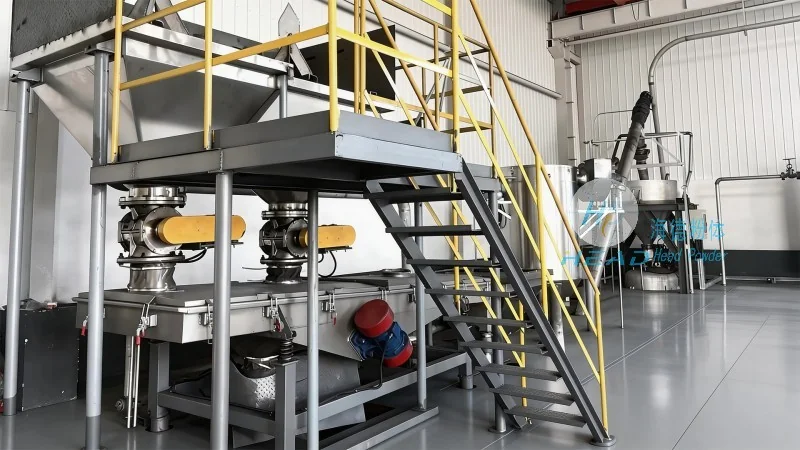
Working Scene Characteristics of Cement Gray Material Conveying Equipment
The working scene characteristics of cement gray material conveying equipment are tailored to the specific demands of industrial environments where bulk materials need to be transported efficiently. These characteristics include high capacity and continuous operation, making them suitable for large-scale production lines in cement plants, construction sites, and manufacturing facilities. The equipment is designed to handle the abrasive nature of cement, ensuring long service life and minimal maintenance. Additionally, the systems are often equipped with dust control measures, such as sealed enclosures and air filtration, to maintain a safe and clean working environment. The flexibility of the equipment allows for integration into existing production workflows, reducing the need for extensive modifications to the facility. The working scene also emphasizes energy efficiency, with modern designs incorporating energy-saving motors and optimized conveyor designs to reduce operational costs. Overall, the characteristics of these conveying systems are centered on reliability, durability, and adaptability to diverse industrial applications.
Typical Working Scenarios and Applications
Cement gray material conveying equipment is widely used in various industrial settings, each with unique requirements that the equipment addresses effectively. In cement production plants, the equipment is crucial for transporting raw materials like limestone and clinker from storage silos to the production line. The high-capacity design ensures that the material is moved quickly and consistently, supporting the continuous operation of the cement manufacturing process. At construction sites, the equipment is used to transport cement and other building materials from storage areas to the work area, improving material handling efficiency and reducing manual labor. In manufacturing facilities, the equipment may be employed to convey powders used in the production of chemicals, pharmaceuticals, or food products. The versatility of the system allows it to handle different material types, including fine powders and granules, making it suitable for a broad range of applications. The working scenarios also highlight the importance of integration with other equipment, such as feeders and classifiers, to create a seamless material handling process. This integration ensures that the material is processed efficiently from intake to final use, minimizing waste and maximizing productivity.
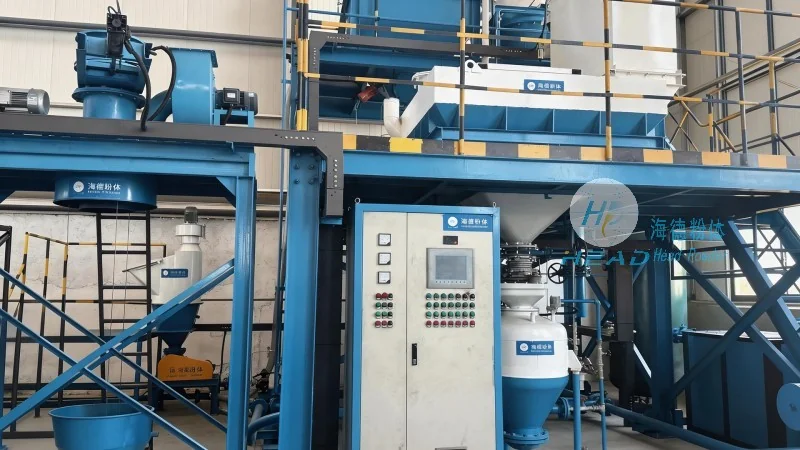
Key Advantages and Benefits
HeadPowder's cement gray material conveying equipment offers several key advantages that make it a preferred choice for industrial applications. The equipment is designed for durability, with components made from high-quality materials that can withstand the harsh conditions of cement and other bulk materials. This results in a longer service life and lower maintenance costs over time. The systems are also highly efficient, with optimized conveyor designs that minimize energy consumption while maintaining high material throughput. Additionally, the equipment is easy to install and integrate into existing production lines, reducing downtime during setup. The safety features, such as overload protection and sealed enclosures, ensure that the operation is safe for personnel and compliant with industrial safety standards. The adaptability of the equipment allows it to be customized to meet specific client requirements, including different conveyor lengths, heights, and material types. Overall, the advantages of these conveying systems contribute to improved operational performance, reduced costs, and enhanced safety in industrial environments.




