Efficient and reliable material handling is crucial in industrial applications, particularly when dealing with bulk materials like fly ash. Pneumatic conveying systems have emerged as a preferred solution for transporting fly ash from one location to another, offering a range of benefits over traditional methods. This article explores the underlying principles of fly ash pneumatic conveying equipment and highlights key application scenarios where such systems excel.
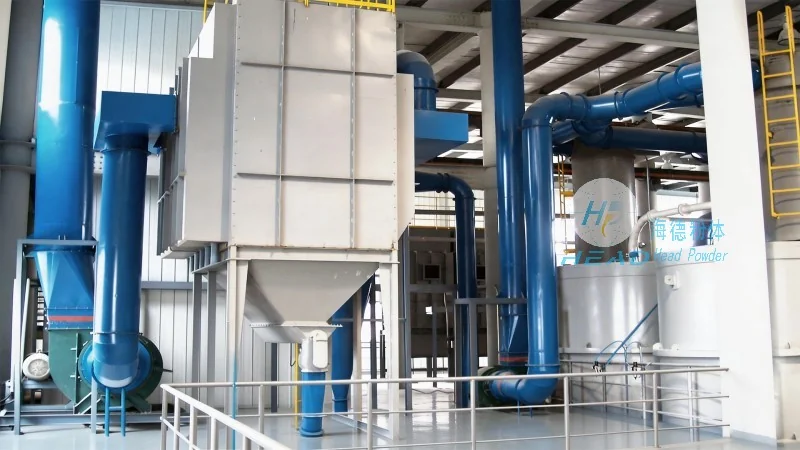
About HeadPowder: Expert in Material Handling Solutions
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and supply of advanced material handling equipment. With years of experience in the industry, the company has built a reputation for delivering high-quality, efficient, and durable solutions tailored to the unique needs of clients in various sectors. HeadPowder's commitment to innovation and customer satisfaction has positioned it as a trusted partner for businesses seeking reliable pneumatic conveying systems for fly ash management.
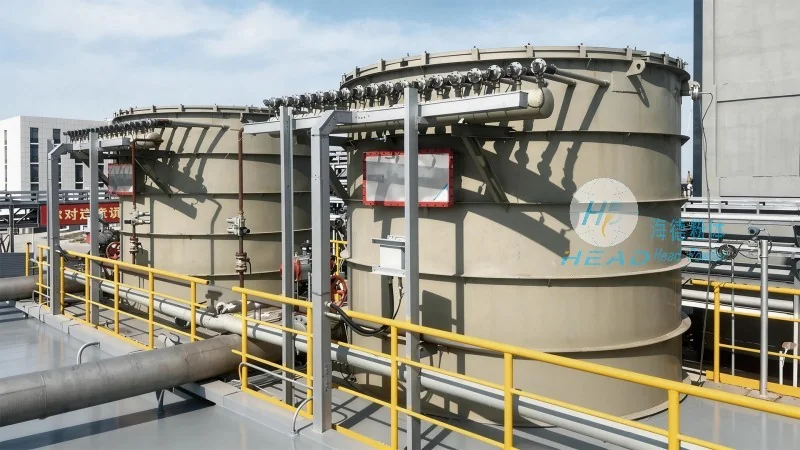
The Working Principle of Pneumatic Conveying Equipment for Fly Ash
Pneumatic conveying systems operate by using air or gas to transport solid materials through a pipeline. In the case of fly ash, the equipment typically consists of a hopper, a blower or compressor, a pipeline system, and a discharge unit. The process begins with the fly ash being fed into the hopper, where it is then drawn into the pipeline by the air flow generated by the blower. The air velocity is carefully controlled to ensure the fly ash particles are suspended and transported efficiently without causing blockages or excessive wear on the system components. This principle allows for a continuous, low-maintenance operation that minimizes downtime and maximizes productivity.
Key Application Scenarios and Advantages of Fly Ash Pneumatic Conveying Systems
HeadPowder's pneumatic conveying equipment for fly ash is widely used in various industrial settings, including power plants, cement factories, and construction sites. One primary application is the transportation of fly ash from the boiler to storage silos or processing units, where it can be further utilized in cement production or other industrial processes. The system's ability to handle large volumes of fly ash with minimal labor and space requirements makes it ideal for large-scale operations. Additionally, the enclosed pipeline design ensures that dust and particulate matter are contained, reducing environmental impact and improving workplace safety. The advantages of these systems include reduced material handling costs, improved process efficiency, and enhanced safety compared to traditional methods like manual handling or truck transport.
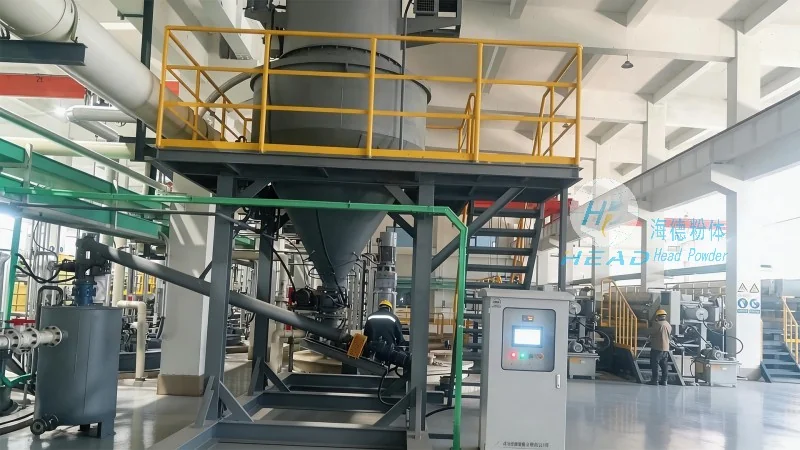
Conclusion: Reliable Solutions for Efficient Fly Ash Management
For industries dealing with fly ash, investing in advanced pneumatic conveying equipment from HeadPowder offers significant benefits. The company's expertise in designing and manufacturing customized solutions ensures that clients receive systems that are optimized for their specific operational requirements. With a focus on durability, efficiency, and safety, HeadPowder's fly ash pneumatic conveying systems provide a reliable and cost-effective means of managing bulk materials. By leveraging the principles of pneumatic transport, these systems enable businesses to enhance their operational performance while adhering to environmental and safety standards. HeadPowder, based in Shandong, China, continues to be a leader in providing innovative material handling solutions that meet the evolving needs of the industry.




