HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of advanced air-driven conveyor systems tailored for the efficient handling of anhydrous sodium sulfate (Na₂SO₄), a key industrial chemical used in various applications such as glass manufacturing, paper production, and chemical synthesis. This equipment is engineered to meet the unique demands of material transport in industrial settings, ensuring reliable performance and optimal operational efficiency. The company, based in Shandong, China, has established itself as a leading provider of bulk material handling solutions, with a focus on pneumatic conveying technology for challenging materials like anhydrous sodium sulfate.
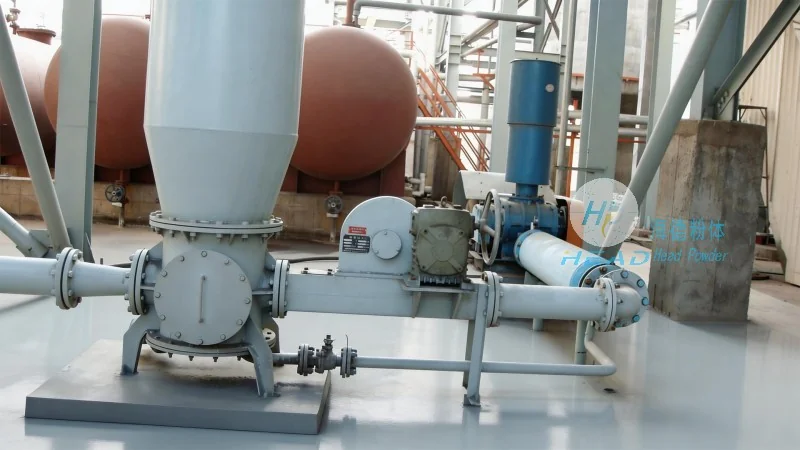
Principle of Air-Driven Material Transport
The core principle of air-driven conveyor equipment involves the use of a pressurized air stream to move bulk materials through a pipeline system. For anhydrous sodium sulfate, the system typically employs either positive pressure (pressure pneumatic conveying) or negative pressure (suction pneumatic conveying), depending on the specific application requirements. In positive pressure systems, compressed air is introduced at the material inlet, creating a high-pressure environment that propels the particles forward. This method is ideal for long-distance transport and handling of dry, free-flowing materials like anhydrous sodium sulfate. In contrast, negative pressure systems use a vacuum at the outlet to draw the material into the pipeline, which is suitable for applications requiring gentle handling or when the material is to be collected from multiple points. The air stream suspends the anhydrous sodium sulfate particles, allowing them to be transported efficiently with minimal friction and energy consumption. This pneumatic conveying technology eliminates the need for mechanical components like belts, buckets, or screw conveyors, reducing maintenance costs and enhancing safety in the workplace by minimizing direct contact with the material.
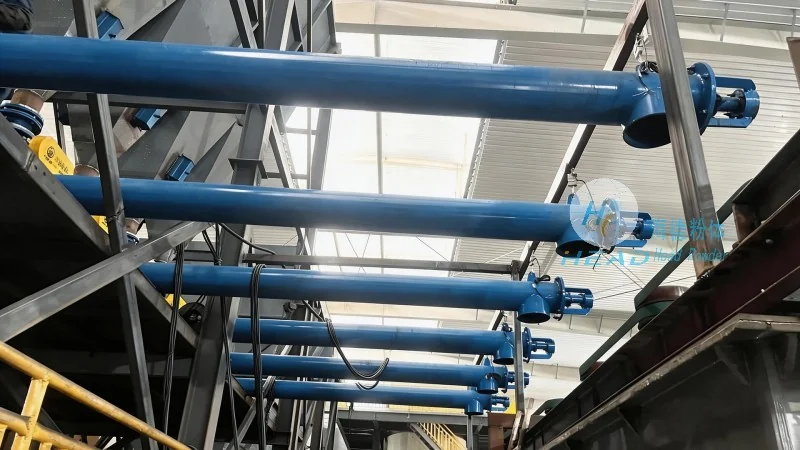
Key Working Scene Characteristics
The air-driven conveyor equipment for anhydrous sodium sulfate is designed to operate effectively in diverse industrial environments, including chemical plants, glass factories, and mining operations. Its adaptability to different working conditions is a significant advantage, as it can handle varying particle sizes (typically ranging from 0.1 mm to several millimeters), moisture content, and flow rates of the material. The system's ability to maintain consistent material flow and prevent clogging is crucial in applications where continuous production is essential, such as in the production of glass where anhydrous sodium sulfate is used as a flux. Additionally, the equipment's compact design and modular construction enable easy integration into existing production lines, minimizing downtime during installation and maintenance. The system can be configured with multiple inlets and outlets, allowing for flexible material distribution and collection, which is particularly beneficial in large-scale industrial operations. The air-driven conveyor also offers advantages in terms of space efficiency, as it can transport materials vertically or horizontally, or even in a combination of both, without the need for complex infrastructure.
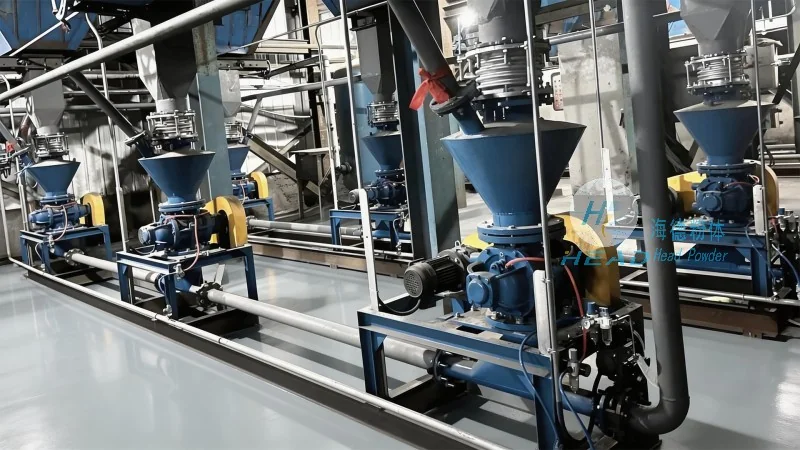
Company Profile and Technical Expertise
HeadPowder Engineering Co., Ltd., a prominent manufacturer based in Shandong, China, has built a strong reputation in the bulk material handling industry. The company specializes in the development and production of air-driven conveyor systems, with a focus on providing customized solutions for challenging materials like anhydrous sodium sulfate. With years of experience in engineering and manufacturing, HeadPowder has developed a comprehensive range of products that meet the specific needs of various industries. The company's technical team consists of experienced engineers and technicians who provide expert consultation and support to help clients select the most suitable equipment for their operational requirements. They conduct thorough site assessments and material analysis to ensure that the chosen system is optimized for performance, energy efficiency, and longevity. HeadPowder's commitment to quality is evident in their adherence to international standards and rigorous testing procedures, ensuring that their products deliver reliable and consistent performance over the long term. The company also offers after-sales support, including maintenance services and spare parts availability, to minimize downtime and maximize operational uptime for their clients.




