Denitrizer powder conveying system equipment, as a critical component in industrial processes, plays a vital role in the efficient transportation of denitrizer powders. This equipment is designed to handle the challenges associated with powder handling, ensuring stable and reliable operation in various industrial applications. The system integrates advanced technologies to address issues such as dust generation, material blockage, and energy consumption, making it an essential solution for modern industrial facilities.
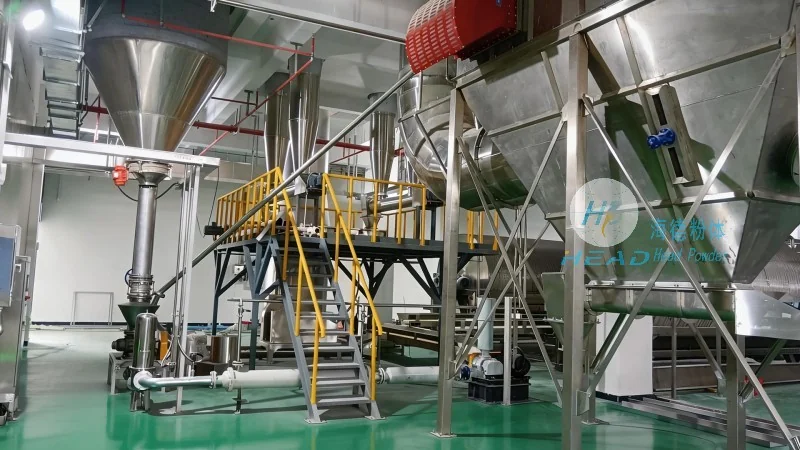
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling equipment, specializes in providing high-quality solutions for industrial powder conveying systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for businesses seeking reliable and efficient powder handling solutions. HeadPowder's products are engineered to meet the diverse needs of different industries, including power generation, chemical processing, and environmental protection. The company's headquarters is located in Shandong, China, where it leverages local resources and expertise to develop cutting-edge technologies.
Key Components and Structure of the Conveying System
The denitrizer powder conveying system typically consists of several key components that work in harmony to ensure smooth operation. These components include a hopper for material storage, a feeder to control the flow rate, a conveyor system (such as a screw conveyor or pneumatic conveyor) for material transport, and a control panel for system monitoring and operation. The hopper is designed to hold a sufficient quantity of denitrizer powder, ensuring a continuous supply to the system. The feeder regulates the material flow, preventing overloading or underloading of the conveyor. The conveyor system, whether mechanical or pneumatic, efficiently transports the powder from the hopper to the desired destination, such as a reactor or storage tank. The control panel allows operators to monitor the system's performance, adjust parameters, and receive alerts in case of any abnormalities.
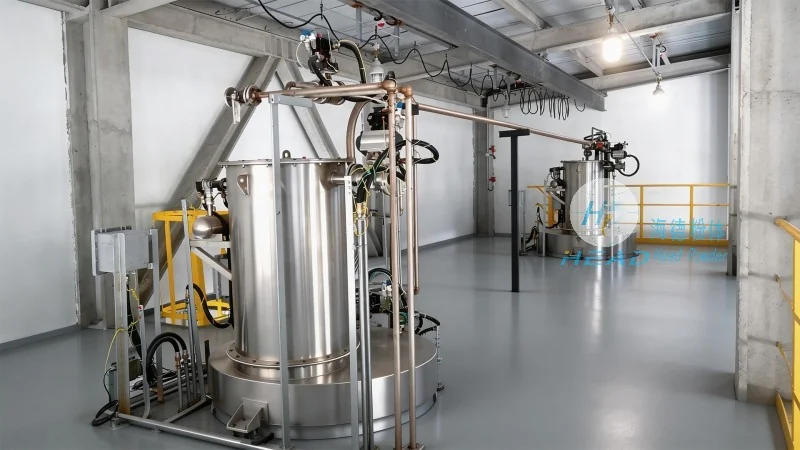
Operating Process of the Conveying System
The operation of the denitrizer powder conveying system follows a systematic process to ensure efficient and safe material handling. The process begins with the loading of denitrizer powder into the hopper. The feeder then starts to discharge the powder at a controlled rate, which is regulated based on the system's requirements and the material's characteristics. The conveyor system receives the powder from the feeder and transports it to the next stage of the process. During this phase, the system continuously monitors the flow rate and pressure to maintain stable operation. If any issues arise, such as blockage or excessive pressure, the control panel triggers appropriate responses, such as adjusting the feeder speed or activating a cleaning mechanism. The system's design ensures that the powder is conveyed without excessive vibration or spillage, minimizing the risk of dust generation and environmental contamination.
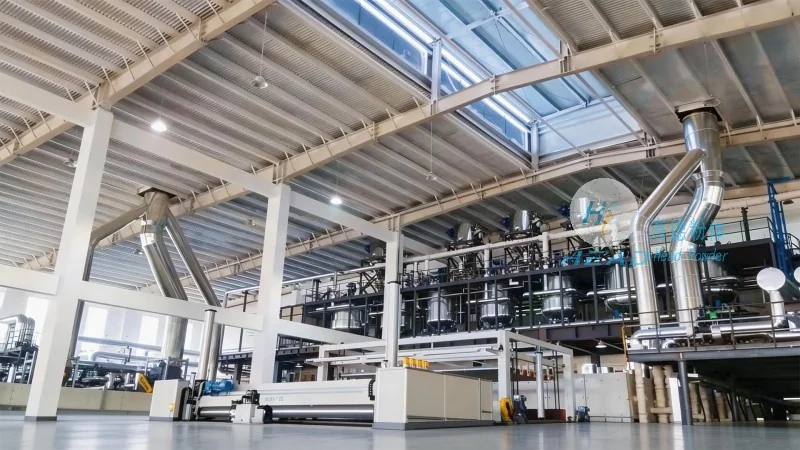
Working Principle of the Conveying System
The working principle of the denitrizer powder conveying system is based on the principles of fluidization and mechanical transport. In pneumatic conveying systems, the powder is suspended in a stream of air, which allows it to be transported through pipes. The air flow is controlled to maintain the powder in a fluidized state, preventing it from settling or clogging the system. Mechanical conveying systems, such as screw conveyors, use rotating screws to push the powder forward, ensuring consistent and reliable transport. The system's design takes into account the properties of the denitrizer powder, including its particle size, density, and flowability, to optimize the conveying process. By understanding the material's characteristics, the system can be configured to achieve the desired flow rate and pressure, minimizing energy consumption and maximizing efficiency.
Advantages and Applications of the Conveying System
The denitrizer powder conveying system offers several advantages that make it an ideal choice for industrial applications. These advantages include high efficiency, low maintenance requirements, and the ability to handle a wide range of powder types. The system is designed to minimize dust generation, which is crucial for maintaining a safe and clean working environment. Additionally, the system's modular design allows for easy integration into existing industrial processes, reducing downtime and installation costs. The denitrizer powder conveying system is widely used in power plants, chemical factories, and environmental protection facilities, where it plays a critical role in the handling of denitrizer powders. By ensuring the efficient and safe transport of these materials, the system contributes to the overall productivity and sustainability of industrial operations.




