HeadPowder, a leading provider in the field, specializes in the design and implementation of fully automatic powder pneumatic conveying systems. These systems are engineered to efficiently transport bulk powders through a network of pipes using air as the primary medium. The technology offers a reliable and flexible solution for industries dealing with various types of powders, ensuring consistent performance and minimal downtime.
Key Components and Their Roles
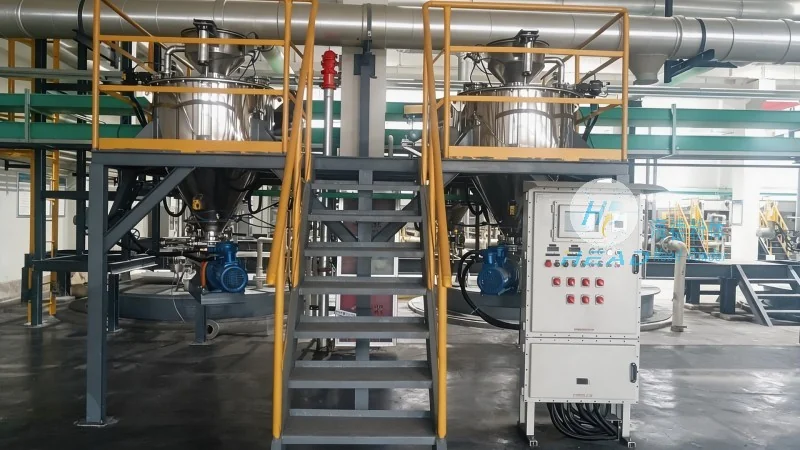
The fully automatic powder pneumatic conveying system comprises several critical components that work in tandem to achieve seamless operation. At the core is the feeding unit, which introduces the powder into the system. This is followed by the air compressor, which generates the necessary air pressure to move the material. The pipeline network connects different sections of the system, while the control system manages the entire process, ensuring optimal air flow and powder transport. Each component is designed for durability and efficiency, contributing to the overall reliability of the system.
Operation Process: Step-by-Step Overview
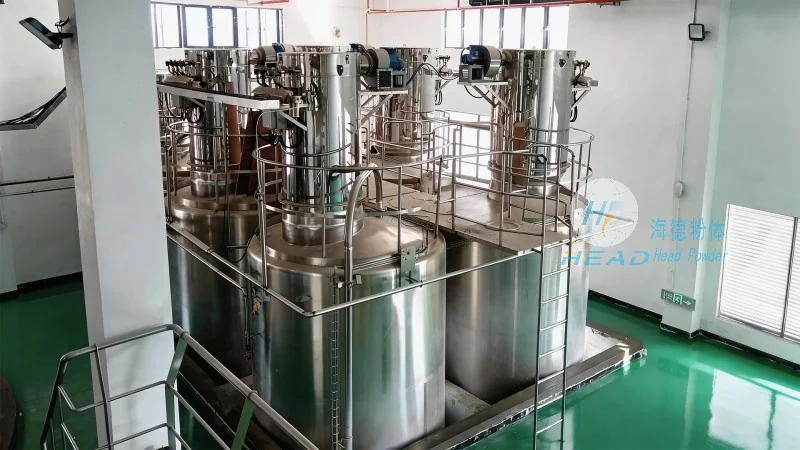
The operation of a fully automatic powder pneumatic conveying system follows a systematic sequence. Initially, the powder is fed into the hopper or feeder. The control system then activates the air compressor, which starts delivering compressed air into the pipeline. As the air flows, it creates a pressure differential that propels the powder particles through the system. The powder travels through the pipeline, reaching the discharge point where it is collected. The system continuously monitors the air pressure and flow rate, adjusting parameters as needed to maintain consistent performance. This automated process eliminates the need for manual intervention, reducing labor costs and enhancing operational efficiency.
Working Principle: How It Transports Powders
The working principle of the fully automatic powder pneumatic conveying system is based on the principle of pneumatic transport. When air is compressed and introduced into the pipeline, it creates a flow that carries the powder particles. The system utilizes either positive pressure or negative pressure (or a combination of both) to move the material. Positive pressure systems force air and powder through the pipeline, while negative pressure systems create a vacuum that draws the powder. The choice of system depends on the specific characteristics of the powder and the application requirements. The fully automatic design ensures that the system can handle different powder types, from fine powders to bulk materials, with precision and reliability.
Advantages and Applications
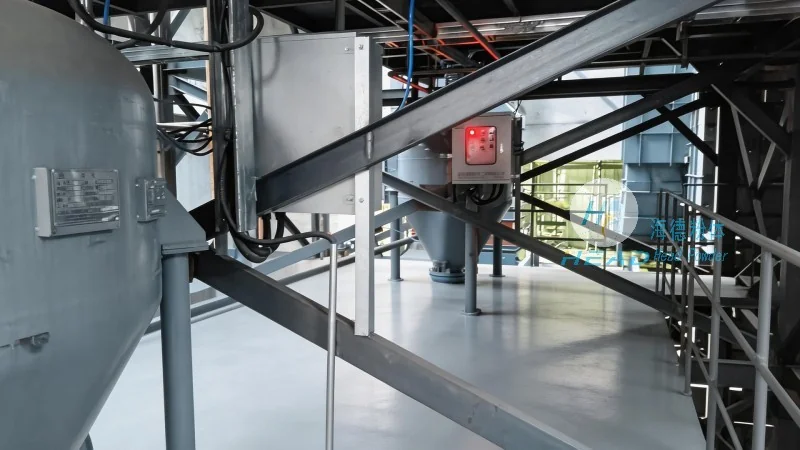
Fully automatic powder pneumatic conveying systems offer numerous advantages over traditional methods. They provide a dust-free and hygienic environment, which is crucial for industries such as pharmaceuticals, food processing, and chemical manufacturing. The system also reduces material waste and improves product quality by minimizing exposure to contaminants. Additionally, the automated control system enhances safety by preventing over-pressurization and ensuring consistent operation. These systems are widely used in various industries, including cement, pharmaceuticals, food, and chemicals, for applications like material transfer, blending, and packaging. The flexibility of the system allows it to be customized to meet the specific needs of different processes, making it a versatile solution for bulk powder handling.




