HeadPowder, a leading provider in the field of pneumatic conveying technology, specializes in the design, manufacturing, and installation of dilute phase material conveying systems. These systems are essential for efficiently transporting bulk materials over long distances with minimal maintenance and operational costs. The following content provides a detailed overview of the operation process and working principles of such systems, highlighting the key components and their functions.
Overview of Dilute Phase Pneumatic Conveying Systems
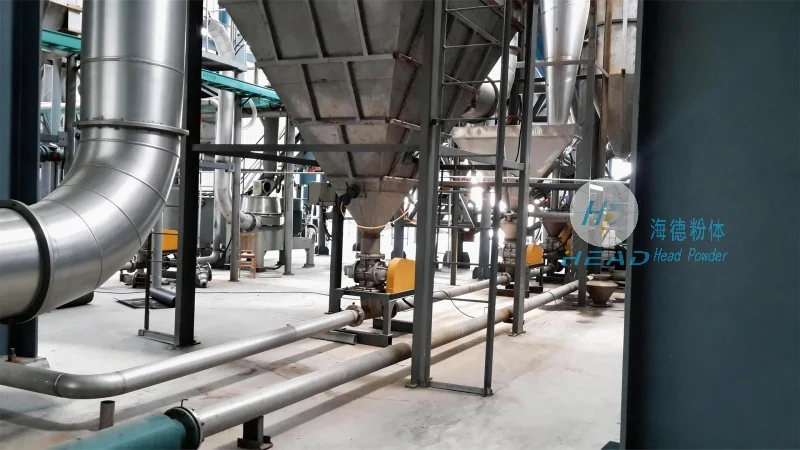
Dilute phase pneumatic conveying systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and minerals. These systems operate by transporting material particles suspended in a high-velocity air stream. The key advantage of dilute phase systems is their ability to handle a wide range of materials, from fine powders to granules, with minimal degradation or segregation. The system typically consists of a blower, a conveying line, a material feed hopper, and a discharge receiver. The blower generates the necessary air pressure and velocity to move the material through the pipeline.
Key Components and Their Functions
The dilute phase pneumatic conveying line comprises several critical components, each playing a vital role in the overall operation. The blower, often an industrial centrifugal or positive displacement type, provides the motive force by creating a pressure differential. The conveying line, usually made of stainless steel or other corrosion-resistant materials, ensures the material is transported efficiently and hygienically, depending on the application. The material feed hopper is designed to feed the material into the system at a controlled rate, preventing blockages and ensuring consistent flow. The discharge receiver collects the material at the end of the line, allowing for easy unloading and further processing.
Operation Process of the Dilute Phase System
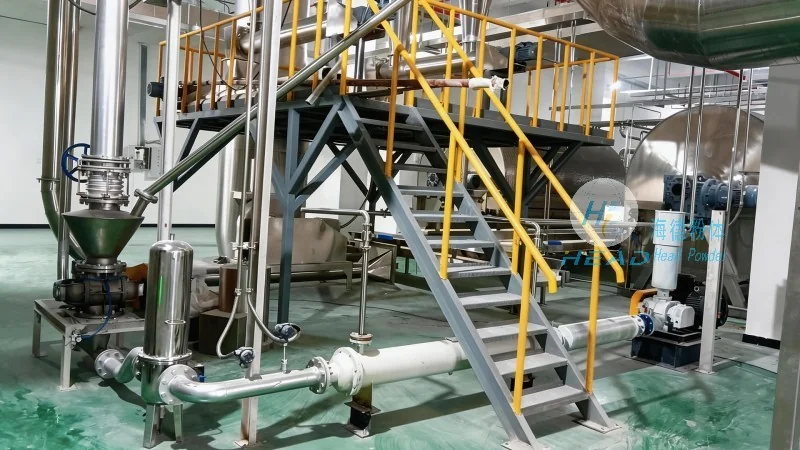
The operation of a dilute phase material conveying line begins with the material being fed into the hopper. The material is then drawn into the blower's inlet by the suction created as the air is expelled from the discharge end. The blower increases the air velocity to a level sufficient to suspend the material particles in the air stream. As the material is carried through the conveying line, it travels to the discharge receiver. The air and material mixture then enters the receiver, where the air is separated from the material, often through a cyclone or filter system. The separated air is then discharged to the atmosphere or recirculated, while the material is collected for further use.
Working Principles of the System
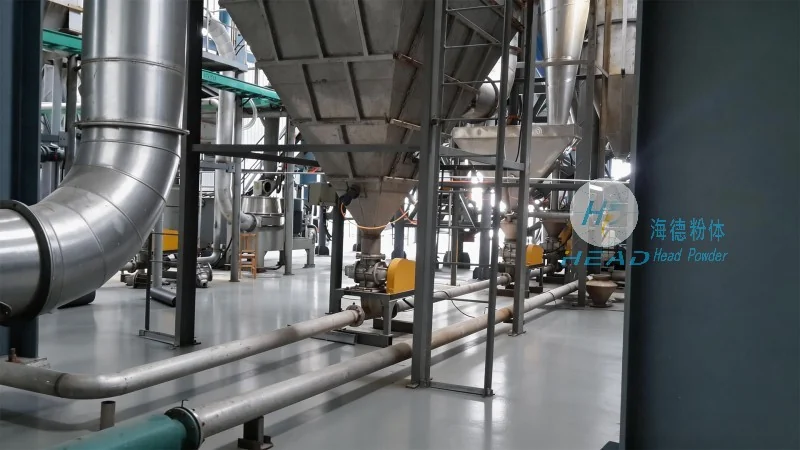
The working principle of a dilute phase pneumatic conveying system is based on the principle of fluidization and suspension. The air stream generated by the blower creates a pressure drop along the conveying line, which pulls the material from the hopper. The material particles are kept in suspension by the high velocity of the air, preventing them from settling or sticking to the pipe walls. The system's efficiency depends on maintaining the correct air velocity and pressure, which ensures that the material remains suspended throughout the entire conveying process. Proper design and maintenance of the components are crucial to achieve optimal performance and minimize downtime.
Benefits and Applications
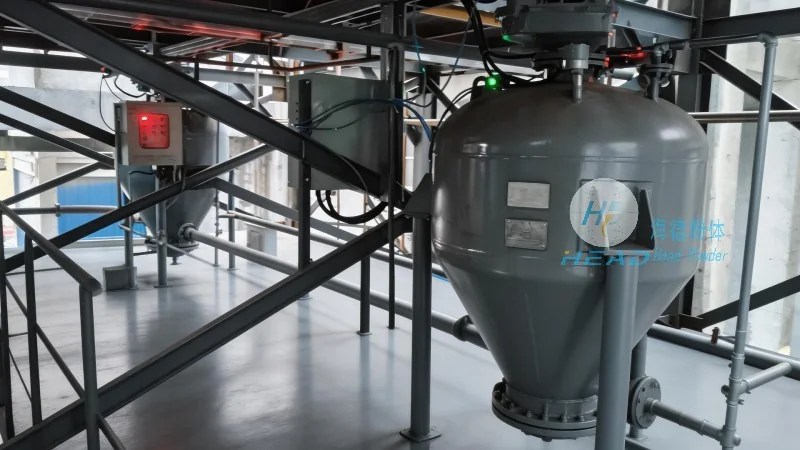
Dilute phase pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. These include reduced material degradation, lower maintenance costs, and the ability to transport materials in a closed system, which is essential for handling hazardous or sensitive materials. The systems are particularly suitable for applications requiring long-distance transport, such as in the chemical and mining industries. Additionally, the systems can be easily integrated with other processing equipment, such as mixers, dryers, and storage silos, to form a complete material handling solution.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a reputable company specializing in the engineering and manufacturing of pneumatic conveying systems. With a strong focus on innovation and quality, HeadPowder provides customized solutions tailored to the specific needs of its clients. The company's headquarters is located in Shandong, China, where it has a team of experienced engineers and technicians dedicated to delivering reliable and efficient material handling solutions. HeadPowder's commitment to customer satisfaction and technological advancement has made it a trusted partner in the industry, serving clients worldwide with high-performance dilute phase pneumatic conveying systems.




