HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and integration of advanced pneumatic conveying systems. Based in Shandong, China, the company has established itself as a trusted partner for industries requiring efficient and reliable powder material transport solutions. This article provides an overview of the automatic bulk bag unloading pneumatic conveying system, detailing its structural components and operational principles.
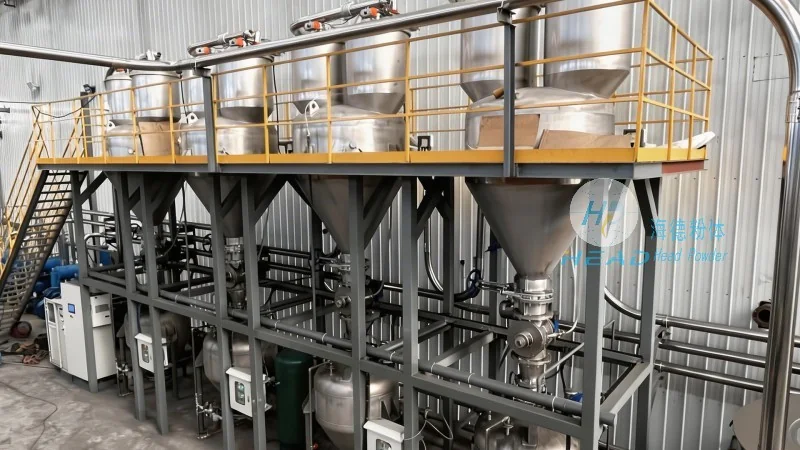
Company Profile and Expertise
HeadPowder Engineering Co., Ltd. is a professional manufacturer dedicated to providing high-quality powder handling equipment. With years of experience in the industry, the company has developed a comprehensive range of solutions tailored to meet the diverse needs of clients across various sectors. The company's commitment to innovation and quality ensures that its products are not only efficient but also durable and user-friendly. HeadPowder's systems are designed to enhance operational efficiency, reduce labor costs, and improve overall productivity in powder handling processes.
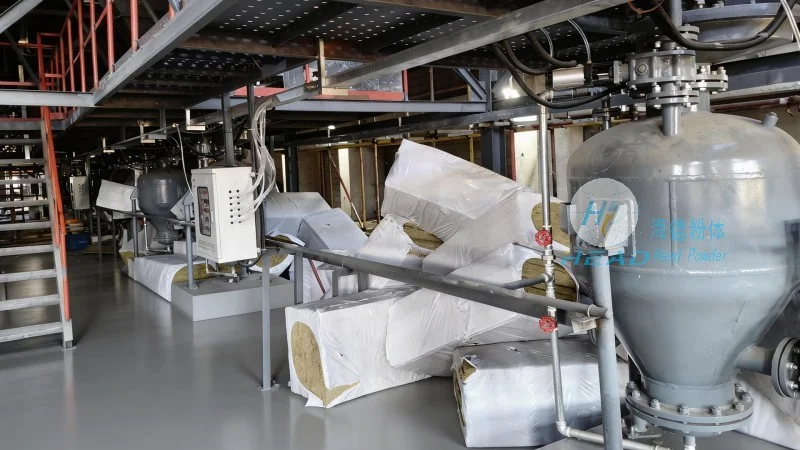
Overview of the Automatic Bulk Bag Unloading Pneumatic Conveying System
The automatic bulk bag unloading pneumatic conveying system is a sophisticated piece of equipment engineered to streamline the process of transferring bulk powders from sealed bags into processing or storage facilities. This system integrates multiple components that work in tandem to achieve seamless and continuous material handling. The core functionality involves the automated opening of bulk bags, the extraction of powder through a pneumatic conveying mechanism, and the delivery of the material to the desired destination. The system is designed to handle a wide variety of powders, including fine, dry, and abrasive materials, making it suitable for applications in pharmaceuticals, food processing, chemical manufacturing, and other industries where precision and reliability are paramount.
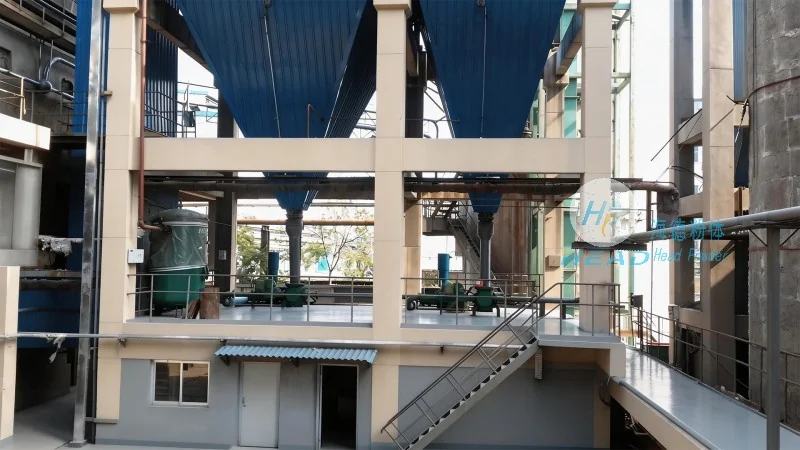
Structural Components and Operational Principles
The automatic bulk bag unloading pneumatic conveying system comprises several key components, each playing a critical role in the overall operation. The primary components include the bulk bag unloader, the pneumatic conveying line, the dust collection system, and the material discharge unit. The bulk bag unloader is responsible for the initial opening and emptying of the bulk bag, typically using a combination of mechanical and pneumatic forces to ensure complete discharge. The pneumatic conveying line, often equipped with a positive displacement blower or a rotary lobe pump, generates the necessary air pressure to transport the powder through the system. The dust collection system, integrated into the design, captures any airborne particles, ensuring compliance with environmental regulations and maintaining a clean working environment. The material discharge unit, such as a hopper or a silo, receives the conveyed powder and stores it for further processing.
Key Features and Advantages
HeadPowder's automatic bulk bag unloading pneumatic conveying system offers several advantages that set it apart from traditional manual or semi-automated methods. One of the most significant benefits is the reduction in labor requirements, as the system operates with minimal human intervention. This not only lowers operational costs but also minimizes the risk of human error and exposure to hazardous materials. The system's high efficiency ensures that bulk bags are emptied completely, reducing material waste and maximizing the utilization of raw materials. Additionally, the pneumatic conveying mechanism allows for the transport of powders over long distances without the need for complex infrastructure, such as conveyor belts or elevators. The integration of a dust collection system enhances safety and environmental compliance, making the system suitable for applications in industries where air quality is a critical concern. The system's modular design enables easy installation and maintenance, with components that can be replaced or upgraded as needed to adapt to changing operational requirements.
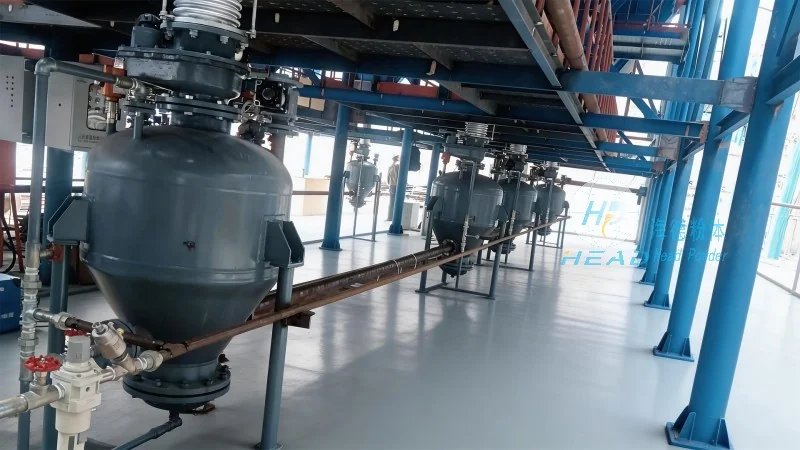
Application Scenarios
The automatic bulk bag unloading pneumatic conveying system is widely used in various industrial applications where bulk powders need to be handled efficiently. In the pharmaceutical industry, for example, the system is employed to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination. The food processing sector utilizes the system to handle dry ingredients like flour, sugar, and spices, ensuring that the materials are transferred hygienically and without cross-contamination. In chemical manufacturing, the system is used to transport abrasive and corrosive powders, such as pigments and chemicals, while maintaining the integrity of the material and the equipment. The system's versatility also makes it suitable for use in the agricultural sector, where it can be used to handle fertilizers and other agricultural chemicals. Overall, the system's ability to handle a wide range of materials and its adaptability to different operational conditions make it a valuable asset for any industry requiring reliable powder handling solutions.




