Barley powder conveying systems are essential in industrial processes where the efficient handling of barley-derived powders is critical. These systems are designed to transport barley powder from storage or processing units to various destinations within a facility, ensuring smooth and reliable material flow. The technology behind these systems combines mechanical components and engineering principles to achieve optimal performance in terms of speed, capacity, and safety.
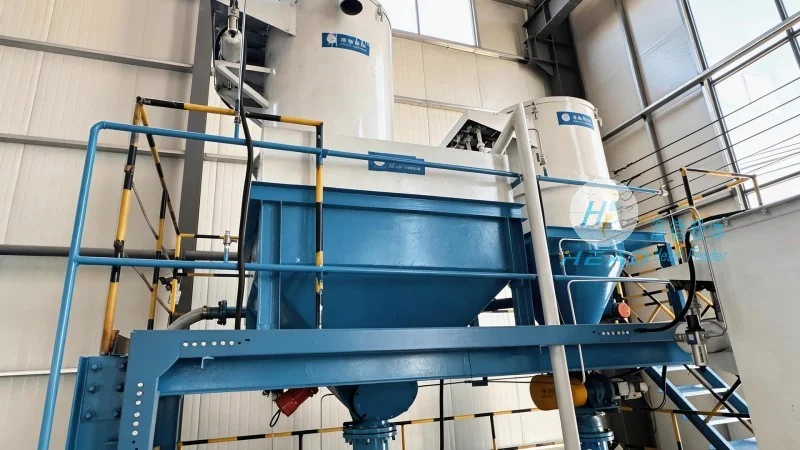
HeadPowder, a leading provider in the field, specializes in the design, manufacturing, and implementation of advanced barley powder conveying solutions. With a focus on precision and durability, their systems are tailored to meet the specific needs of clients in the food, pharmaceutical, and agricultural sectors. The company’s expertise lies in integrating state-of-the-art components that enhance the overall efficiency of powder handling operations.
At the core of any barley powder conveying system is the structural framework that supports the entire operation. This framework typically includes a series of components such as hoppers, conveyors, and control mechanisms. The hoppers are responsible for collecting and storing the barley powder, ensuring a consistent feed to the conveyor system. The conveyors, which may be of various types like screw, pneumatic, or belt conveyors, transport the powder through the system. Control mechanisms, including sensors and automation systems, regulate the flow and ensure that the process operates within safe and efficient parameters.
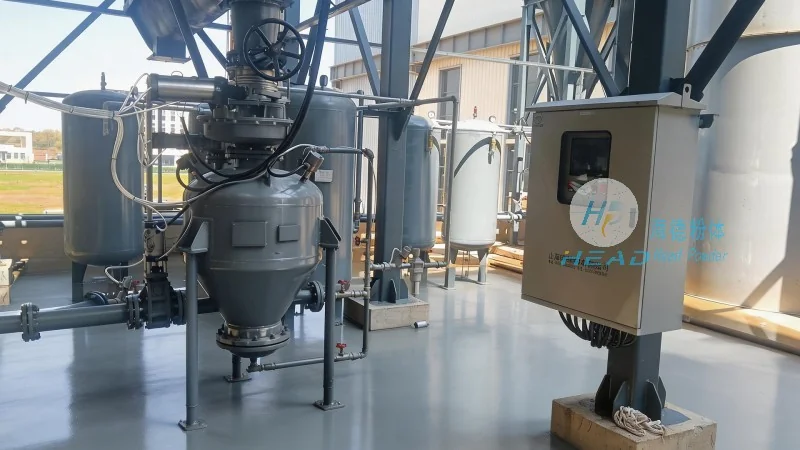
The working principles of barley powder conveying systems revolve around the mechanics of material movement. For instance, screw conveyors utilize rotating screws to push the powder forward, while pneumatic systems employ air pressure to move the material through pipes. Each method has its advantages and is chosen based on factors like the powder’s properties, the required conveying distance, and the environmental conditions. HeadPowder’s engineers carefully select the most suitable technology for each application, ensuring that the system is both effective and cost-efficient.
Material handling in barley powder applications demands high standards of cleanliness and hygiene, especially in industries like food processing. Therefore, the design of these conveying systems incorporates features that prevent contamination and maintain product integrity. Stainless steel components, sealed connections, and easy-to-clean surfaces are common elements in modern systems. These features not only meet regulatory requirements but also extend the lifespan of the equipment and reduce maintenance costs.
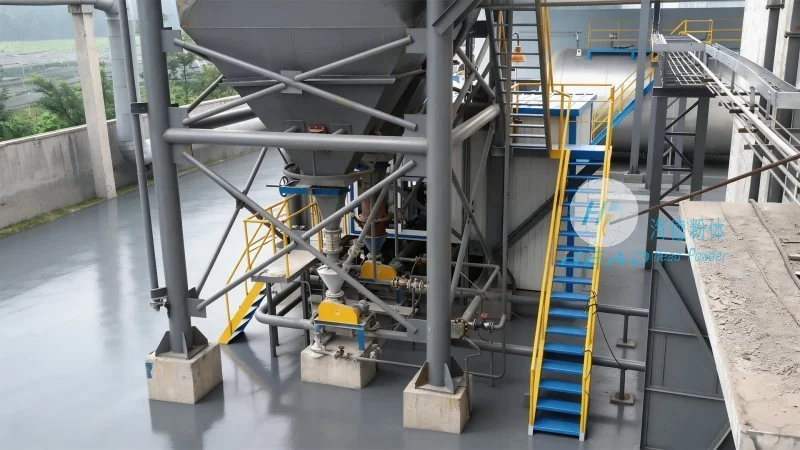
Another critical aspect of barley powder conveying is the integration of safety measures. The systems are equipped with safety sensors and emergency stop buttons to prevent accidents during operation. Additionally, the design considers the potential for dust accumulation, which can be a fire hazard in powder handling environments. Proper ventilation and explosion-proof components are incorporated to mitigate these risks, ensuring a safe working environment for operators.
HeadPowder’s commitment to quality and innovation is evident in their approach to system design. The company employs rigorous testing and validation processes to ensure that each conveying system meets the highest industry standards. Their team of engineers collaborates closely with clients to understand their unique requirements, from initial consultation to final installation and maintenance. This customer-centric approach has made HeadPowder a trusted partner for businesses seeking reliable and efficient barley powder conveying solutions.
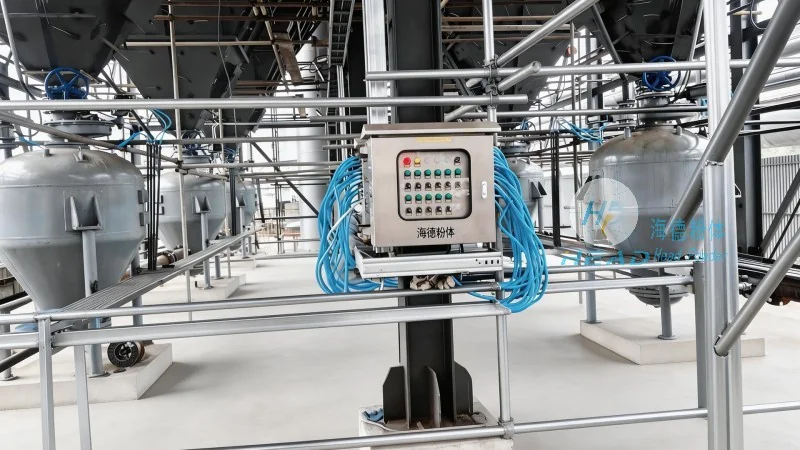
As the demand for barley-based products continues to grow, the importance of efficient powder handling systems becomes increasingly significant. The technology developed by HeadPowder not only enhances productivity but also contributes to the sustainability of operations by reducing waste and improving resource utilization. By leveraging advanced engineering and a deep understanding of powder dynamics, HeadPowder’s systems help clients achieve their operational goals while maintaining compliance with industry regulations.
In conclusion, barley powder conveying systems, as exemplified by those offered by Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated blend of engineering and practical application. These systems are designed to handle the unique challenges of barley powder, ensuring reliable and efficient material transport. With a focus on quality, safety, and customer satisfaction, HeadPowder continues to set the benchmark in the industry, providing solutions that meet the evolving needs of modern industrial processes.




