Positive pressure dilute phase powder transport equipment is a specialized system designed for the efficient and reliable transportation of bulk powders over long distances. This technology is widely used in various industrial sectors, including chemical, food, pharmaceutical, and mining industries, where the safe and efficient movement of powders is critical to operational efficiency and product quality.
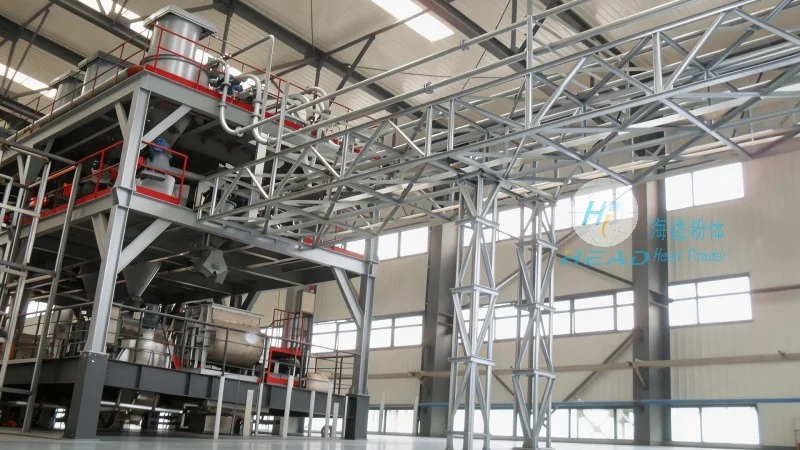
Key Features and Advantages of the Equipment
The core of positive pressure dilute phase powder transport systems lies in their ability to transport powders in a dilute phase, typically at high velocities, ensuring minimal particle agglomeration and maintaining the integrity of the material. This method offers several advantages over traditional dense phase or pneumatic conveying systems. For instance, it provides higher throughput rates, lower energy consumption per unit of material, and reduced equipment wear due to the lower pressure differentials required. Additionally, the dilute phase operation allows for better control over particle flow, which is essential for preventing blockages and ensuring consistent material delivery to the destination.
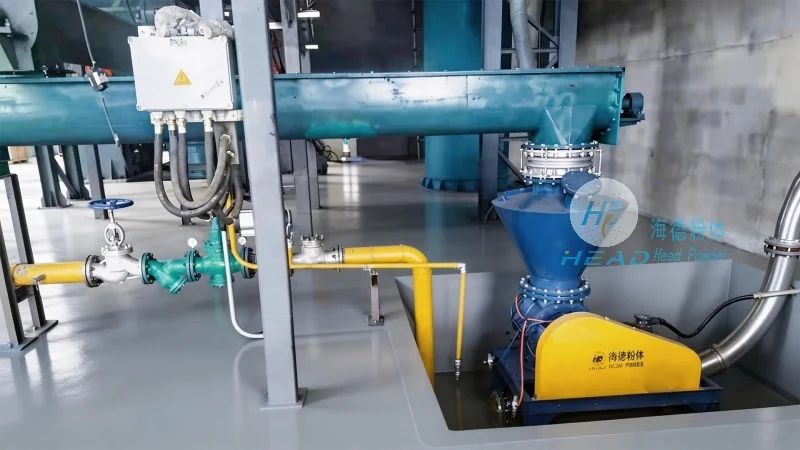
Structural Components and Working Principle
The equipment typically consists of several key components, each playing a crucial role in the overall operation. The main components include a positive pressure blower or compressor, a hopper or feeder for material loading, a pipeline system with appropriate fittings and valves, and a receiver or discharge unit at the end of the line. The working principle involves the blower generating a high-pressure air stream that draws the powder from the hopper into the pipeline. The powder is then suspended in the air stream and transported through the pipeline to the receiver. The receiver is designed to separate the powder from the air, typically using a cyclone or other separation equipment, and collects the material for further processing or storage.
Applications and Industries
Positive pressure dilute phase powder transport equipment is versatile and can be applied to a wide range of industries. In the chemical industry, it is used for transporting raw materials such as powders, granules, and fine particles. In the food and pharmaceutical sectors, the equipment ensures that powders are handled in a hygienic and controlled manner, meeting stringent quality and safety standards. The mining industry also benefits from this technology for transporting ore powders from processing plants to storage or for further treatment. Additionally, in the agricultural sector, it can be used for the transport of fertilizers and other agricultural powders, enhancing the efficiency of supply chains.
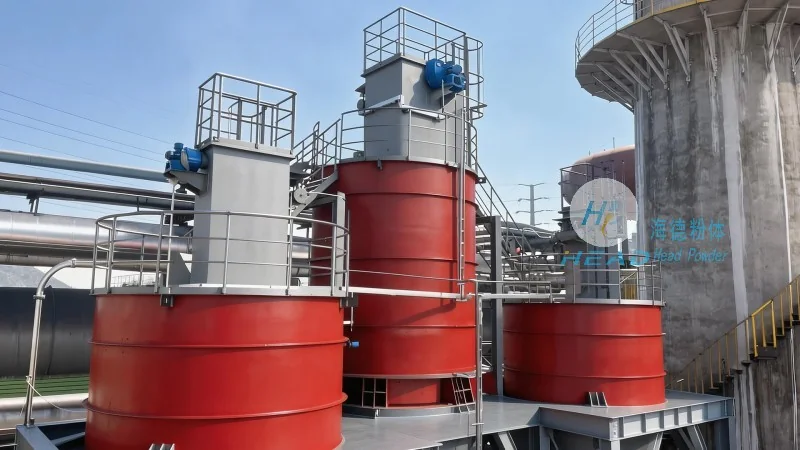
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling and transport solutions, specializes in the design, manufacturing, and supply of positive pressure dilute phase powder transport equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries requiring reliable and efficient powder transport systems. HeadPowder's products are engineered to meet the specific needs of various applications, ensuring optimal performance and durability. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing capabilities and technical expertise to deliver high-quality equipment to global markets.




