For industries that handle fine powders, efficient material transport is essential to maintain production efficiency and product quality. Fine powder pneumatic conveying equipment, also known as powder handling systems, utilizes air or gas as the primary medium to move powders from one location to another. This technology is particularly important in sectors such as pharmaceuticals, food processing, chemicals, and minerals, where maintaining the integrity of the powder is critical. The equipment is designed to minimize product degradation, prevent contamination, and ensure consistent flow rates, making it a preferred choice for many industrial applications.
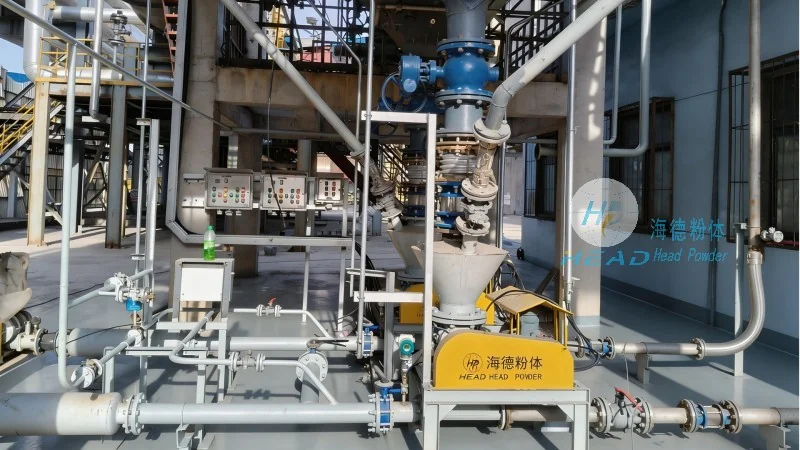
Key Components of a Fine Powder Pneumatic Conveying System
A typical fine powder pneumatic conveying system consists of several interconnected components that work together to achieve effective material transport. The main components include the hopper, which stores the powder; the feeder, which controls the discharge rate; the conveying line, which transports the powder; and the receiver, which collects the material at the destination. Each component is engineered to handle fine powders without causing clogging or particle segregation. The hopper is often equipped with a venting system to manage pressure and prevent dust accumulation. The feeder, such as a rotary valve or a screw feeder, regulates the flow of powder into the conveying line. The conveying line is typically made of stainless steel or other corrosion-resistant materials to ensure durability and prevent contamination. The receiver is designed to collect the powder efficiently and may include a filter or dust collection system to maintain air quality.
Working Principle of Pneumatic Conveying for Fine Powders
The operation of fine powder pneumatic conveying systems is based on the principle of creating a pressure differential or using vacuum to move the powder particles. In positive pressure systems, compressed air is introduced into the hopper, which forces the powder into the conveying line. The air velocity is carefully controlled to ensure that the powder particles are carried along without being damaged or separated. In negative pressure (or vacuum) systems, a vacuum is created at the receiver end, drawing the powder from the hopper through the line. The air flow rate and velocity are critical parameters that determine the efficiency and capacity of the system. Proper design of the air nozzles and the conveying line geometry ensures that the powder particles remain suspended and transported effectively.
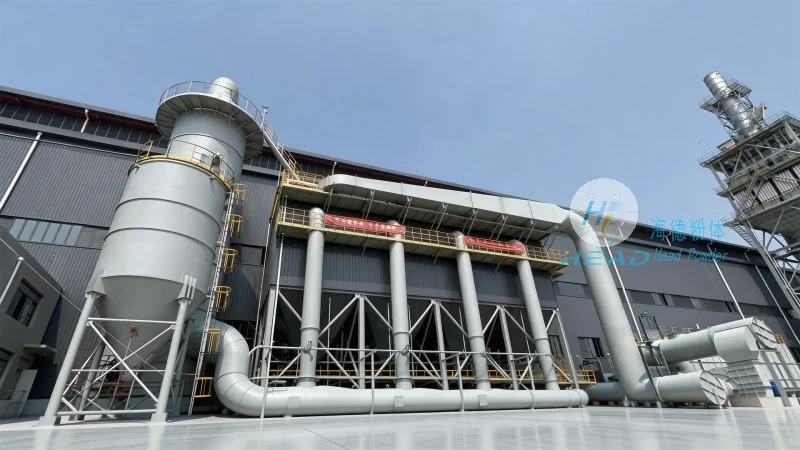
Applications and Benefits of Fine Powder Pneumatic Conveying
Fine powder pneumatic conveying equipment is widely utilized across various industries due to its versatility and efficiency. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final product meets stringent quality standards. In food processing, they handle ingredients like flour, sugar, and spices, maintaining hygiene and preventing cross-contamination. The chemical industry uses pneumatic conveying for transporting powders like pigments, catalysts, and reagents, where controlling particle size and flow is essential. Additionally, in the minerals and mining sector, these systems are employed to transport raw materials and finished products, improving overall process efficiency.
Advantages of Using Fine Powder Pneumatic Conveying Systems
Compared to traditional material handling methods like belt conveyors or bucket elevators, fine powder pneumatic conveying offers several advantages. One of the key benefits is the ability to handle fine powders without causing segregation or agglomeration. The enclosed system prevents dust emissions, reducing environmental impact and improving workplace safety. Another advantage is the flexibility in system design, allowing for customized solutions to meet specific production requirements. These systems can be scaled up or down to accommodate varying production volumes and can be integrated with other processing equipment for a seamless workflow. Furthermore, pneumatic conveying systems are relatively low maintenance, as they have fewer moving parts compared to mechanical conveyors, reducing downtime and operational costs.
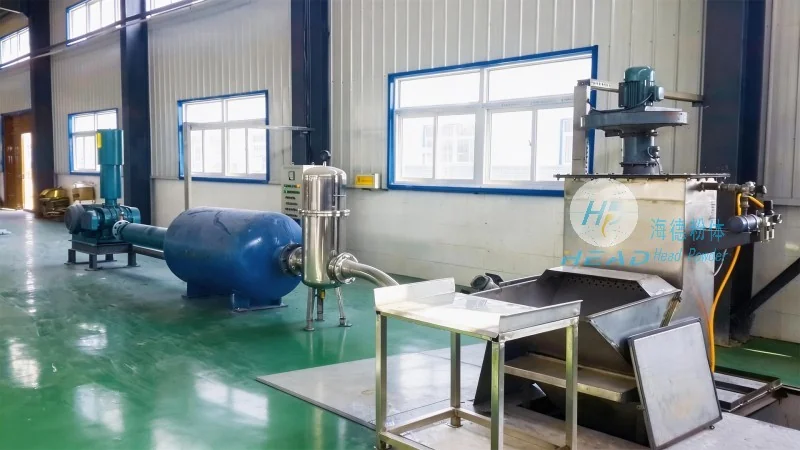
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a reputable manufacturer specializing in the design and production of fine powder handling equipment. The company is headquartered in Shandong, China, and has built a strong reputation for delivering high-quality, reliable pneumatic conveying systems. HeadPowder focuses on innovation, using advanced engineering and materials to develop solutions that meet the evolving needs of the industry. The company provides customized equipment tailored to the specific requirements of each client, ensuring optimal performance and efficiency. With a commitment to quality and customer satisfaction, HeadPowder has established itself as a trusted partner in the field of powder handling technology.




