

Working Principle and Features of Dust-Free Feeding Pneumatic Conveying Systems
For industries that require precise material handling with minimal contamination, dust-free feeding pneumatic conveying systems offer a reliable solution. These systems are engineered to transport bulk materials efficiently while maintaining a clean and controlled environment. In this article, we will explore the working principle and key features of such systems, highlighting how they contribute to operational efficiency and product integrity.
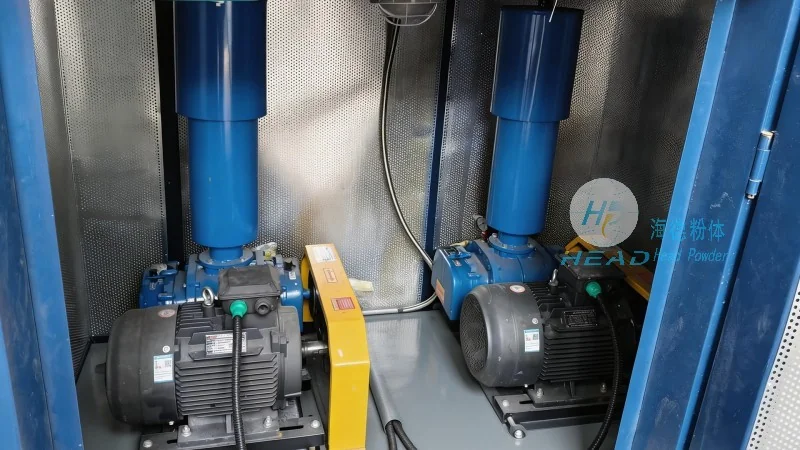
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in industrial material handling equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the field of pneumatic conveying technology. HeadPowder's commitment to excellence is reflected in its state-of-the-art manufacturing facilities and rigorous quality control processes, ensuring that every product meets the highest industry standards.
Introduction to Dust-Free Feeding Pneumatic Conveying Systems
Dust-free feeding pneumatic conveying systems are designed to transport dry bulk materials from a source to a destination without generating dust or contamination. This is achieved through the use of pressurized or vacuum air to move materials through a sealed pipeline system. The systems are particularly suitable for applications where material purity is critical, such as in pharmaceuticals, food processing, and chemical industries.
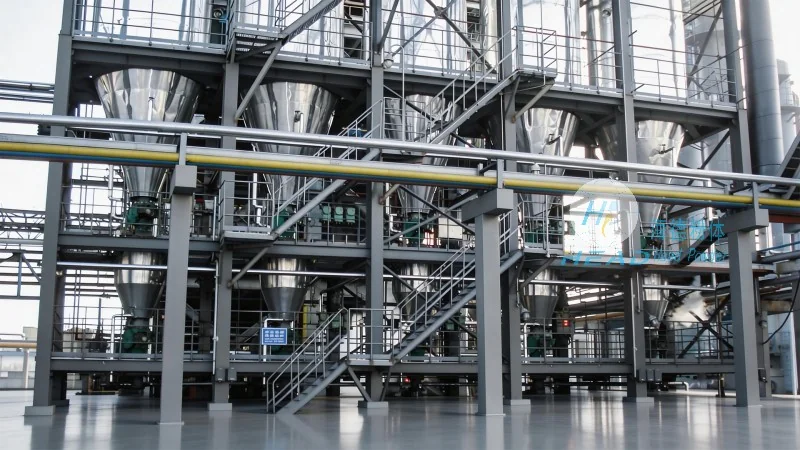
Working Principle of the System
The core working principle of a dust-free feeding pneumatic conveying system involves the use of a blower or compressor to generate airflow within a sealed pipeline. The material to be conveyed is introduced into the system, typically via a hopper or feeder, and is then entrained by the air stream. As the air and material mixture travels through the pipeline, it is directed to the desired destination, such as a silo, storage tank, or processing unit. The system maintains a positive pressure or vacuum to ensure that no dust escapes into the surrounding environment, thus preserving material integrity and workplace safety.
Key Features and Advantages
Several key features distinguish dust-free feeding pneumatic conveying systems from traditional methods. Firstly, the sealed pipeline design eliminates the risk of dust contamination, making it ideal for applications where product purity is paramount. Secondly, the system offers high efficiency in material transport, with the ability to handle a wide range of materials, including powders, granules, and fine particles. Additionally, the systems are compact and can be integrated into existing production lines with minimal modifications. The use of advanced control systems allows for precise regulation of airflow and material flow, ensuring consistent performance and reducing downtime.
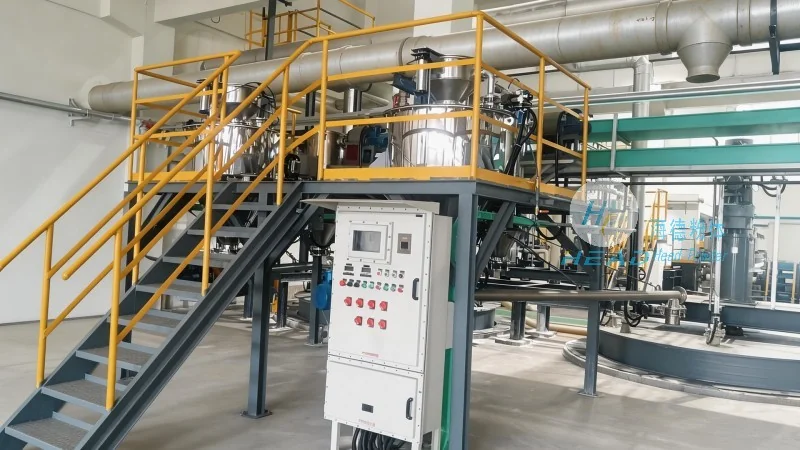
Application-Specific Benefits
In industries like pharmaceuticals, dust-free feeding systems are essential for maintaining compliance with stringent regulatory standards. By preventing cross-contamination and ensuring material purity, these systems help manufacturers meet quality control requirements and enhance product safety. Similarly, in food processing, the sealed design prevents the introduction of foreign particles, ensuring that final products meet food safety regulations. The systems also contribute to improved workplace safety by eliminating the need for manual handling of dusty materials, reducing the risk of respiratory issues and other health hazards.
Conclusion
Dust-free feeding pneumatic conveying systems represent a significant advancement in material handling technology, offering a combination of efficiency, safety, and product integrity. With their ability to transport materials without generating dust, these systems are becoming increasingly popular in industries where contamination control is critical. As a leading manufacturer, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide high-quality solutions that meet the evolving needs of modern industrial applications.