

Working Principle and Features of Glucose Pneumatic Conveying Systems
Glucose pneumatic conveying systems are advanced industrial equipment designed to transport granular or powdered materials, such as glucose, efficiently and safely. These systems utilize air or gas as the conveying medium to move materials from one location to another without the need for mechanical components like belts or buckets. The core of these systems lies in their ability to handle delicate materials like glucose, ensuring minimal product degradation and maintaining product quality throughout the conveying process.
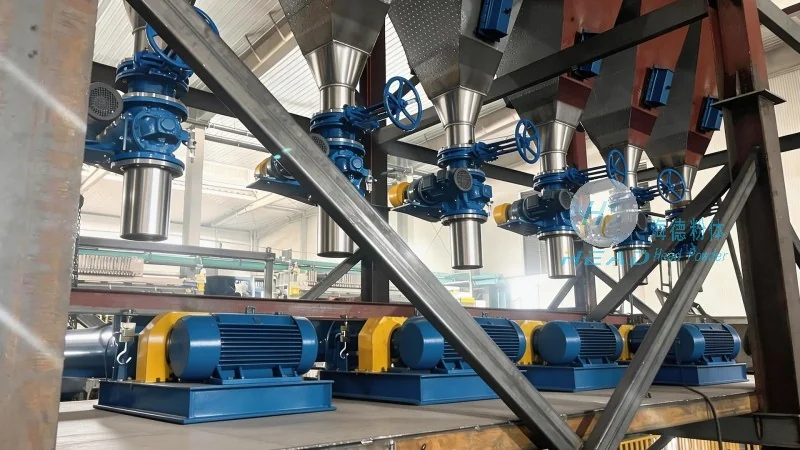
HeadPowder, a leading manufacturer in the field, specializes in developing and supplying high-quality glucose pneumatic conveying solutions. With a strong focus on innovation and precision engineering, the company has established itself as a trusted partner for industries requiring reliable material handling equipment. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility dedicated to producing robust and efficient conveying systems.
The Working Principle of Glucose Pneumatic Conveying Systems
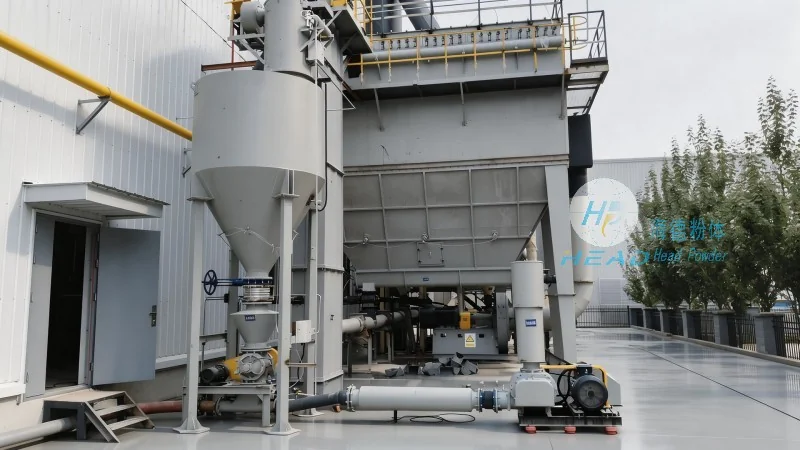
At the heart of a glucose pneumatic conveying system is the pneumatic transport mechanism, which operates on the principle of air flow. The system typically consists of a hopper, a conveying line, and a receiver. The process begins when the glucose is fed into the hopper. A fan or blower then generates a high-velocity air stream, which draws the glucose particles into the conveying line. The air and material mixture travels through the pipeline under pressure, ensuring that the material is transported to the desired destination. Once the material reaches the receiver, the air is separated from the product, often through a cyclone separator or a filter, allowing the glucose to be collected in its pure form.
Key components of the system include the air compressor, which provides the necessary pressure and airflow; the hopper, which stores and feeds the glucose; the conveying line, which is usually made of stainless steel to prevent contamination and ensure durability; and the receiver, which collects the conveyed material. The design of these components is critical to the system's performance, as they must work in harmony to achieve efficient and consistent material transport.
Key Features of Glucose Pneumatic Conveying Systems
Glucose pneumatic conveying systems offer several advantages that make them ideal for handling sensitive materials like glucose. One of the primary features is their ability to maintain product integrity. Unlike mechanical conveying methods, which can cause abrasion or breakage of the particles, pneumatic systems use air to move the material, reducing the risk of product damage. This is particularly important for glucose, which is often used in pharmaceutical and food industries where product quality is paramount.
Another significant feature is the system's flexibility. Glucose pneumatic conveying systems can be configured to handle various material types and flow rates, making them adaptable to different production needs. They can also be integrated with other processing equipment, such as mixers or dryers, to create a seamless material handling process. The systems are also designed for easy maintenance, with components that are easy to access and replace, reducing downtime and operational costs.
Efficiency and Reliability in Material Handling
Efficiency is a key characteristic of glucose pneumatic conveying systems. By using air as the conveying medium, these systems can transport materials over long distances with minimal energy consumption compared to traditional methods. The high-velocity air stream ensures that the material is moved quickly and consistently, reducing the time required for material transfer. Additionally, the systems are designed to operate continuously, with minimal interruptions, which enhances overall production efficiency.
Reliability is another critical feature. HeadPowder's systems are built with high-quality materials and components, ensuring long-term performance and durability. The company's commitment to quality control ensures that each system meets strict industry standards, providing customers with reliable equipment that can handle the demands of continuous production. The systems are also equipped with safety features, such as pressure relief valves and air filters, to prevent accidents and ensure safe operation.
Application in the Glucose Industry
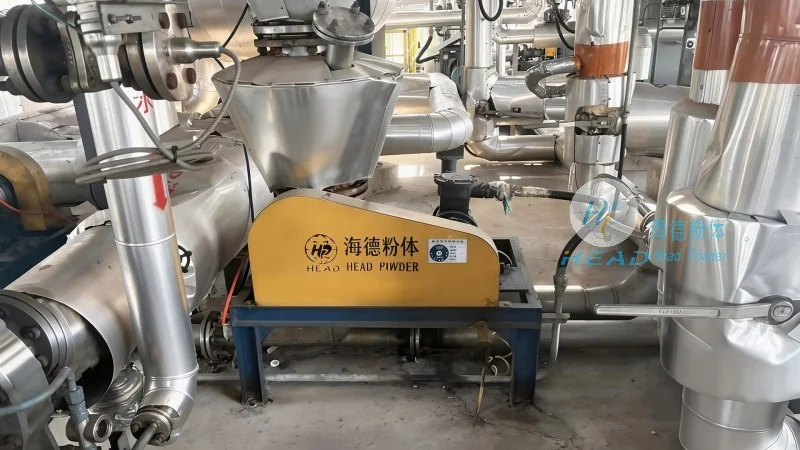
Glucose pneumatic conveying systems are widely used in the glucose industry for various applications, including the transport of raw materials, intermediate products, and finished goods. In the production of glucose, these systems are essential for moving the material from storage to processing equipment, such as reactors or crystallizers. The ability to handle large volumes of material efficiently makes these systems indispensable in modern glucose production facilities.
The systems are also used in downstream processes, such as packaging and distribution. By ensuring that the glucose is transported without contamination or degradation, the systems help maintain the quality of the final product. This is particularly important for glucose used in food and pharmaceutical applications, where product purity is a critical factor.
Conclusion
Glucose pneumatic conveying systems, as provided by HeadPowder, are advanced solutions for efficient and reliable material handling in the glucose industry. With their ability to maintain product integrity, flexibility, and high efficiency, these systems offer significant advantages over traditional conveying methods. HeadPowder's commitment to quality and innovation ensures that customers receive top-tier equipment that meets their specific needs. Based in Shandong, China, the company continues to lead the industry in developing cutting-edge material handling solutions, supporting the growth and success of its clients in the glucose sector.