

Working Principle and Features of Corn Starch Pneumatic Conveying Systems
Corn starch is a vital raw material in various industries, including food processing, pharmaceuticals, and cosmetics. Efficient and reliable material handling is crucial for maintaining product quality and operational efficiency. Pneumatic conveying systems have emerged as a preferred solution for transporting corn starch, offering advantages over traditional methods like belt conveyors or bucket elevators. This article explores the working principle and key features of corn starch pneumatic conveying lines, highlighting their role in modern industrial applications.
The Working Principle of Corn Starch Pneumatic Conveying Systems
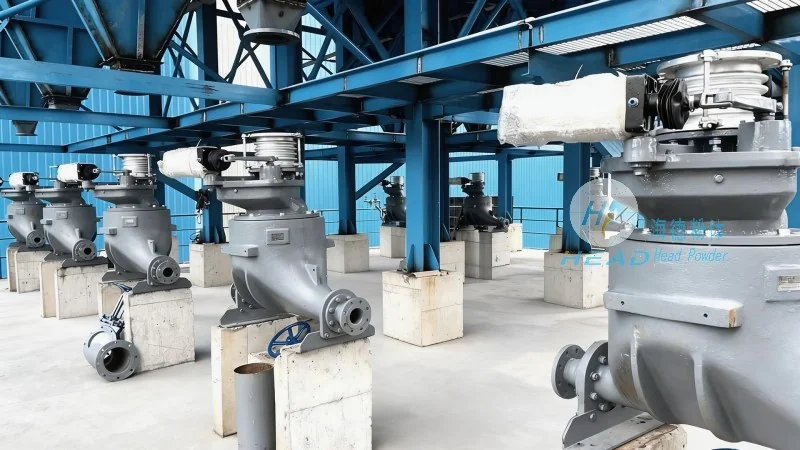
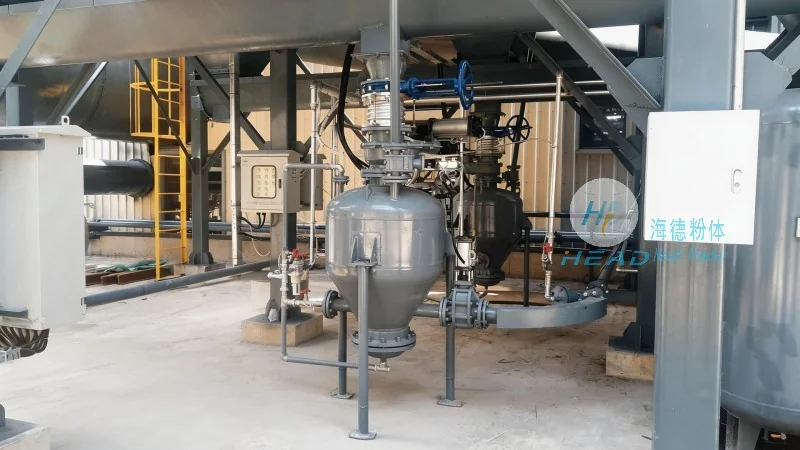
At the core of a corn starch pneumatic conveying system is the use of air to transport bulk materials. The system operates by creating a pressure differential between the intake and discharge points. There are two primary types of pneumatic conveying: positive pressure and negative pressure systems. Positive pressure systems generate air pressure at the material inlet, pushing the corn starch through the pipeline. Negative pressure systems, on the other hand, create a vacuum at the discharge end, drawing the material into the system. For corn starch, which is a fine powder, positive pressure systems are often preferred as they provide better control over flow and reduce the risk of material degradation. The process typically involves a hopper where corn starch is stored, a feeder that meters the material into the pipeline, and a conveyor line with appropriate ductwork. The air is introduced at a controlled rate, ensuring the corn starch particles are suspended and transported to the destination. The system may also include filters and cyclones to separate the air from the material at the discharge point, maintaining a clean and efficient operation.
Key Features and Advantages of Corn Starch Pneumatic Conveying Systems
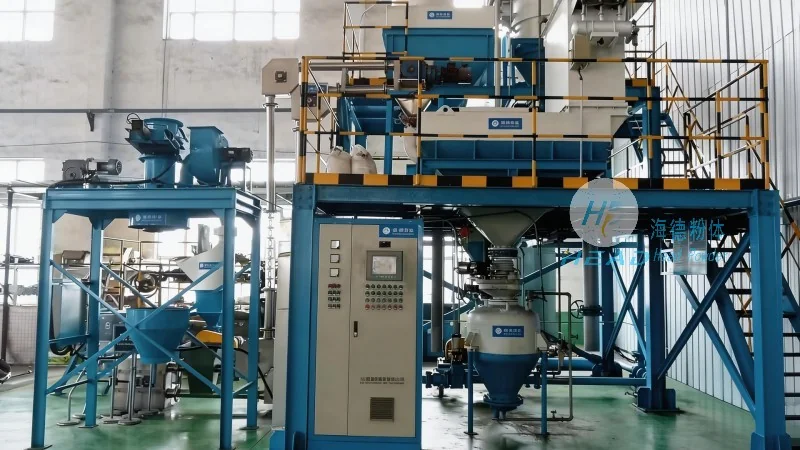
Several distinct features make corn starch pneumatic conveying systems highly effective for industrial use. First, they offer high efficiency in material transport, with the ability to move large volumes of corn starch over long distances with minimal energy consumption compared to mechanical systems. The systems are also known for their cleanliness and hygienic design, which is critical in food and pharmaceutical applications where contamination must be avoided. This is achieved through sealed pipelines and enclosed systems that prevent dust and particulate matter from entering the environment. Another significant advantage is the low risk of material degradation. Unlike mechanical conveyors that may cause friction and heat buildup, pneumatic systems use air to move the material, reducing the chances of clumping or quality loss. Additionally, these systems provide flexibility in layout, allowing for vertical, horizontal, or inclined transport, adapting to the specific requirements of a facility. The ability to integrate with other processing equipment, such as mixers or storage silos, enhances overall operational efficiency. Furthermore, modern pneumatic conveying systems are equipped with advanced controls and monitoring systems, enabling real-time adjustments to flow rates and pressure, ensuring optimal performance and minimizing downtime.
HeadPowder Engineering's Expertise in Corn Starch Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the needs of the corn starch industry. With years of experience and a commitment to innovation, HeadPowder provides customized solutions that meet the unique challenges of material handling in food processing and related sectors. The company's engineers work closely with clients to understand their operational requirements, including production capacity, material characteristics, and facility layout, to design systems that maximize efficiency and reliability. HeadPowder utilizes high-quality components and materials, ensuring durability and long-term performance. The company's focus on customer satisfaction is evident in its comprehensive after-sales support, including maintenance services and technical assistance. By leveraging advanced technology and industry best practices, HeadPowder delivers pneumatic conveying systems that not only meet but exceed industry standards, helping clients improve their production processes and maintain product quality. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with the latest equipment and testing capabilities.