Wheat bran, a byproduct of wheat processing, is widely utilized in animal feed, food additives, and various industrial applications. Efficient and reliable powder conveying systems are essential for handling wheat bran, as they ensure minimal material loss and maintain product quality. This article delves into the working principle and key characteristics of wheat bran powder conveying systems, highlighting the technology and features that make them effective for industrial use.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier of powder handling equipment based in Shandong, China. With extensive experience in the industry, HeadPowder specializes in designing and producing customized powder conveying solutions tailored to the unique requirements of sectors such as food processing, agriculture, and chemical manufacturing. The company’s headquarters is located in Shandong, China, providing a robust foundation for serving clients globally with high-quality equipment and technical support.
Working Principle of Wheat Bran Powder Conveying Systems
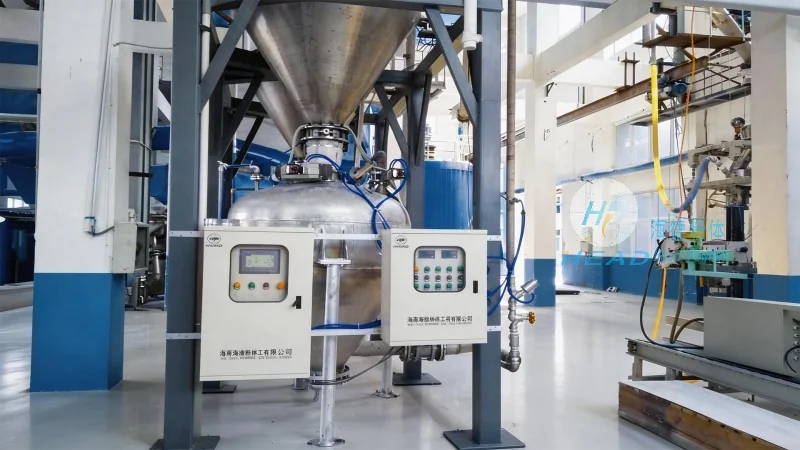
The working principle of wheat bran powder conveying systems typically involves pneumatic or mechanical methods to transport bulk powder materials. Pneumatic conveying systems utilize compressed air to create a flow that moves the wheat bran through pipes, making them particularly effective for fine powders like wheat bran. This method minimizes product degradation and contamination by maintaining an enclosed environment. The system generally includes a hopper, a conveyor line, and a receiver. Wheat bran is fed into the hopper, drawn into the conveyor line by air flow, and travels through pipes to the receiver where powder is separated from air and collected. Mechanical conveying systems, such as screw or belt conveyors, use mechanical components to move the powder. These are often adapted for materials with higher moisture or larger particle sizes but can also handle wheat bran. The mechanical parts rotate to push the powder forward, ensuring consistent and controlled movement.
Key Characteristics of Wheat Bran Powder Conveying Systems
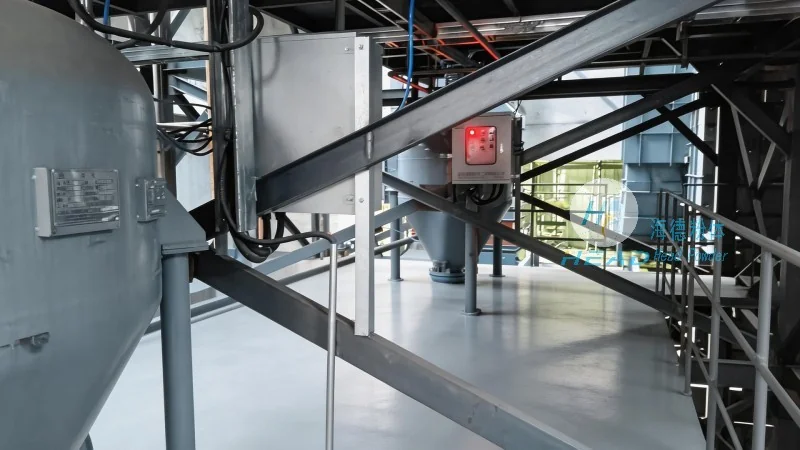
Wheat bran powder conveying systems exhibit several critical characteristics for industrial applications. One primary characteristic is efficiency, as these systems can handle large volumes of wheat bran with minimal downtime. They are designed to preserve product integrity, preventing clumping, agglomeration, or contamination during transport. Another key characteristic is flexibility, allowing customization to meet specific operational needs. This includes adjustable conveying speeds, different pipe configurations, and integration with other processing equipment. Environmental friendliness is also a notable feature, as enclosed pipes contain dust and prevent environmental pollution. Additionally, these systems offer low maintenance requirements, with durable components that can withstand the abrasive nature of wheat bran particles. The ability to handle varying particle sizes and moisture levels is another advantage, ensuring consistent performance across different production stages.
Benefits of Using Wheat Bran Powder Conveying Systems
Implementing wheat bran powder conveying systems provides numerous benefits for industrial operations. The primary benefit is improved productivity, as these systems enable faster and more reliable material transport compared to manual handling. This leads to increased throughput and reduced labor costs. Maintaining product quality is another significant advantage, as the enclosed and controlled environment minimizes exposure to moisture, air, and contaminants, preserving the nutritional value and quality of the wheat bran. Cost savings are also realized through reduced material loss and lower maintenance expenses. The systems are designed for durability, with components that can handle the abrasive nature of wheat bran, reducing the frequency of repairs and replacements. Furthermore, the flexibility of these systems allows for easy integration into existing production lines, minimizing disruptions during setup and operation. The environmental benefits, such as reduced dust emissions and improved safety, contribute to a more sustainable and compliant operation.
Application Examples in the Food and Agriculture Industry
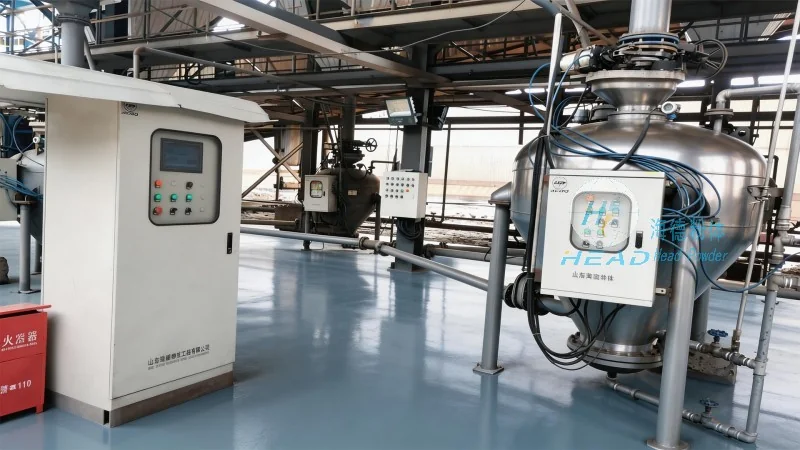
Wheat bran powder conveying systems are widely used in the food and agriculture industry for various applications. In animal feed production, these systems efficiently transport wheat bran from storage silos to feed mixers, ensuring consistent ingredient ratios and preventing contamination. In food processing, they are used to move wheat bran into processing lines for making bread, pastries, and other baked goods. The systems are also utilized in the production of nutritional supplements, where precise dosing and handling of wheat bran are critical. Additionally, in agricultural settings, they help in the distribution of wheat bran as a soil amendment or animal feed supplement, improving crop yields and livestock health. The adaptability of these systems to different production scales and environments makes them a versatile solution for various industrial needs.
Conclusion
Wheat bran powder conveying systems are essential for efficient and reliable handling of wheat bran in industrial applications. The working principle, which often involves pneumatic or mechanical methods, ensures minimal product loss and maintains quality. Key characteristics such as efficiency, flexibility, and environmental friendliness make these systems suitable for diverse industries. By implementing such systems, companies can enhance productivity, reduce costs, and improve overall operational performance. Shandong HeadPowder Engineering Co., Ltd. offers customized solutions tailored to the specific needs of clients, providing high-quality equipment and technical support to meet the demands of the modern industrial landscape.




