For industrial applications dealing with fly ash handling, the fly ash silo powder pneumatic conveying line is a critical system designed to efficiently transport fly ash from storage silos to processing or disposal units. This system, developed by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, combines advanced pneumatic conveying technology with robust silo storage solutions to ensure reliable and safe material transport. The following sections will delve into the working principle and key features of this essential equipment.
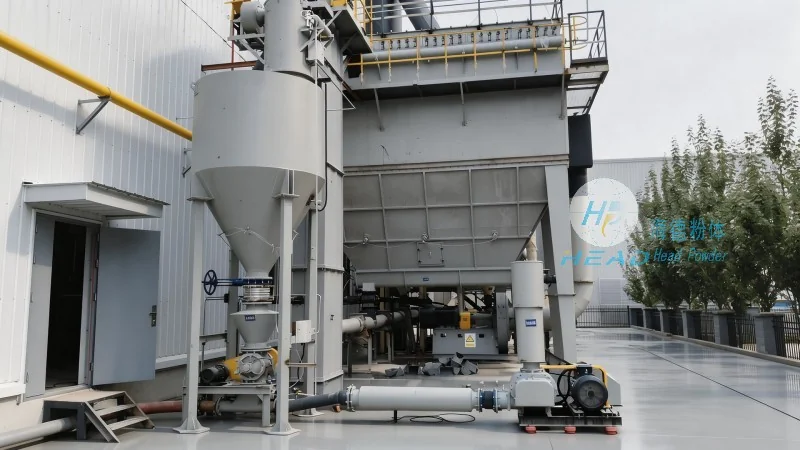
Working Principle of the Fly Ash Silo Powder Pneumatic Conveying Line
The fly ash silo powder pneumatic conveying line operates on the principle of air pressure to move dry powder materials. The system typically consists of a fly ash silo, a pneumatic conveying pipeline, a control system, and a discharge unit. When the system is activated, compressed air is introduced into the silo, creating a pressure differential that lifts the fly ash particles and propels them through the pipeline to the destination. The control system monitors the pressure, flow rate, and other parameters to maintain optimal operation, ensuring consistent and efficient material transfer. The discharge unit at the end of the pipeline then releases the fly ash into the next processing stage, completing the conveying process.
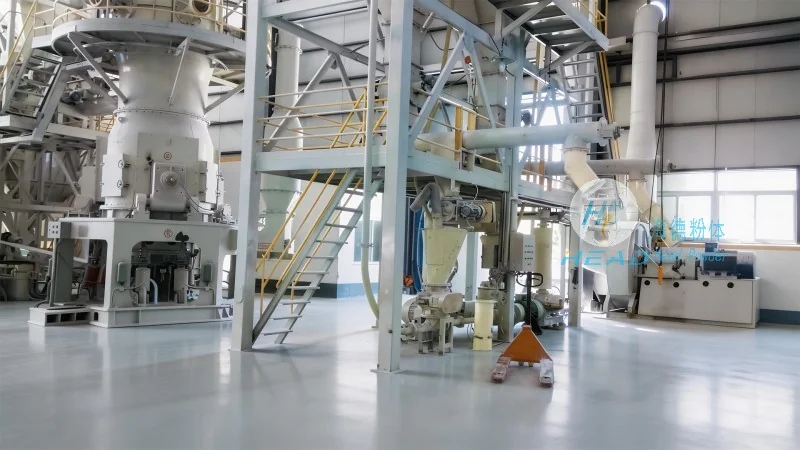
Key Features of the Fly Ash Silo Powder Pneumatic Conveying Line
Shandong HeadPowder Engineering Co., Ltd. has integrated several advanced features into the fly ash silo powder pneumatic conveying line to enhance performance and reliability. One of the primary features is the high-efficiency pneumatic conveying technology, which minimizes material degradation and ensures a smooth flow of fly ash. The system is also equipped with a robust silo design that provides stable storage and prevents material segregation, maintaining consistent material quality. Additionally, the control system offers real-time monitoring and adjustable parameters, allowing operators to optimize the conveying process based on specific requirements. The pipeline design incorporates corrosion-resistant materials and smooth internal surfaces to reduce friction and prevent blockages, ensuring long-term durability and low maintenance costs. Another notable feature is the safety mechanisms integrated into the system, including pressure relief valves and overfill prevention devices, which enhance operational safety and compliance with industrial standards. The overall design is compact and modular, making it suitable for various industrial settings and easy to integrate with existing infrastructure.
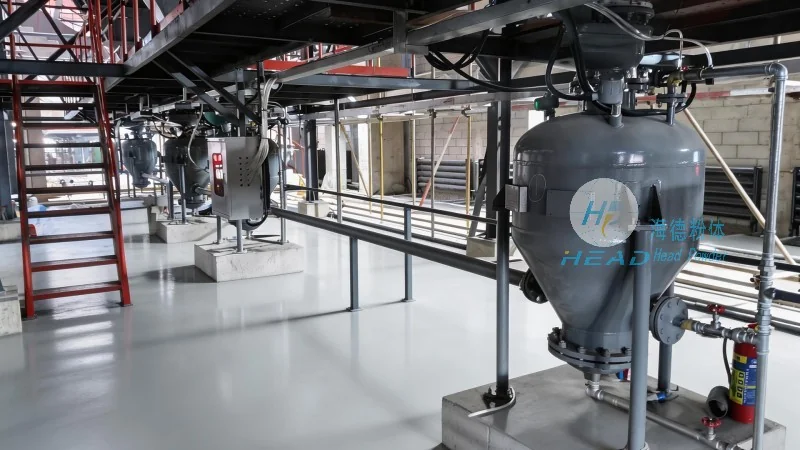
Application and Benefits
The fly ash silo powder pneumatic conveying line is widely used in power plants, cement factories, and other industrial facilities that generate or process fly ash. The primary benefits of this system include improved material handling efficiency, reduced labor costs, and enhanced safety compared to traditional methods like manual handling or truck transport. By automating the conveying process, the system minimizes the risk of dust exposure and accidents, contributing to a safer working environment. The consistent flow rate and pressure control also ensure that downstream processes receive a steady supply of fly ash, improving overall production efficiency. Furthermore, the system's low maintenance requirements and long service life reduce operational costs over time, making it a cost-effective solution for long-term material transport needs. The modular design allows for easy expansion or modification as production needs change, providing flexibility for growing industrial operations.




