Working Principle and Features of Stone Aggregate Powder Pneumatic Conveying Systems
Release time:2026-09-18 04:01:23
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced pneumatic conveying solutions for stone aggregate powders. This article explores the working principle and key features of their systems, providing a comprehensive overview for potential clients and industry professionals.
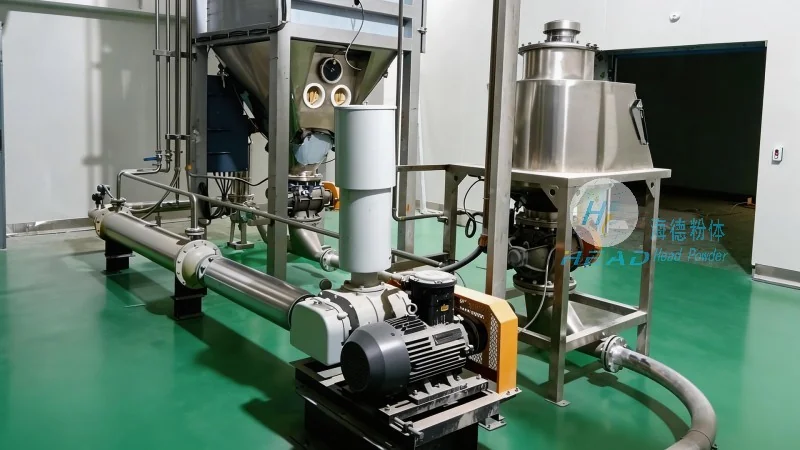
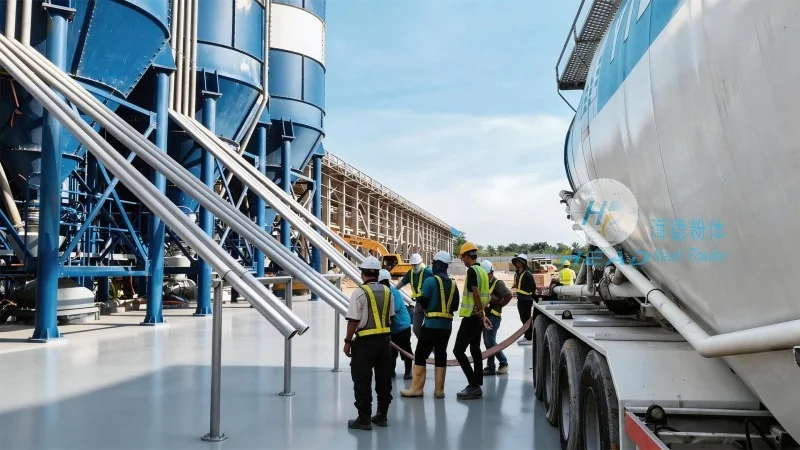
The Working Principle of Pneumatic Conveying Systems for Stone Aggregate Powders
The pneumatic conveying system for stone aggregate powders operates by utilizing compressed air to transport dry bulk materials. The process begins with the material being fed into a hopper or silo, where it is then drawn into a pipeline by the air flow. As the air moves through the system, it carries the powder particles along, ensuring efficient and continuous transportation. The system typically includes components such as a blower, ducts, and control valves that work in tandem to regulate the flow and pressure. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and operational costs. The air pressure and velocity are carefully controlled to prevent material degradation and ensure smooth transport, making it ideal for handling abrasive and heavy stone aggregates.
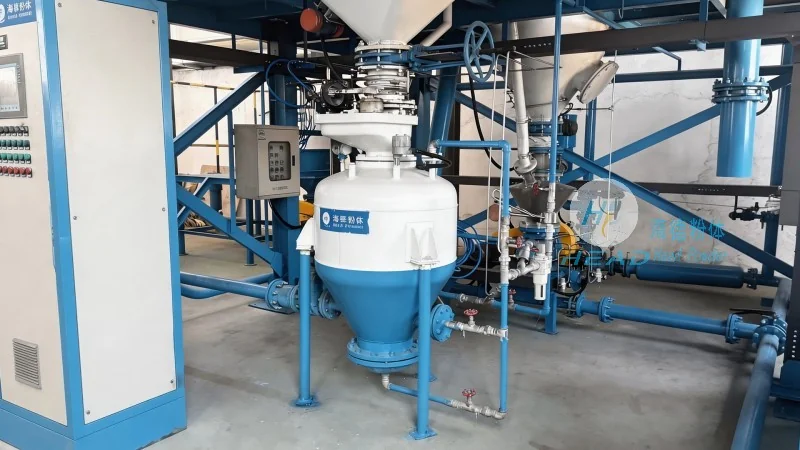
Key Features of Stone Aggregate Powder Pneumatic Conveying Systems
HeadPowder's pneumatic conveying systems for stone aggregates offer several distinct advantages that set them apart in the industry. Firstly, the systems are highly efficient in terms of material handling, capable of transporting large volumes of powder with minimal energy consumption. The design minimizes product degradation, preserving the quality of the stone aggregates during transport. Additionally, the systems are flexible and can be customized to suit various production requirements, including different material types and processing capacities. Another notable feature is the reduced maintenance needs, as there are fewer moving parts compared to traditional mechanical conveyors. This leads to lower operational costs and increased reliability. The systems also provide better safety by eliminating the risk of dust explosions, as the material is contained within the air stream. Furthermore, the compact design allows for easy integration into existing production lines, making it a practical solution for both new and retrofit applications.
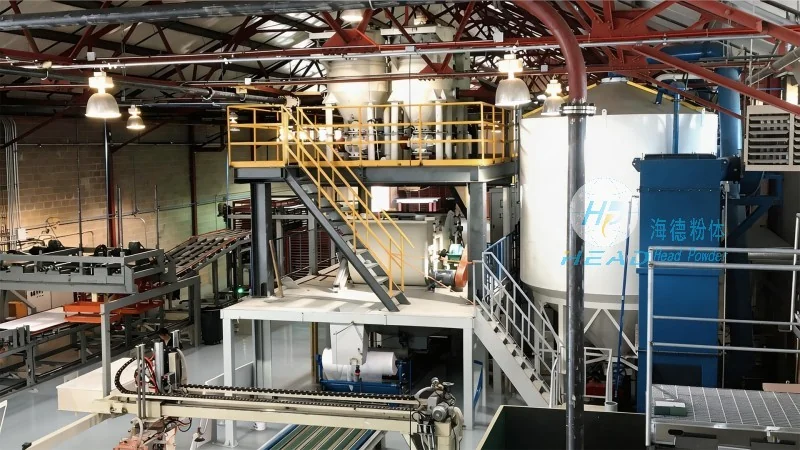
Advantages in Practical Applications
When considering the implementation of a pneumatic conveying system for stone aggregate powders, several practical advantages become evident. The system's ability to handle abrasive materials without wear and tear on components is a significant benefit. This extends the lifespan of the equipment and reduces downtime. The uniform flow of material also ensures consistent quality in downstream processes, such as mixing or packaging. For industries that require high throughput, the system's capacity to transport large volumes in a continuous manner is crucial. Additionally, the reduced noise levels compared to mechanical conveyors contribute to a safer and more comfortable working environment. The environmental benefits are also noteworthy, as the enclosed system prevents dust from escaping into the air, improving workplace safety and compliance with environmental regulations. Overall, the combination of efficiency, reliability, and safety makes these systems a preferred choice for many manufacturers dealing with stone aggregates.




