HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems. This article explores the fundamental principles of the suction-pressure mixed pneumatic conveying system and highlights its key working scene characteristics, providing a comprehensive understanding of this innovative equipment.
The Principle of Suction-Pressure Mixed Pneumatic Conveying System
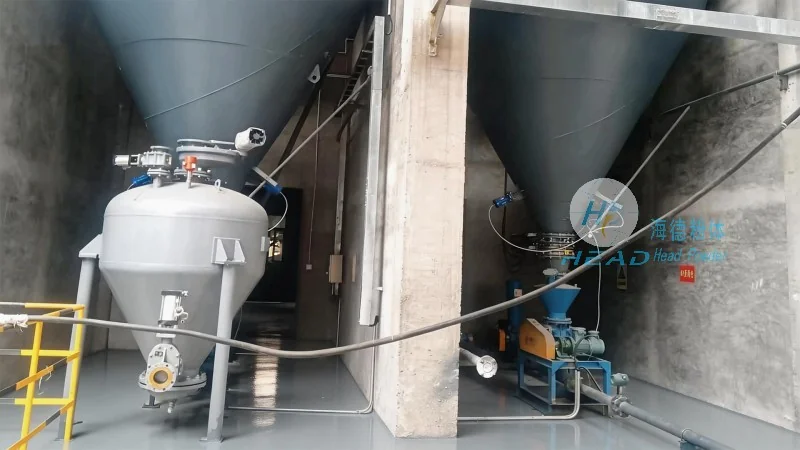
The suction-pressure mixed pneumatic conveying system combines the advantages of both suction and pressure conveying methods, offering a versatile solution for material handling in various industries. At its core, the system operates by utilizing a combination of negative pressure (suction) and positive pressure (pressure) to transport bulk materials through a sealed pipeline network. The process begins with the material being fed into the system via an appropriate feeder, such as a rotary valve or a vacuum feeder. The feeder then introduces the material into the conveying line, where it is carried by a flow of air. The air flow is generated by a blower or a vacuum pump, which creates the necessary pressure differential to move the material. The system's design allows for the seamless transition between suction and pressure modes, enabling it to handle a wide range of materials, including powders, granules, and even bulk solids with varying particle sizes and moisture content. The mixed operation ensures efficient material transport while maintaining the integrity of the conveyed material, minimizing degradation or contamination.
Key Working Scene Characteristics
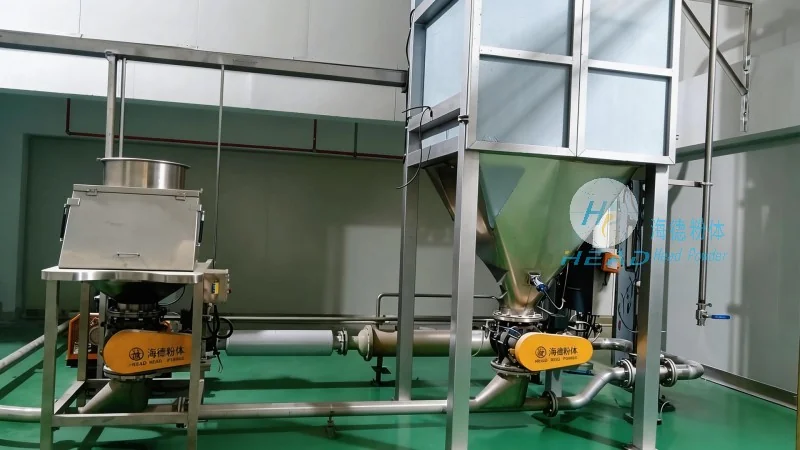
The suction-pressure mixed pneumatic conveying system is particularly well-suited for applications where flexibility and efficiency are paramount. Its working scene characteristics include:
- Wide Material Compatibility: The system can handle diverse materials, from fine powders to larger granules, making it adaptable to various production processes. This versatility is crucial for industries such as chemical manufacturing, food processing, and pharmaceuticals, where different materials require specialized handling solutions.
- Efficient and Clean Transport: Unlike traditional methods like belt conveyors or bucket elevators, pneumatic conveying offers a dust-free and hygienic transport solution. The sealed pipeline system prevents material spillage and contamination, ensuring compliance with industry standards, especially in food and pharmaceutical sectors. The system also reduces the risk of product degradation due to exposure to air or moisture.
- Space-Saving and Flexible Layout: The pneumatic conveying system utilizes a compact design with flexible pipeline configurations, allowing for installation in confined spaces or complex layouts. This is advantageous in facilities where space is limited or where the production line requires non-linear transport paths. The ability to route the pipeline around obstacles or through multiple processing stages enhances operational flexibility.
- Energy Efficiency and Low Maintenance: Modern suction-pressure mixed systems are engineered for energy efficiency, utilizing advanced blowers and control systems to optimize air usage. The sealed design minimizes air leakage, reducing energy consumption. Additionally, the system's components, such as the feeder and separation equipment, are designed for durability and low maintenance, ensuring long-term operational reliability and cost-effectiveness.
Application Scenarios
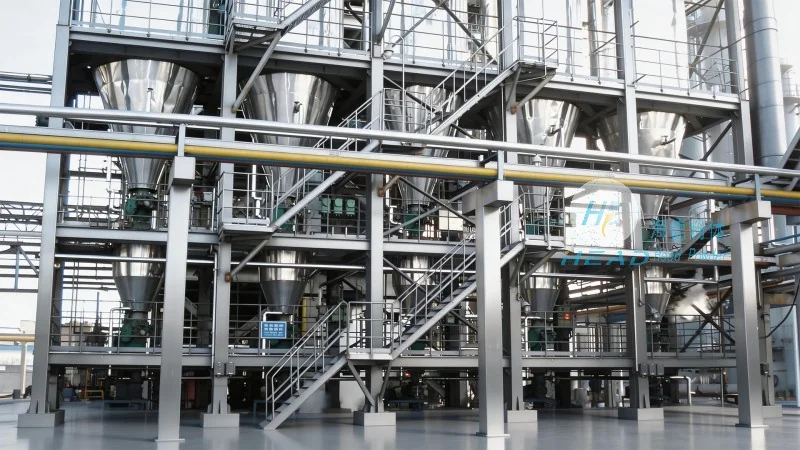
HeadPowder's suction-pressure mixed pneumatic conveying systems are widely applied in several key industries, demonstrating their practical utility and effectiveness. In the chemical industry, the system is used to transport raw materials like powders and granules from storage silos to processing units, ensuring a continuous and controlled supply of materials. The food and beverage sector benefits from the system's hygienic design, which is essential for handling sensitive food products, such as flour, sugar, and spices. Pharmaceutical manufacturers rely on the system's ability to maintain sterile conditions and prevent cross-contamination, making it ideal for transporting active pharmaceutical ingredients (APIs) and other sensitive materials. Additionally, in the agricultural and mining sectors, the system can handle bulk materials like grains, ores, and fertilizers, providing an efficient solution for material transport over long distances or within complex processing facilities.
Conclusion
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers advanced suction-pressure mixed pneumatic conveying systems that integrate the best features of both suction and pressure conveying methods. These systems provide efficient, flexible, and clean material handling solutions for a wide range of industries. By understanding the principles and working scene characteristics of this equipment, businesses can make informed decisions about implementing such systems to enhance their operational efficiency and product quality. HeadPowder's commitment to innovation and quality ensures that their pneumatic conveying solutions meet the evolving needs of modern industrial applications.




