HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced environmental protection pneumatic conveying systems. These systems represent a sophisticated solution for material handling, offering efficient, clean, and sustainable methods for transporting bulk materials. The core of such systems lies in their ability to use air as the primary medium to move powders, granules, and other particulate materials, eliminating the need for traditional mechanical conveyors that often generate dust, noise, and operational inefficiencies.
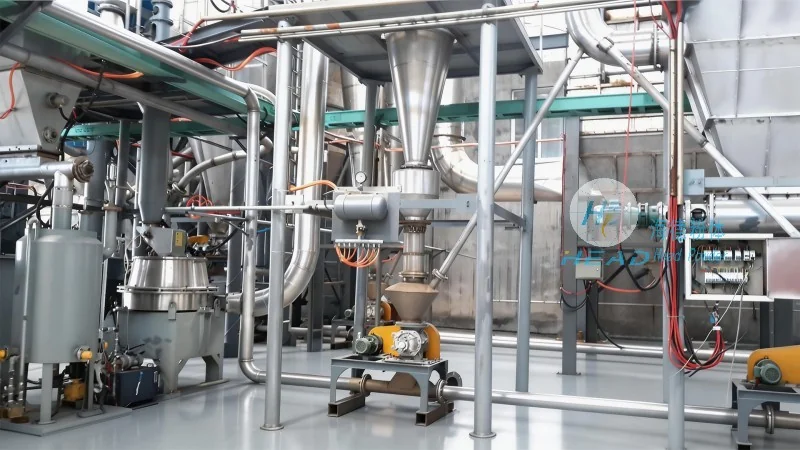
The Fundamental Principles of Pneumatic Conveying
At the heart of environmental protection pneumatic conveying systems is the principle of air-driven material transport. The system operates by creating a pressure differential or using vacuum to move materials through a pipeline. There are two main categories: pressure systems (where air is compressed and introduced at the material source) and vacuum systems (which draw material into a collection point). The choice between these depends on the material characteristics, distance, and required flow rate. For instance, pressure systems are ideal for short to medium distances and high flow rates, while vacuum systems are better suited for longer distances or when material needs to be collected from multiple points.
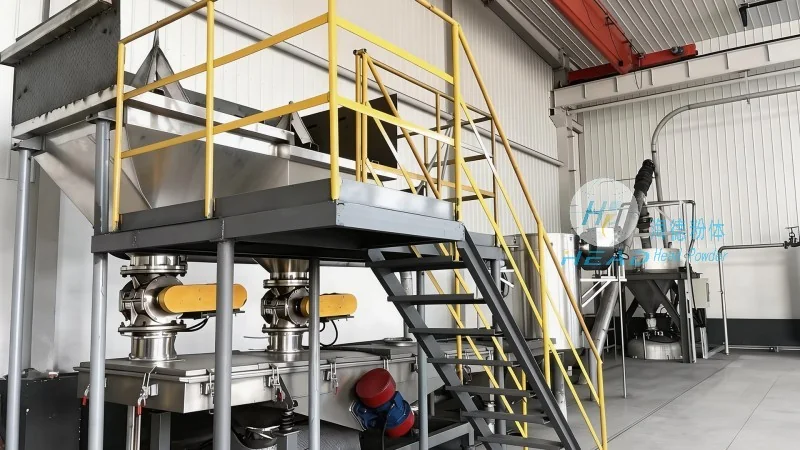
Key Working Scene Characteristics
The working scene characteristics of these systems are tailored to meet diverse industrial needs, ensuring adaptability across various applications. One notable feature is their ability to handle a wide range of materials, from fine powders like cement and flour to bulk granules such as grains or chemicals. This versatility makes them indispensable in sectors like food processing, pharmaceuticals, and chemical manufacturing. Additionally, the systems are designed with environmental considerations in mind, minimizing dust emissions and noise pollution. Advanced models incorporate filtration and dust collection mechanisms to ensure compliance with environmental regulations, making them a sustainable choice for modern industries.
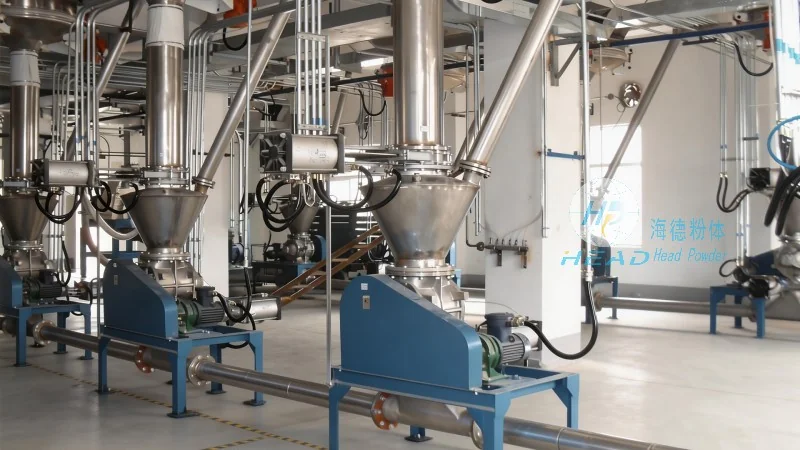
Operational Efficiency and Environmental Benefits
Environmental protection pneumatic conveying systems not only enhance operational efficiency but also provide significant environmental advantages. By eliminating the need for mechanical components like belts or chains, these systems reduce maintenance costs and downtime. The use of air as the conveying medium also minimizes physical contact with materials, preserving product quality and reducing contamination risks. Furthermore, the systems can be integrated with recycling and waste management processes, contributing to a circular economy approach. In industrial settings, this translates to lower energy consumption and reduced carbon footprint, aligning with global sustainability goals.
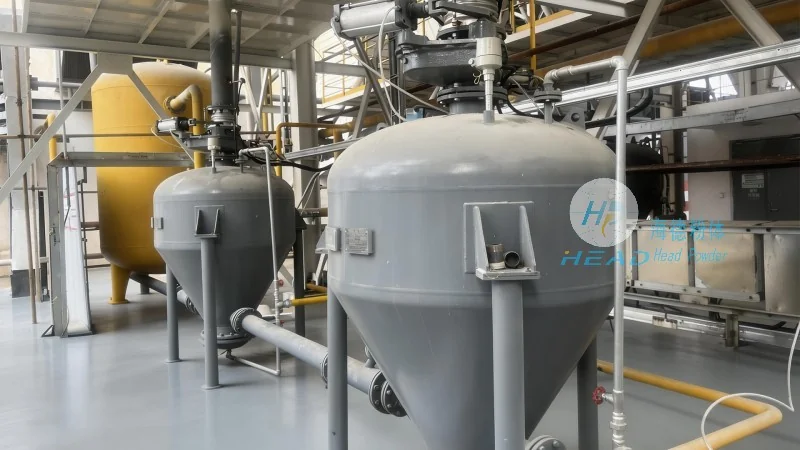
Application Examples and Real-World Impact
HeadPowder's environmental protection pneumatic conveying systems have been successfully implemented in various working scenes. For example, in a food processing plant, the system efficiently transports flour from storage silos to production lines, maintaining hygiene standards and preventing cross-contamination. In a chemical manufacturing facility, it handles hazardous powders with precision, ensuring safety and compliance with regulatory standards. These applications highlight the systems' reliability and adaptability, demonstrating their role in improving productivity while adhering to environmental best practices.




