HeadPowder, a leading provider in the field of powder handling technology, specializes in the design and implementation of efficient conveying systems for various bulk materials. This article delves into the fundamental principles and operational characteristics of oat powder conveying systems, highlighting how such systems are engineered to meet the unique demands of handling oat powders in industrial settings.
Understanding the Core Principles of Oat Powder Conveying Systems
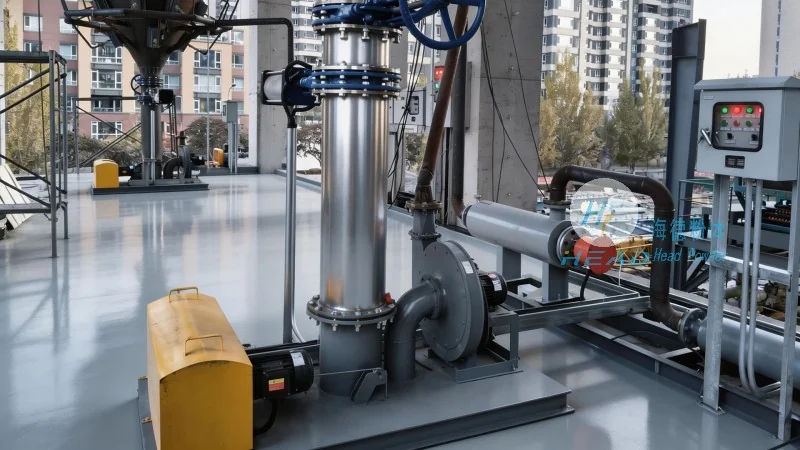
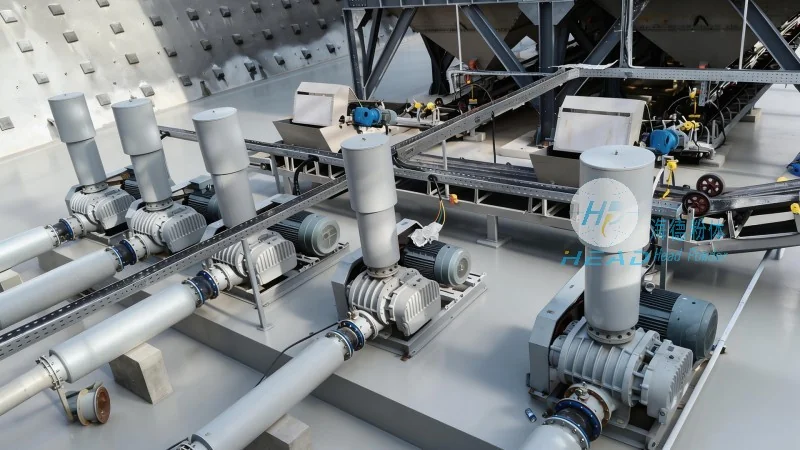
The operation of oat powder conveying systems is grounded in several key principles that ensure reliable and efficient material transport. These systems are typically designed to handle the specific properties of oat powders, which include particle size distribution, moisture content, and flow characteristics. A critical component in such systems is the selection of appropriate conveying equipment, which may include screw conveyors, pneumatic conveyors, or bucket elevators, each chosen based on the volume, distance, and material characteristics. The system's design also incorporates features to prevent material degradation, such as agglomeration or caking, by maintaining optimal temperature and humidity conditions. Additionally, the integration of control mechanisms allows for precise regulation of the conveying rate, ensuring consistent material flow and minimizing downtime.
Key Working Scene Characteristics of Oat Powder Conveying Systems
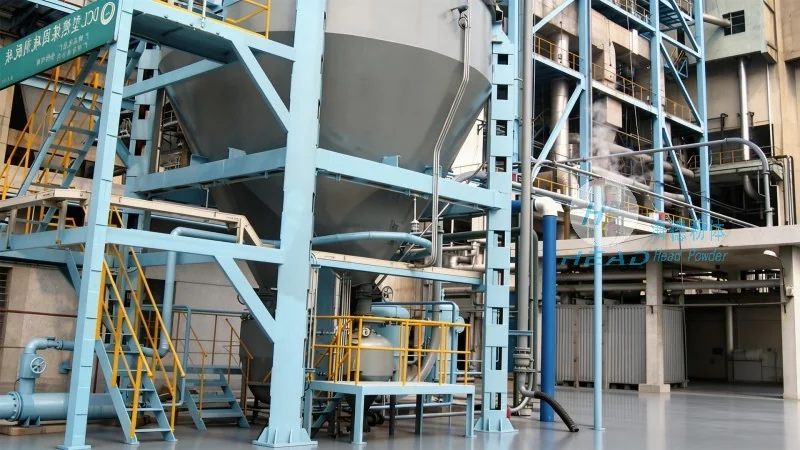
Oat powder conveying systems are widely applied in diverse industrial scenarios, each with distinct requirements that influence system configuration. In food processing facilities, for instance, these systems are crucial for transferring oat powders from storage silos to production lines, where they are used as ingredients in cereal products, baked goods, or nutritional supplements. The systems must adhere to stringent hygiene standards, often featuring stainless steel construction and easy-to-clean components to comply with food safety regulations. In agricultural and milling operations, the focus is on large-scale handling of raw oat grains, which are processed into powders for animal feed or further processing. Here, the systems are designed to handle higher capacities and may incorporate bulk handling equipment like belt conveyors or pneumatic transport lines. Furthermore, in research and development laboratories, specialized conveying systems are used for testing and analyzing oat powders, requiring precise control over material flow and particle size analysis. The adaptability of these systems to different operational environments underscores their versatility in various industrial applications.
About HeadPowder Engineering
HeadPowder Engineering, with its headquarters in Shandong, China, is a reputable company dedicated to advancing powder handling solutions. The company's expertise lies in customizing conveying systems to meet the specific needs of clients, ensuring optimal performance and reliability. With a focus on innovation and quality, HeadPowder provides comprehensive services, including system design, installation, and maintenance, tailored to the unique requirements of each project. The company's commitment to excellence has earned it a strong reputation in the industry, serving clients across various sectors that rely on efficient bulk material handling.




