Efficient and reliable powder conveying systems are essential for industries dealing with coal and coke, ensuring smooth material transport from production to processing stages. The systems designed by Shandong HeadPowder Engineering Co., Ltd. (commonly known as headpowder) leverage advanced technology to address the unique challenges of handling these bulk materials, which are often abrasive, variable in size, and prone to dust generation. These systems play a critical role in maintaining production efficiency, reducing downtime, and enhancing safety in industrial operations.
Understanding the Core Principles of Coal and Coke Powder Conveying Systems
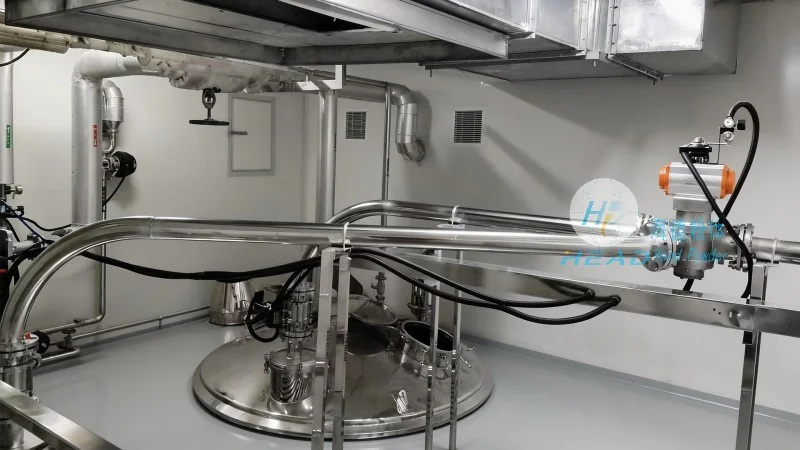
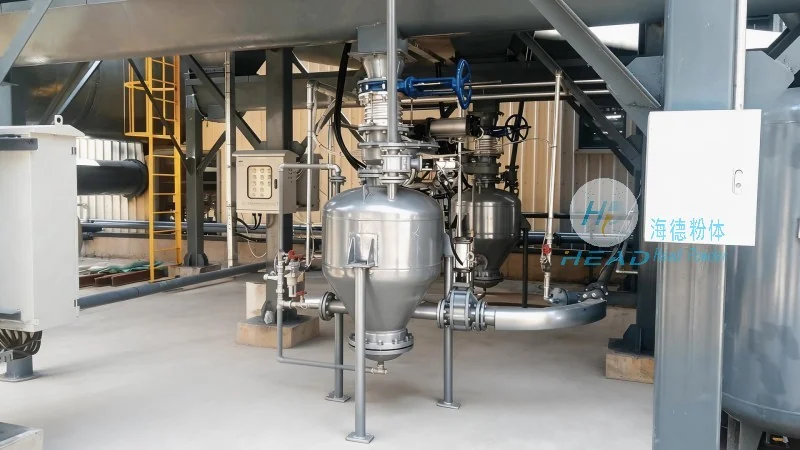
At the heart of coal and coke powder conveying systems lies a sophisticated integration of mechanical components and control mechanisms. These systems are engineered to handle the diverse properties of coal and coke powders, which can range from fine particles (e.g., coal dust) to larger coke fragments. The primary goal is to maintain consistent flow rates, minimize material degradation (such as clumping or agglomeration), and ensure safe operation in industrial settings. Key components typically include feeders (e.g., rotary feeders, vibratory feeders) that control the initial material flow, conveyors (such as screw conveyors, pneumatic (air) conveyors, or bucket elevators) that transport the material over horizontal or vertical distances, and control systems that regulate pressure, flow, and temperature. The design of these systems is tailored to the specific characteristics of the material, such as particle size distribution, moisture content, and bulk density, to optimize performance and longevity. For example, screw conveyors are effective for handling dry, free-flowing powders, while pneumatic conveyors are suitable for fine, dusty materials that require dust suppression and containment. The integration of sensors and automation further enhances system efficiency, allowing real-time monitoring and adjustment to maintain optimal operation.
Key Working Scene Characteristics and Applications
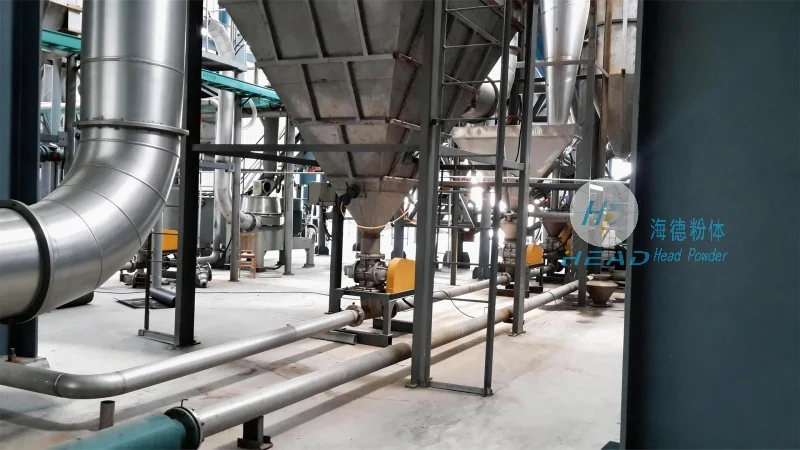
The working scene characteristics of coal and coke powder conveying systems vary significantly based on the industrial environment and operational requirements. In power plants, these systems are crucial for transporting coal from storage silos to boilers, where precise control over flow and moisture is critical to maintain combustion efficiency and reduce emissions. The systems must handle large volumes of coal while minimizing dust generation to comply with environmental regulations. In steel mills, the systems handle coke fines and dust, which are byproducts of coke production. These materials are often abrasive and can cause wear on equipment, requiring robust construction materials (such as stainless steel or wear-resistant alloys) and regular maintenance to ensure continuous operation under high-temperature conditions. Additionally, in mining and processing facilities, the systems may operate in harsh, dust-prone environments, necessitating dust suppression measures (such as cyclone separators or baghouse filters) and durable construction to withstand the rigors of continuous use. The versatility of headpowder's solutions allows them to adapt to diverse working scenarios, from small-scale operations in rural mining sites to large-scale industrial plants in urban areas, ensuring reliability and efficiency across various applications. For instance, in a coal-fired power plant, the system might involve a combination of screw conveyors for horizontal transport and bucket elevators for vertical lifting, while in a steel mill, a pneumatic conveyor system may be used to transport coke dust from processing equipment to storage silos.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
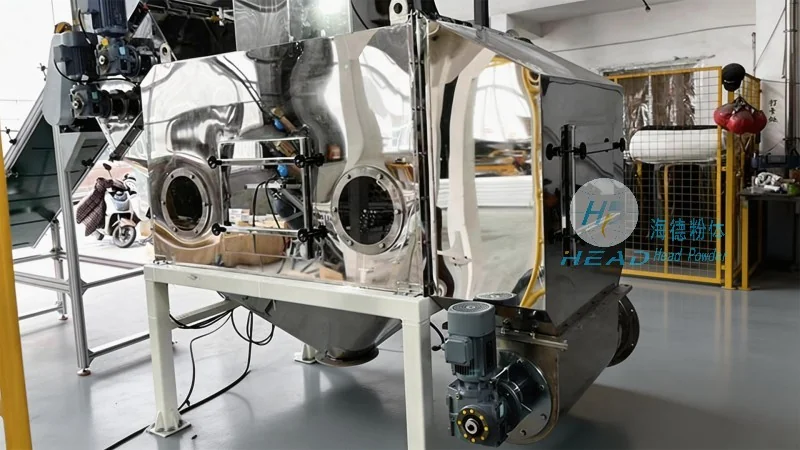
As a leading provider of specialized engineering solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of coal and coke powder conveying systems. With a strong focus on innovation and customer-centric approaches, the company has established itself as a trusted partner in the industry, serving clients across various sectors including power generation, steel manufacturing, and mining. Headpowder's team of experienced engineers and technicians leverages cutting-edge technology and rigorous testing protocols to develop systems that meet the highest standards of performance, safety, and durability. The company's headquarters is located in Shandong, China, where it maintains state-of-the-art facilities for research, development, and production. These facilities are equipped with advanced equipment for material testing, system simulation, and prototype development, enabling headpowder to deliver tailored solutions that address the unique needs of each client. By combining technical expertise with practical experience, headpowder delivers systems that not only meet current operational requirements but also adapt to future technological advancements. The company's commitment to quality and customer satisfaction has earned it a reputation for reliability and excellence in the market. Headpowder's solutions are designed to be scalable, allowing clients to upgrade or expand their systems as their operations grow, ensuring long-term investment returns and operational success.




