HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling silica powder and similar fine materials. This article delves into the fundamental principles behind these systems and highlights key working scene characteristics that make them indispensable in industrial applications.
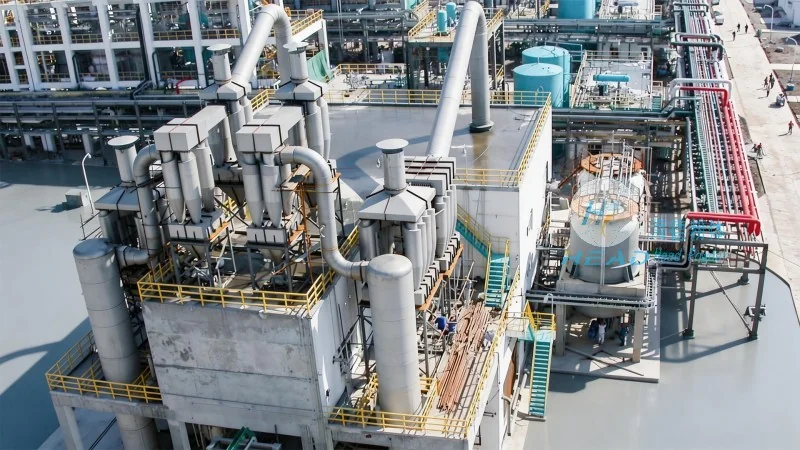
Understanding the Core Principle of Pneumatic Conveying for Silica Powder
The pneumatic conveying equipment for silica powder operates on the principle of transporting dry bulk materials through a pipeline using compressed air or other gas as the conveying medium. Unlike traditional mechanical conveying methods, this system eliminates the need for moving parts like belts or screws, reducing maintenance requirements and enhancing operational reliability. The process typically involves creating a pressure differential within the pipeline, where the gas flow propels the powder particles forward. For silica powder, which is often fine and abrasive, specialized equipment is essential to prevent material degradation and ensure efficient transport.
Key Working Scene Characteristics of Silica Powder Pneumatic Conveying Systems
One of the primary advantages of pneumatic conveying systems for silica powder is their ability to handle materials in a closed environment, minimizing dust emissions and ensuring compliance with environmental regulations. This feature is particularly critical in industries where air quality and worker safety are paramount. Additionally, these systems offer high flexibility in terms of layout, allowing for vertical, horizontal, or mixed-direction transport configurations. This adaptability makes them suitable for various industrial settings, from small-scale laboratory applications to large-scale production lines.
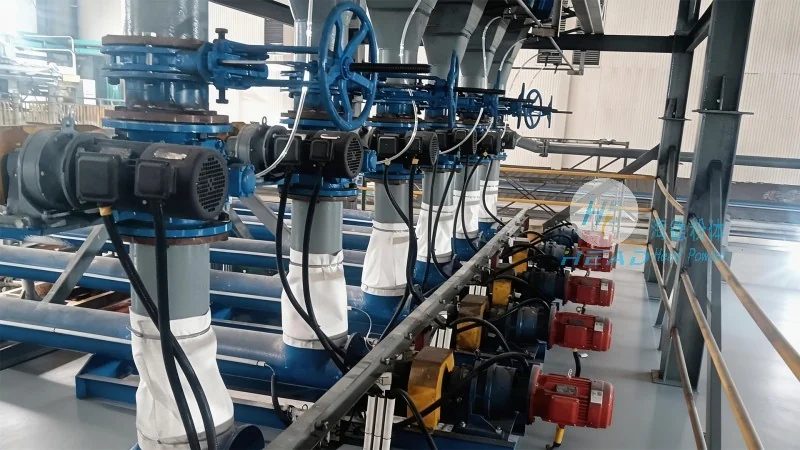
Applications and Operational Efficiency in Diverse Industrial Environments
Silica powder pneumatic conveying systems are widely utilized across multiple sectors, including pharmaceuticals, food processing, and chemical manufacturing. In pharmaceutical applications, the closed system ensures product purity and prevents contamination, which is crucial for meeting stringent regulatory standards. In food processing, the hygienic design of these systems maintains the quality of food-grade silica powders, ensuring they remain free from microbial or chemical contaminants. The operational efficiency of these systems is further enhanced by their ability to handle high volumes of material with minimal downtime, contributing to overall productivity gains in industrial operations.
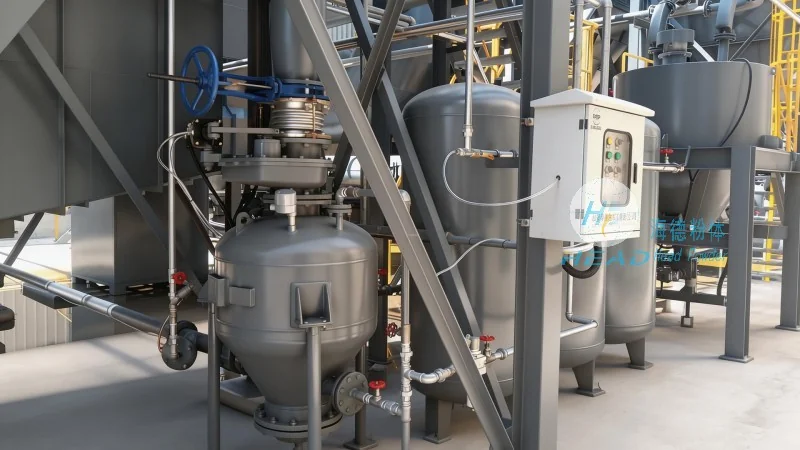
Advantages Over Traditional Conveying Methods for Silica Powder
Compared to mechanical conveying methods such as screw conveyors or bucket elevators, pneumatic conveying systems offer several distinct advantages for silica powder. Firstly, they provide a more hygienic and dust-free environment, which is essential for materials that require strict quality control. Secondly, the absence of moving parts reduces the risk of material abrasion and wear, extending the lifespan of the equipment. Thirdly, the flexibility in system design allows for seamless integration with existing production lines, minimizing installation and operational costs. These benefits collectively make pneumatic conveying the preferred choice for many industries dealing with silica powder and other fine powders.
Conclusion: The Role of HeadPowder in Advancing Silica Powder Conveying Technology
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, continues to innovate in the field of pneumatic conveying technology, providing customized solutions that meet the unique demands of silica powder handling. By leveraging advanced engineering and material science, the company ensures that its systems deliver optimal performance, reliability, and efficiency. As industries increasingly prioritize sustainability and operational excellence, the role of advanced pneumatic conveying systems for silica powder will only grow, solidifying their position as a cornerstone of modern material handling solutions.




