Positive pressure dense phase powder conveying is a critical technology in the field of bulk material handling, designed to transport powders and granular materials efficiently and reliably. This method is particularly effective for materials that are prone to dust, have low flowability, or require precise control over the conveying process. The technology operates by creating a positive pressure environment within the conveying line, which ensures that the material is moved in a dense phase, minimizing the risk of segregation and ensuring consistent flow rates.
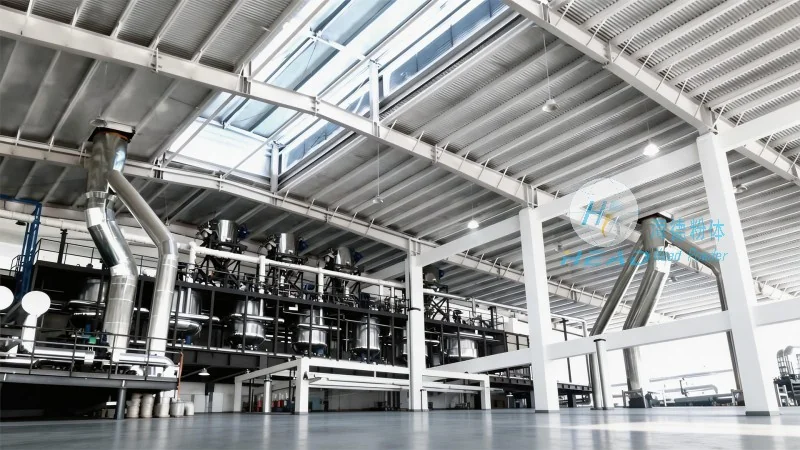
Overview of Positive Pressure Dense Phase Powder Conveying
At its core, positive pressure dense phase powder conveying involves the use of a positive pressure system to transport materials through a pipeline. Unlike negative pressure or pneumatic conveying systems, this method uses compressed air or other gases to push the material forward, resulting in a more stable and controlled conveying process. The dense phase operation means that the material is conveyed in a semi-solid state, which reduces the risk of particle separation and improves the overall efficiency of the system.
The Operation Process of Positive Pressure Dense Phase Powder Conveying
The operation process of positive pressure dense phase powder conveying typically involves several key steps. First, the material is fed into the conveying line from a hopper or storage silo. The feeder, often a screw or rotary valve, controls the flow rate of the material into the line. Next, compressed air is introduced into the system, creating a positive pressure environment. The air and material mixture is then propelled through the pipeline to the destination point, such as a silo, storage tank, or processing unit. The system is designed to maintain a consistent pressure and flow rate, ensuring that the material is conveyed smoothly without blockages or air leaks.
Working Principle of Positive Pressure Dense Phase Powder Conveying
The working principle of positive pressure dense phase powder conveying is based on the principles of fluid dynamics and material flow. The system uses compressed air to create a pressure differential between the inlet and outlet of the conveying line. This pressure differential drives the material forward, while the dense phase operation ensures that the material remains in contact with the pipeline walls, reducing the risk of particle segregation and improving the conveying efficiency. The system is equipped with pressure sensors and control valves to maintain the optimal pressure and flow rate, ensuring that the conveying process is efficient and reliable.
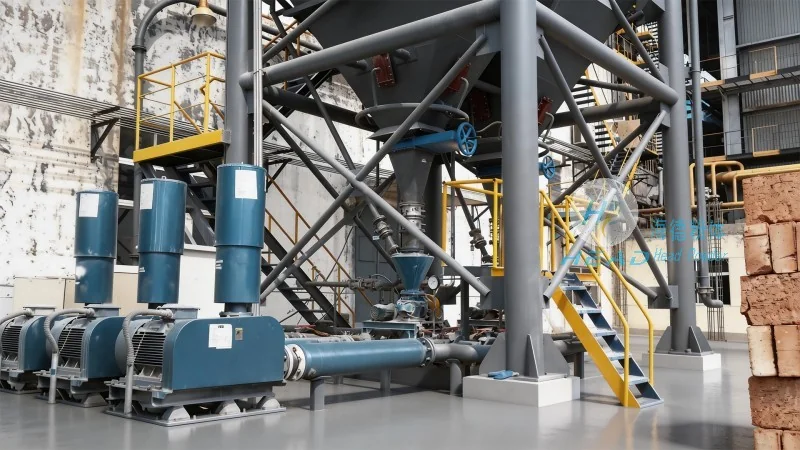
Key Components and Their Functions
Several key components are essential for the proper operation of a positive pressure dense phase powder conveying system. These include the material feeder, which controls the flow rate of the material; the compressor, which provides the compressed air; the conveying line, which transports the material; and the control system, which monitors and adjusts the pressure and flow rate. Each component plays a critical role in ensuring the efficient and reliable operation of the system. For example, the feeder ensures that the material is fed at a consistent rate, while the compressor maintains the required pressure. The control system ensures that the system operates within the optimal parameters, preventing overpressure or underpressure conditions that could lead to system failure.
Advantages of Positive Pressure Dense Phase Powder Conveying
Positive pressure dense phase powder conveying offers several advantages over other conveying methods. One of the main advantages is its ability to handle a wide range of materials, including those that are difficult to convey, such as powders with low flowability or high dust content. The dense phase operation also reduces the risk of particle segregation, which can affect the quality of the material being conveyed. Additionally, the system is more energy-efficient than other methods, as it uses less air and requires less maintenance. The positive pressure environment also helps to prevent the ingress of contaminants into the system, ensuring that the material remains clean and free from contamination.
Applications of Positive Pressure Dense Phase Powder Conveying
Positive pressure dense phase powder conveying is used in a variety of industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, it is used to transport powders such as flour, sugar, and cocoa. In the pharmaceutical industry, it is used to transport powders such as active pharmaceutical ingredients (APIs) and excipients. In the chemical industry, it is used to transport powders such as pigments, fillers, and catalysts. In the mining industry, it is used to transport powders such as coal, ore, and minerals. The technology is also used in the production of cement, where it is used to transport raw materials such as limestone and clay.
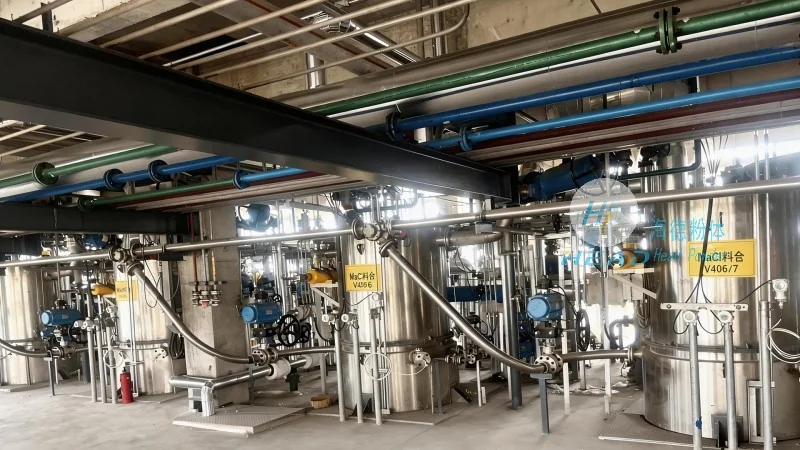
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of positive pressure dense phase powder conveying systems. The company is headquartered in Shandong, China, and has a strong reputation for providing high-quality, reliable, and efficient conveying solutions to its customers. HeadPowder specializes in the design, manufacturing, and installation of positive pressure dense phase powder conveying systems, tailored to the specific needs of each customer. The company's products are known for their durability, efficiency, and ease of maintenance, making them a popular choice among industries that require reliable material handling solutions.
Technical Expertise and Innovation
HeadPowder has a team of experienced engineers and technicians who are dedicated to developing and improving positive pressure dense phase powder conveying technology. The company invests heavily in research and development, ensuring that its products are at the forefront of the industry. HeadPowder's engineers work closely with customers to understand their specific conveying needs and develop customized solutions that meet their requirements. The company also provides comprehensive technical support and training to its customers, ensuring that they can operate and maintain their conveying systems effectively.
Quality Assurance and Compliance
HeadPowder is committed to providing high-quality products and services to its customers. The company has implemented a comprehensive quality management system that ensures that all products meet or exceed industry standards. HeadPowder's products are tested and certified to meet various international standards, including ISO 9001 and CE. The company also adheres to strict environmental and safety regulations, ensuring that its products are environmentally friendly and safe to use.




