Ammonium nitrate is a widely used chemical compound in industries such as agriculture, explosives, and chemical manufacturing. When dealing with ammonium nitrate powders that contain moisture, efficient and safe conveying systems are essential to ensure smooth production processes and minimize operational risks. This article provides a detailed overview of the operation process and working principle of a specialized conveying system designed for handling moist ammonium nitrate powders, highlighting key components, operational steps, and technical advantages.
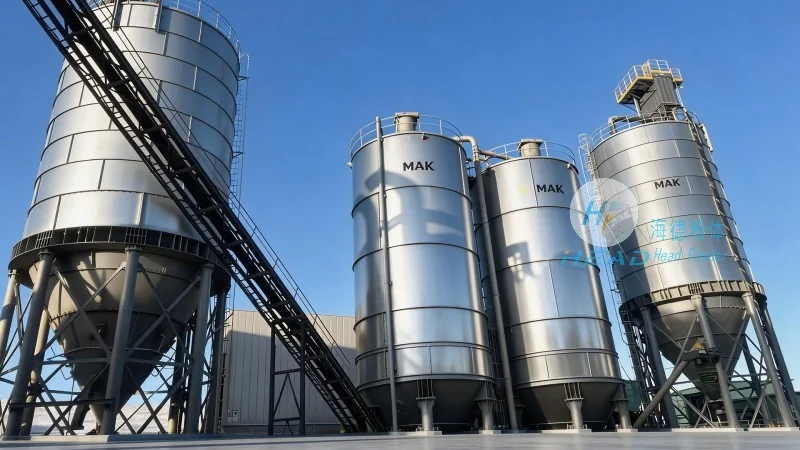
System Overview and Core Components
The ammonium nitrate powder conveying system with moisture is engineered to handle powders that have a certain level of moisture content, which can affect flowability and handling characteristics. The system typically consists of several critical components working in tandem to achieve reliable material transport. These components include a hopper for material storage, a rotary valve or feeder to control the flow rate, a flexible or rigid conveying pipe system, a drive unit (such as a motor and gearbox), and a control panel for monitoring and adjusting operational parameters. Each component plays a vital role in maintaining the system's efficiency and safety during operation.
System Structure and Design Considerations
The design of the conveying system is tailored to address the unique challenges posed by moist ammonium nitrate powders. Moisture in the powder can lead to caking or blockages in traditional conveying systems, so the design incorporates features like anti-caking mechanisms and self-cleaning elements. The hopper is often equipped with heating elements or insulation to prevent moisture condensation and maintain the material's properties. The conveying pipes may be made of corrosion-resistant materials like stainless steel or special plastics to withstand the chemical properties of ammonium nitrate. Additionally, the system includes safety features such as pressure relief valves and emergency stop buttons to protect operators and equipment from potential hazards.
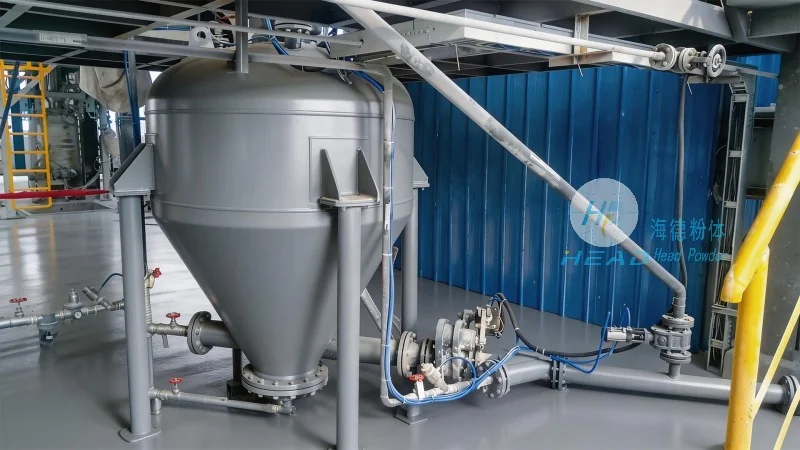
Operation Process: Step-by-Step Execution
The operation of the ammonium nitrate powder conveying system with moisture follows a systematic sequence to ensure consistent and safe material handling. The process begins with the loading of moist ammonium nitrate into the hopper. The hopper is designed to accommodate the bulk material and maintain a stable feed. Once the material is loaded, the rotary valve or feeder is activated to regulate the flow rate. The controlled flow then enters the conveying pipe, where the material is propelled forward by the drive unit. The drive unit, typically a motor-driven screw or positive displacement pump, provides the necessary force to move the powder through the system. The control panel allows operators to adjust the speed and flow rate based on real-time conditions, ensuring optimal performance. The material exits the system through a discharge valve or outlet, where it is collected for further processing or storage.
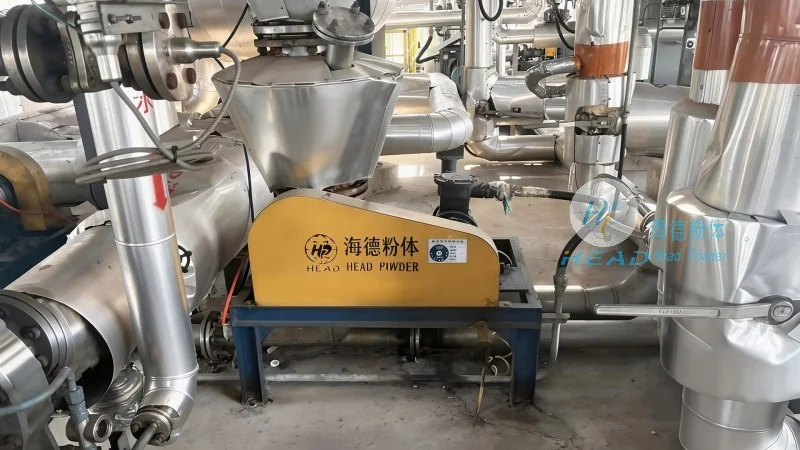
Working Principle: Mechanics and Physics
The working principle of the conveying system is based on the principles of fluid dynamics and mechanical force application. For moist ammonium nitrate powders, the system utilizes a combination of gravity and mechanical force to move the material. The hopper and feeder work together to create a consistent flow, while the drive unit provides the necessary pressure or force to overcome resistance in the conveying pipe. The flexible or rigid pipes are designed to minimize friction and maintain the material's integrity. The system's control mechanisms ensure that the flow rate and pressure are maintained within safe and efficient parameters. This integrated approach allows for continuous and reliable operation, even with varying moisture content in the powder.
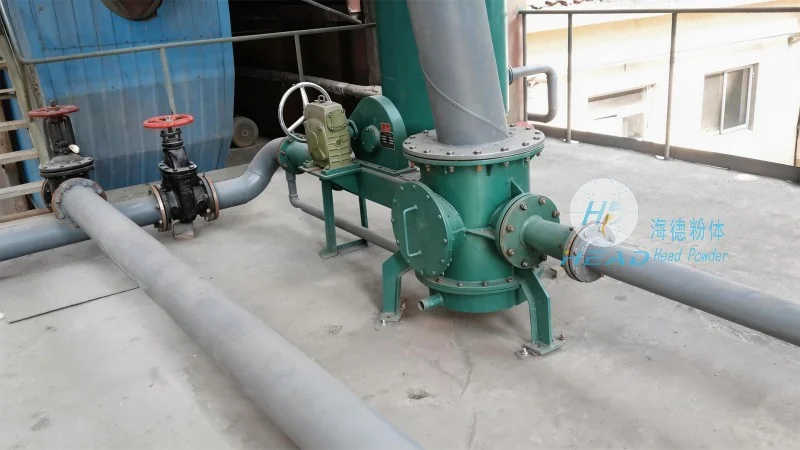
Technical Advantages and Application Value
The ammonium nitrate powder conveying system with moisture offers several technical advantages that enhance operational efficiency and safety. One key advantage is its ability to handle powders with moisture content, which is often a challenge for traditional conveying systems. The system's anti-caking and self-cleaning features reduce downtime and maintenance costs. The corrosion-resistant materials used in the construction ensure long-term durability and resistance to chemical degradation. Additionally, the system's control panel provides real-time monitoring and adjustment capabilities, allowing operators to optimize performance and respond to changes in material conditions quickly. These advantages make the system suitable for various applications, including fertilizer production, chemical processing, and industrial material handling, where reliable and safe powder transport is critical.
Company Information: HeadPowder Engineering
HeadPowder Engineering, also known as Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier of specialized powder handling equipment. The company is headquartered in Shandong, China, and has extensive experience in designing and manufacturing conveying systems for various industrial applications. HeadPowder Engineering focuses on providing high-quality, reliable solutions tailored to the specific needs of its clients, ensuring that their equipment meets the highest standards of performance, safety, and efficiency. The company's commitment to innovation and customer satisfaction has made it a trusted partner in the powder handling industry.




