For industrial applications requiring precise and contamination-free powder transport, the dust-free powder handling system from Shandong HeadPowder Engineering Co., Ltd. offers a reliable solution. This equipment is designed to maintain a clean environment while efficiently moving powders, ensuring product integrity and operational safety. The following sections detail the operational process and underlying working principles of this advanced system.
Company Overview and Product Introduction
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and supply of high-quality powder handling equipment. Based in Shandong, China, the company leverages years of industry experience to develop systems that meet stringent standards for dust control and material transport. The dust-free powder transport system is a core product line, engineered to address the challenges of handling powders in environments where contamination and particle loss are critical concerns. This system integrates advanced technology to ensure efficient, safe, and clean operation, making it suitable for various industrial sectors such as pharmaceuticals, food processing, and chemical manufacturing.
System Components and Their Roles
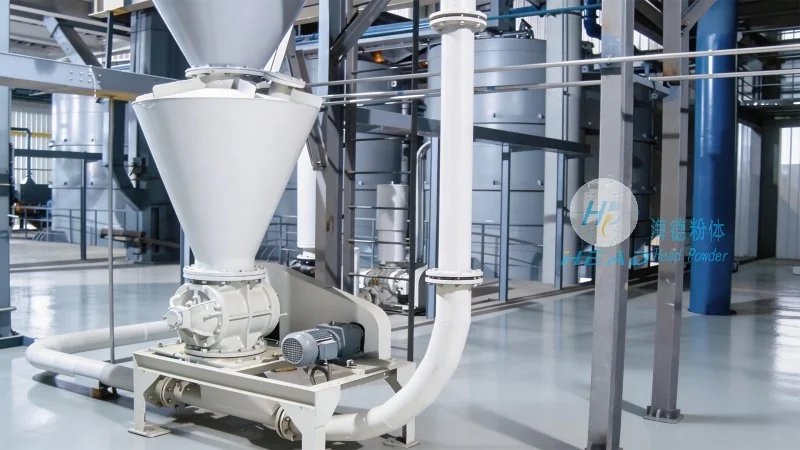
The dust-free powder handling system comprises several key components, each playing a vital role in the overall operation. The primary elements include a hopper for material storage, a rotary valve or feeder for controlled discharge, a conveyor system (often pneumatic or mechanical) for transport, and a dust collection unit to maintain air quality. The hopper is typically equipped with a lid and sealing mechanisms to prevent dust leakage. The feeder regulates the flow of powder from the hopper to the conveyor, ensuring a consistent and controlled rate. The conveyor transports the powder to the destination, while the dust collection system captures any airborne particles, preventing environmental contamination and maintaining a safe working environment. Each component is designed with precision to work in harmony, contributing to the system's overall efficiency and reliability.
Operation Process: Step-by-Step Execution
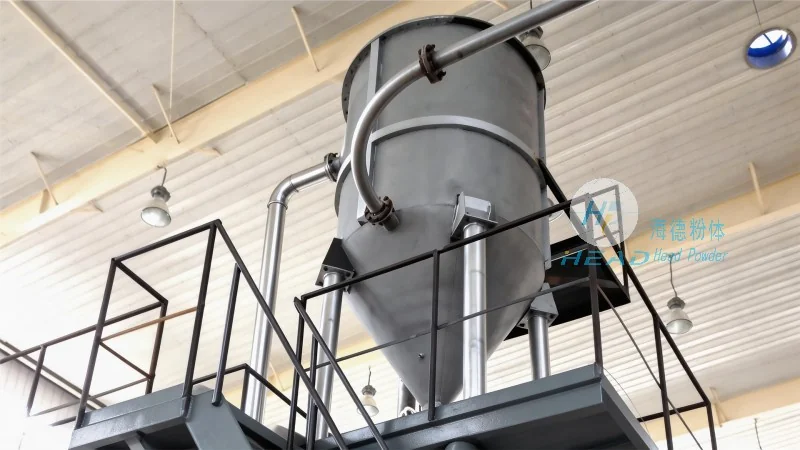
The operation of the dust-free powder handling system follows a systematic process, starting with material loading and ending with delivery. The steps are as follows: First, the powder is loaded into the hopper, which is sealed to prevent dust from escaping. Second, the feeder is activated to control the flow of powder from the hopper. Third, the conveyor system is engaged, transporting the powder to the target location. Fourth, the dust collection unit operates continuously to capture any particles that may be released during the process. Fifth, the system monitors key parameters such as flow rate and pressure to ensure optimal performance. Finally, the powder is delivered to the processing unit or storage area. This step-by-step process ensures that the system operates smoothly and efficiently, minimizing downtime and maximizing productivity.
Working Principle: How the System Maintains Dust-Free Conditions
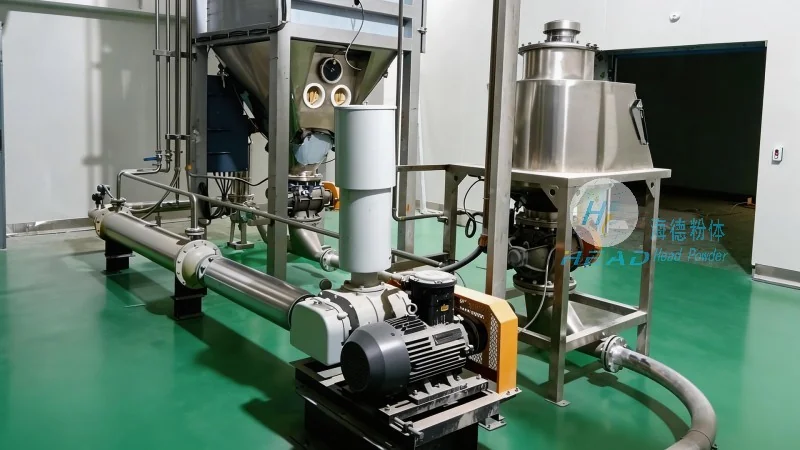
The working principle of the dust-free powder handling system is centered on creating a sealed environment and controlling airflow to prevent dust contamination. The system operates on the principle of negative pressure or sealed transport, where the conveyor and associated components are enclosed to contain the powder. The feeder and hopper are designed with tight seals to prevent dust from escaping into the surrounding environment. The dust collection unit uses filters or cyclones to capture any particles that may be released, ensuring that the air is clean before it is released back into the facility. Additionally, the system may incorporate air filtration and recirculation to maintain a consistent air quality. By maintaining a sealed and controlled environment, the system effectively prevents dust from contaminating the product or the workplace, ensuring compliance with industry standards and regulations. The working principle also emphasizes energy efficiency and minimal particle loss, making it a cost-effective solution for long-term operation.
Key Advantages and Industrial Applications
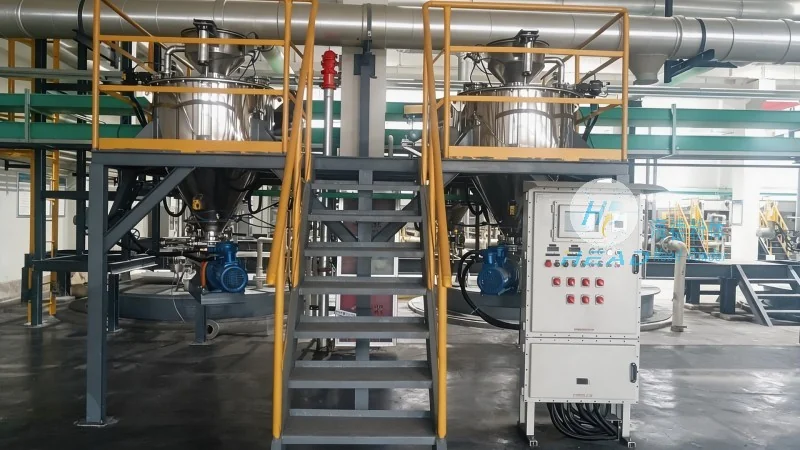
The dust-free powder handling system offers several advantages that make it a preferred choice for industries requiring precise powder transport. These advantages include high efficiency in material handling, minimal product contamination, and compliance with stringent environmental regulations. The system is designed to handle a wide range of powders, from fine to coarse, and can be customized to meet specific operational requirements. Industrial applications of this system include pharmaceutical manufacturing, where product purity is paramount, food processing, where hygiene is critical, and chemical production, where dust control is essential for safety and quality. The system's ability to maintain a clean environment and ensure product integrity makes it an indispensable tool in these industries, contributing to higher quality output and reduced operational risks.
Conclusion: Reliability and Performance of the Dust-Free Powder Handling System
In conclusion, the dust-free powder handling system from Shandong HeadPowder Engineering Co., Ltd. is a sophisticated and reliable solution for industrial powder transport. By integrating advanced components and a systematic operational process, the system ensures efficient, safe, and clean operation. The working principle of maintaining a sealed environment and controlling airflow is fundamental to its success, preventing dust contamination and ensuring product integrity. With its robust design and customization options, the system is suitable for various industrial applications, meeting the demands of modern manufacturing. As a leader in powder handling technology, headpowder continues to innovate and provide high-quality solutions that enhance operational efficiency and safety in the industry.




