For industrial applications requiring precise and efficient handling of powders, the small bag quantitative weighing powder conveying system equipment from Shandong HeadPowder Engineering Co., Ltd. offers a reliable solution. This system is designed to handle the entire process from receiving bulk powders in small bags to accurately weighing and transferring them to the next stage of production. The equipment is engineered to ensure high accuracy in measurement and seamless operation, making it an essential component in various manufacturing and processing industries.
System Overview and Core Components
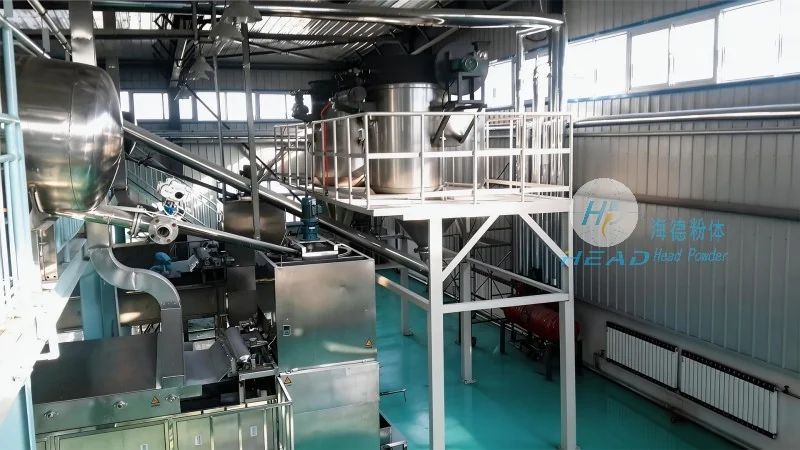
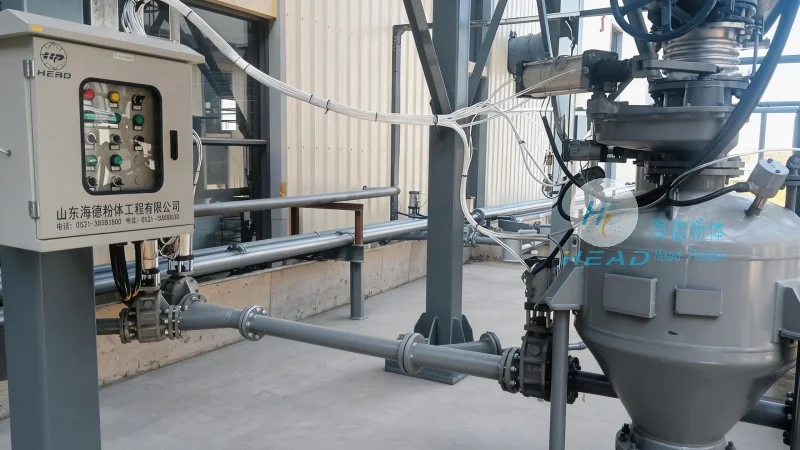
The small bag quantitative weighing powder conveying system typically consists of several key components that work in tandem to achieve precise material handling. These include the bag opening mechanism, the weighing scale, the conveyor system, and the control unit. The bag opening mechanism is responsible for safely and efficiently opening the small bags, allowing the powder to be released into the weighing hopper. The weighing scale, often a high-precision load cell system, measures the weight of the powder as it is transferred, ensuring that the correct quantity is obtained. The conveyor system then transports the weighed powder to the storage or processing area, while the control unit manages the entire process, including bag opening, weighing, and conveyor operation. Each component is carefully selected and integrated to provide a robust and accurate system suitable for demanding industrial environments.
Operation Process: Step-by-Step Workflow
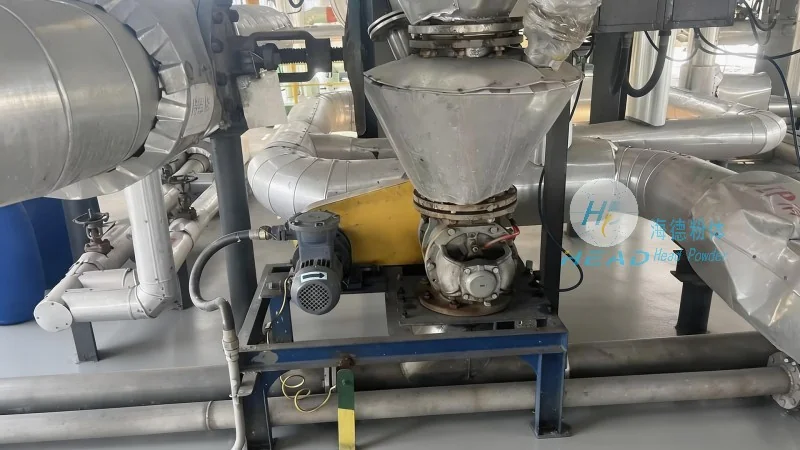
The operation of the small bag quantitative weighing powder conveying system follows a systematic workflow that ensures consistent and accurate results. The process begins with the placement of a small bag of powder onto the bag opening platform. The system then automatically opens the bag, allowing the powder to flow into the weighing hopper. As the powder is added, the load cell measures the weight in real-time, and the control unit monitors the weight against the set target. Once the desired weight is reached, the system stops the flow of powder and signals the next step. The weighed powder is then transferred to the conveyor, which moves it to the storage silo or directly to the processing equipment. The system can handle multiple bags sequentially, maintaining a continuous and efficient operation. This step-by-step process minimizes human intervention, reduces errors, and enhances overall productivity in powder handling operations.
Working Principle: How Precision is Achieved
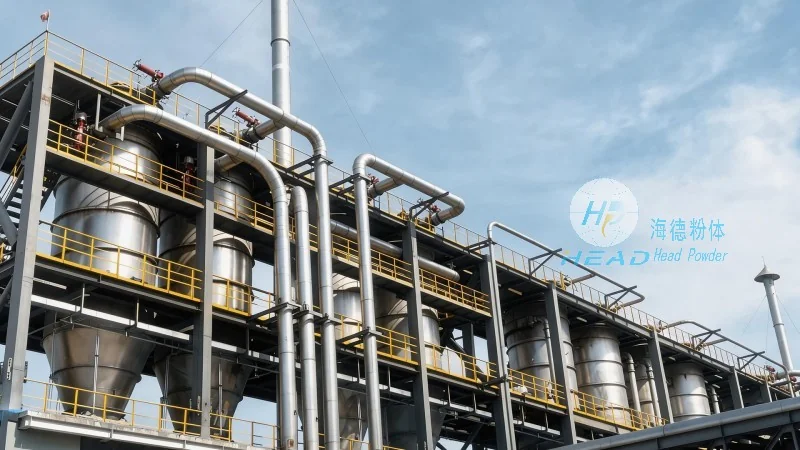
The working principle of the small bag quantitative weighing powder conveying system is based on the integration of mechanical, electrical, and software components to achieve high-precision measurement and control. The core of the system is the load cell, which converts the weight of the powder into an electrical signal. This signal is transmitted to the control unit, which processes the data and compares it with the preset weight. The control unit then adjusts the flow of powder through the bag opening and conveyor system to maintain the desired weight. The system uses advanced algorithms to compensate for variations in powder density, bag size, and other factors that could affect the accuracy of the measurement. Additionally, the system incorporates features such as automatic bag detection, weight verification, and error correction to ensure that each batch of powder is handled with precision. This combination of hardware and software ensures that the system delivers consistent results, even with different types of powders and varying operating conditions.




