Ammonium sulfate is a widely used chemical fertilizer and industrial raw material, and the efficient handling of its powder form is crucial for industrial production. The powder conveying system equipment designed by Shandong HeadPowder Engineering Co., Ltd. (headpowder) plays a vital role in ensuring smooth material flow and stable production operations. This article will delve into the operation process and working principle of this system, providing a comprehensive understanding of its functionality and technical advantages.
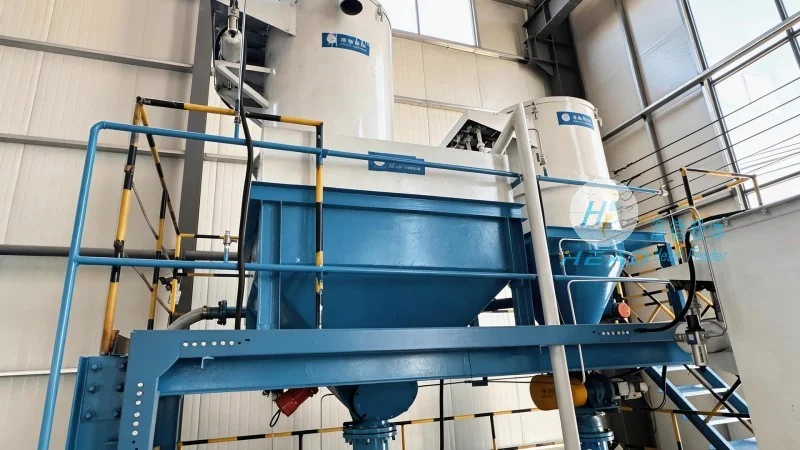
System Overview and Core Components
The ammonium sulfate powder conveying system typically consists of several key components, including a hopper for material storage, a feeder to control the flow rate, a conveyor (such as a screw conveyor or pneumatic conveyor), a dust collection system, and a control panel for automated operation. Each component is carefully designed to work in harmony, ensuring the safe and efficient transport of the powder. The system is built with durability in mind, using high-quality materials that can withstand the corrosive and abrasive nature of ammonium sulfate.
Working Principle of the Conveying Process
The core working principle of the system is based on the principles of fluidization and mechanical transport. When the material is fed into the hopper, the feeder regulates the flow rate, ensuring a consistent supply to the conveyor. For mechanical conveyors, the screw or belt mechanism moves the powder forward through the system. In pneumatic conveying systems, compressed air is used to create a flow that carries the powder particles through the pipeline. The dust collection system is integrated to capture any airborne particles, maintaining a clean and safe working environment. The control panel allows operators to monitor and adjust the system parameters in real-time, optimizing performance and preventing downtime.
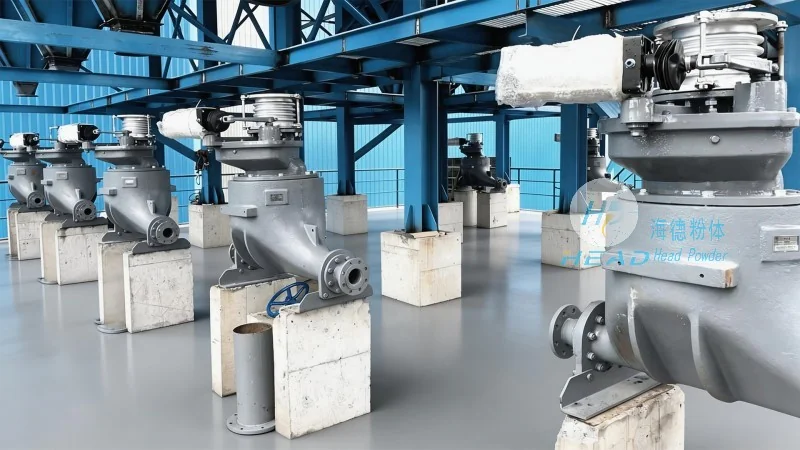
Operation Process and Key Steps
The operation process of the ammonium sulfate powder conveying system involves several sequential steps. First, the hopper is filled with ammonium sulfate powder, and the feeder is activated to start the material flow. The feeder adjusts the flow rate based on the system's requirements, ensuring that the conveyor operates at an optimal speed. The conveyor then transports the powder to the next processing stage or storage area. During operation, the dust collection system continuously filters the air, preventing dust accumulation and maintaining air quality. The control panel provides real-time data on flow rate, pressure, and other critical parameters, allowing operators to make adjustments as needed. Regular maintenance is also performed to ensure the system remains in good working condition, including cleaning of the hopper and conveyor, checking for wear and tear, and replacing any worn parts.
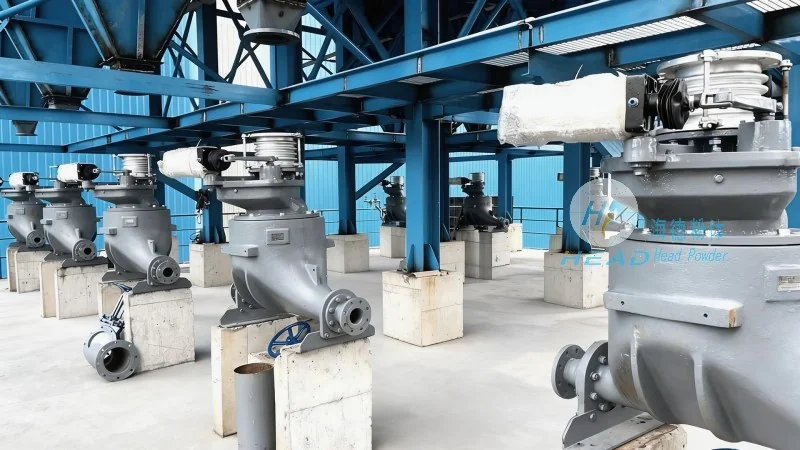
Technical Advantages and Application Benefits
Shandong HeadPowder Engineering Co., Ltd. has designed this system with several technical advantages that enhance its performance and reliability. The use of high-quality materials ensures long service life and minimal maintenance. The automated control system reduces the need for manual intervention, improving operational efficiency and reducing labor costs. The dust collection system not only maintains a clean environment but also prevents dust-related health hazards. The system's modular design allows for easy integration into existing production lines, making it a flexible solution for various industrial applications. The company's expertise in powder handling technology ensures that the system is tailored to meet the specific needs of each client, providing a customized solution that maximizes productivity and safety.
Overall, the ammonium sulfate powder conveying system equipment from headpowder is a reliable and efficient solution for industrial powder handling. By understanding the operation process and working principle, users can better appreciate the technical sophistication and practical benefits of this system. The company's commitment to quality and innovation ensures that their products meet the highest standards, making them a trusted choice in the industry.




