Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer based in Shandong, China, specializing in the design, development, and implementation of advanced bulk powder pneumatic conveying systems for grain silos. These systems are crucial for efficient material handling in agricultural and food processing industries, ensuring smooth and reliable transport of grains and other powders.
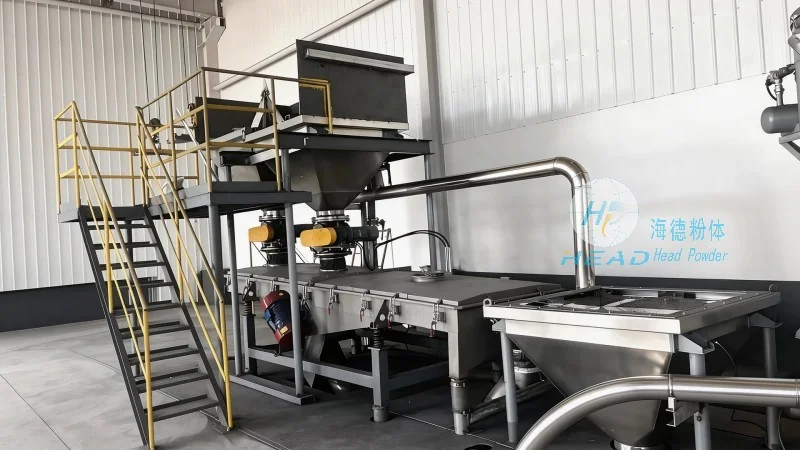
Overview of Bulk Powder Pneumatic Conveying Systems in Grain Silos
A bulk powder pneumatic conveying system in a grain silo is a sophisticated setup that utilizes compressed air or vacuum to move granular materials through a network of pipes. The system is engineered to handle various types of grains, including wheat, corn, rice, and other bulk commodities, with minimal product degradation and maximum operational efficiency. Key components typically include a hopper for material storage, a conveyor line with appropriate ductwork, a control system for regulating air flow, and a discharge point for delivering the material to the next processing stage.
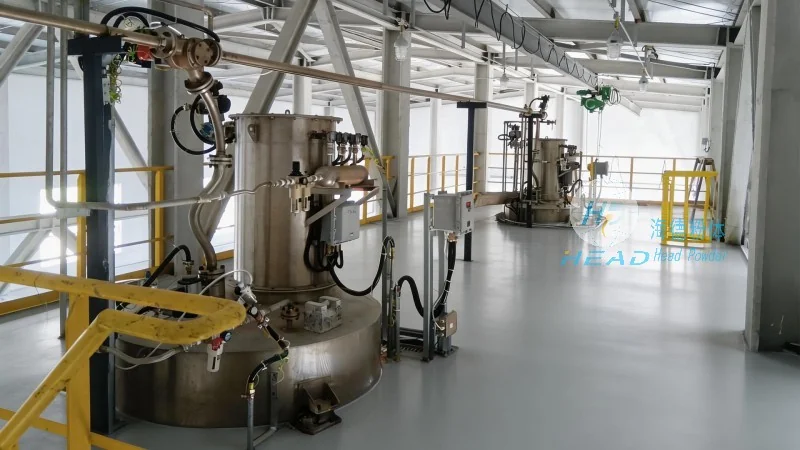
The Operation Process of the System
The operation of a grain silo bulk powder pneumatic conveying system follows a systematic sequence to ensure safe and efficient material transport. Initially, the system is prepared by checking all components, including the hopper, conveyor pipes, and air compressor or vacuum pump, for proper functionality and security. Once the system is ready, the material is fed into the hopper from the storage silo or a bulk loading area. The control system then activates the air compressor or vacuum pump, generating the necessary pressure or suction to initiate the conveying process. As the air flows through the pipes, it entrains the powder particles, forming a dense mixture known as a "pneumatic stream." This stream travels through the ductwork, transporting the material from the source to the destination point, such as a processing plant, storage bin, or packaging area. The system continues to operate until the required amount of material has been transferred, at which point the control system automatically shuts down the air flow and stops the conveyor. Finally, the system is cleaned and maintained to prepare for the next batch of material.
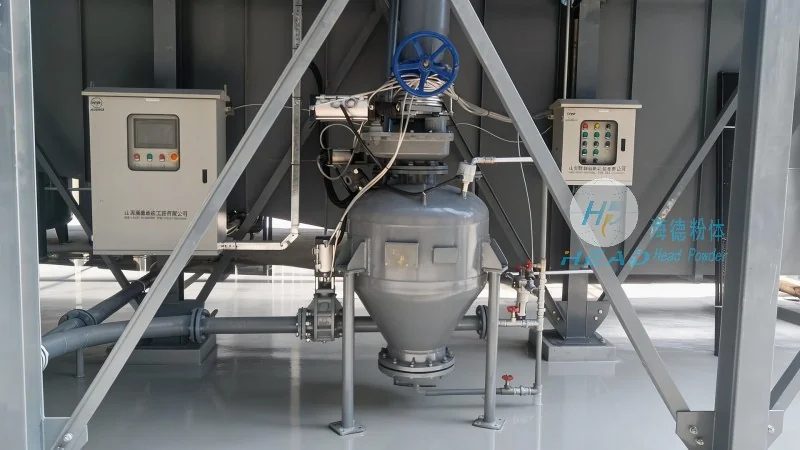
The Working Principle of the System
The core working principle of a bulk powder pneumatic conveying system in a grain silo is based on the interaction between air flow and solid particles. There are two primary methods: positive pressure (or pressure) conveying and negative pressure (or vacuum) conveying. In positive pressure conveying, a high-pressure air compressor forces air through the conveyor pipes, creating a pressure differential that pulls the powder particles along with the air stream. The air flow is directed from the discharge end towards the hopper, ensuring that the material is pushed forward. In negative pressure conveying, a vacuum pump creates a low-pressure environment at the discharge end, drawing the powder particles into the system and moving them towards the hopper. Both methods rely on the principle of fluidization, where the air flow suspends the powder particles, allowing them to be transported as a fluid-like mixture. The system's efficiency depends on factors such as the air velocity, particle size, and the design of the ductwork, all of which are optimized to minimize energy consumption and maximize material throughput.
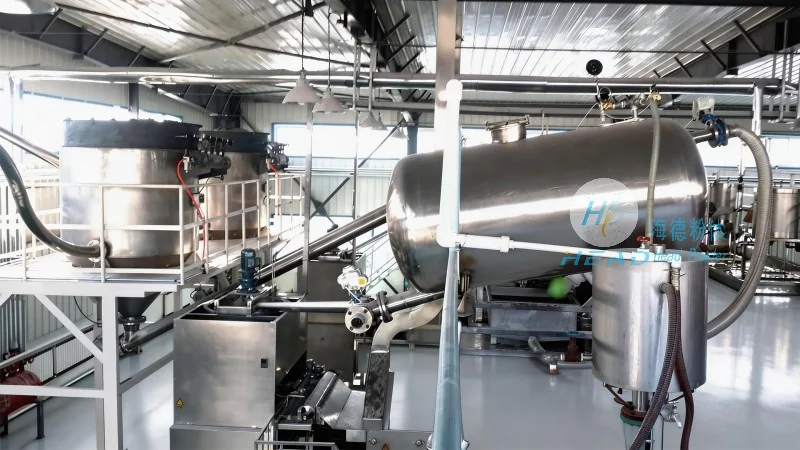
Key Technical Features and Benefits
Shandong HeadPowder Engineering Co., Ltd. designs and manufactures bulk powder pneumatic conveying systems that incorporate several advanced technical features to enhance performance and reliability. These features include adjustable air flow control to regulate the conveying rate, anti-clogging mechanisms to prevent blockages in the pipes, and temperature control systems to maintain optimal conditions for sensitive materials. The systems are also equipped with safety sensors and alarms to detect and respond to any abnormalities, such as pressure fluctuations or blockages, ensuring the safety of the operation and the integrity of the material. The benefits of these systems include reduced labor costs due to automated material handling, minimized product loss and contamination, and improved overall operational efficiency in grain silo operations. By leveraging these advanced features, the systems provide a cost-effective and reliable solution for bulk material transport in the agricultural and food processing sectors.




