This article provides an overview of small stone pneumatic conveying equipment, focusing on its structural design and operational principles. The equipment is engineered to efficiently transport small stone particles through an air-driven system, offering a reliable solution for material handling in various industrial applications. By understanding the core components and working mechanisms, users can appreciate the efficiency and versatility of this technology.
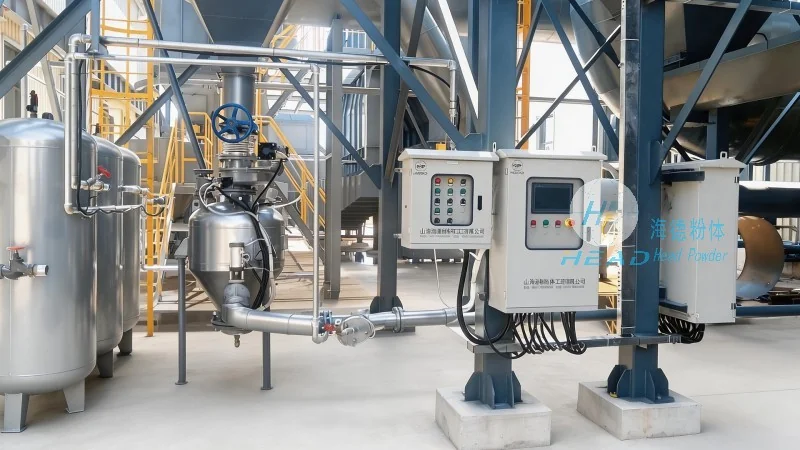
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems. With years of industry experience, the company has developed a range of equipment tailored to meet the specific needs of different sectors, including construction, mining, and manufacturing. The company's commitment to quality and innovation ensures that their products deliver optimal performance and durability.
At the heart of small stone pneumatic conveying equipment is the air compressor, which generates the necessary pressure to move the material. The system typically consists of a hopper for material storage, a feeder to control the flow rate, and a pipeline network that transports the particles. The hopper is designed with a conical or rectangular shape to facilitate smooth material discharge, while the feeder, often a rotary valve or a screw feeder, regulates the amount of material entering the pipeline. The pipeline itself is made of durable materials such as stainless steel or plastic, ensuring resistance to corrosion and wear from the small stone particles.
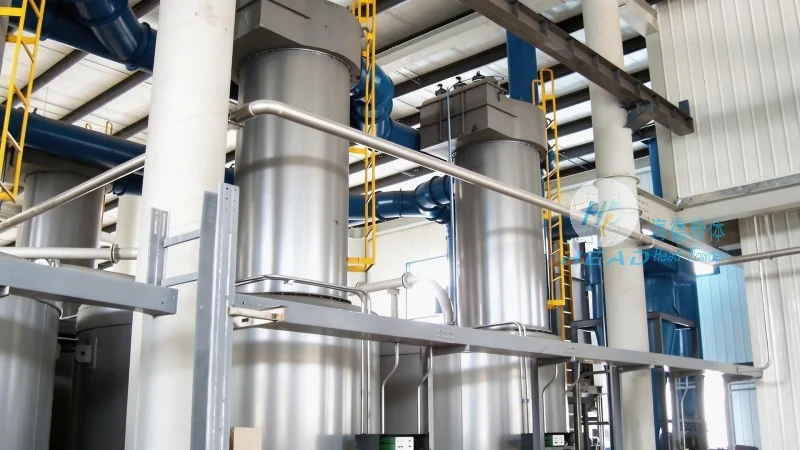
The conveying process begins when the air compressor pumps high-pressure air into the pipeline. The small stone particles are then introduced into the system, either by gravity or through the feeder. As the air flows through the pipeline, it creates a low-pressure zone that draws the particles along with it. This combination of air and material forms a dense phase or dilute phase flow, depending on the operating conditions. The dense phase flow is characterized by a higher concentration of particles, which is suitable for longer distances or when handling more abrasive materials. The dilute phase flow, on the other hand, involves a lower particle concentration, making it ideal for shorter distances or when the material is less abrasive.
Key components of the small stone pneumatic conveying system include the air compressor, which provides the driving force; the hopper, which stores the material; the feeder, which controls the material flow; the pipeline, which transports the material and air; and the receiver, which collects the material at the destination. The air compressor is usually a positive displacement type, such as a rotary screw or a piston compressor, capable of delivering the required pressure and airflow. The hopper is equipped with a discharge valve to prevent material buildup and ensure consistent feeding. The feeder is designed to maintain a steady flow rate, preventing overloading or underloading of the system. The pipeline is typically arranged in a straight or slightly curved configuration to minimize pressure losses and ensure smooth material transport. The receiver is a container that collects the material after it has been conveyed, often with a dust collection system to prevent air leakage and maintain a clean environment.
One of the primary advantages of small stone pneumatic conveying equipment is its ability to handle small, abrasive particles without causing excessive wear on the system components. The design of the hopper and feeder minimizes material impact, while the pipeline is constructed from materials that can withstand the abrasive nature of the small stones. Additionally, the system can be configured to handle different particle sizes and shapes, making it versatile for various applications. The air-driven operation also reduces the risk of mechanical failure compared to traditional belt or bucket elevators, as there are fewer moving parts that can break or wear out.
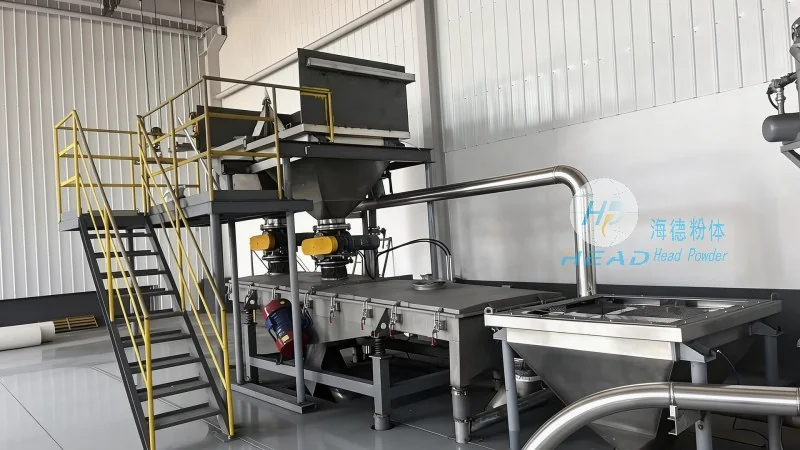
HeadPowder's small stone pneumatic conveying equipment is designed with user-friendly features that enhance operational efficiency. The control panel allows operators to adjust the air pressure, flow rate, and material feed rate, ensuring optimal performance under different conditions. The system is also equipped with safety features, such as pressure relief valves and overcurrent protection, to prevent accidents and equipment damage. Maintenance is simplified with easy access to key components, such as the air compressor and feeder, allowing for quick inspections and repairs. The company provides comprehensive technical support and training to ensure that users can operate and maintain the equipment effectively.
In conclusion, small stone pneumatic conveying equipment offers a reliable and efficient solution for transporting small stone particles in various industrial applications. The combination of advanced structural design and operational principles ensures high performance, durability, and versatility. HeadPowder, with its expertise and commitment to quality, provides top-tier equipment that meets the needs of different industries. By understanding the components and working mechanisms, users can make informed decisions about implementing this technology in their operations.




