Ammonium bicarbonate, a critical chemical in various industrial applications, requires efficient and reliable transportation systems to ensure consistent supply and process stability. The design of pneumatic conveying equipment for this material is a specialized field that combines mechanical engineering principles with material handling expertise. This document outlines the key considerations and design elements for an effective ammonium bicarbonate pneumatic conveying system, highlighting the technical solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
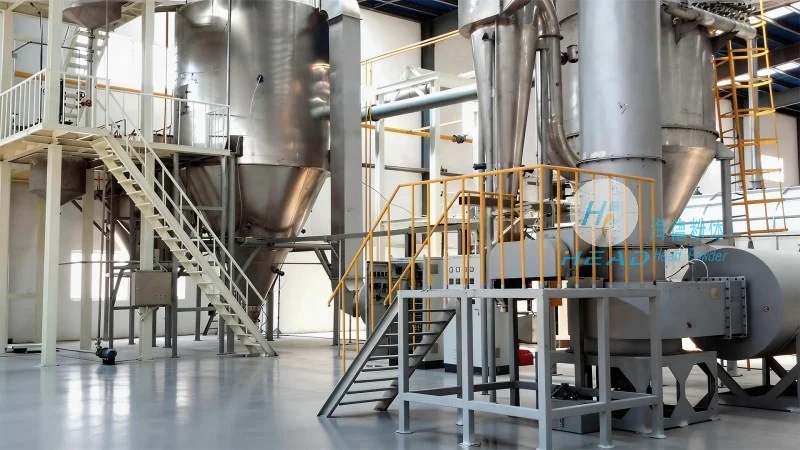
Company Overview: HeadPowder
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is a professional enterprise based in Shandong, China. With a strong focus on engineering innovation and customer-centric solutions, HeadPowder specializes in the design, manufacturing, and installation of pneumatic conveying systems for various bulk materials, including ammonium bicarbonate. The company’s commitment to quality and technical excellence has established it as a trusted partner for industries requiring high-performance material handling solutions.
Key Design Features of the Ammonium Bicarbonate Pneumatic Conveying System
The pneumatic conveying system for ammonium bicarbonate is engineered to address the unique properties of this material, such as its hygroscopic nature and potential for dust generation. The design incorporates several critical components to ensure safe, efficient, and reliable operation. These include a high-capacity feed hopper with integrated level control, a positive displacement blower or rotary airlock for consistent air flow, and a specialized pipeline system that minimizes material degradation and blockage. The system is also equipped with advanced filtration and dust collection units to comply with environmental regulations and maintain air quality. Additionally, the design allows for easy maintenance and cleaning, reducing downtime and operational costs.
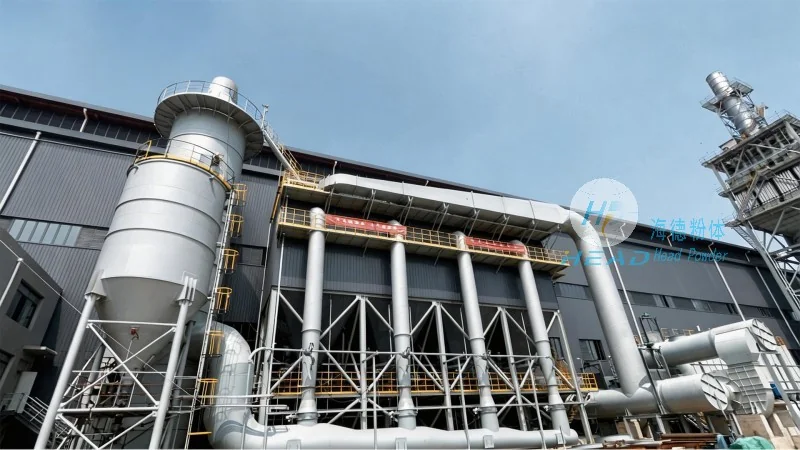
Technical Specifications and Performance Parameters
The ammonium bicarbonate pneumatic conveying equipment from HeadPowder is designed to meet specific performance requirements tailored to customer needs. Key technical specifications include a conveying capacity ranging from 0.5 to 10 tons per hour, depending on the system configuration. The system operates at pressures between 0.5 to 1.5 bar, with air flow rates optimized to handle the material’s flow characteristics. The equipment is constructed using corrosion-resistant materials, such as stainless steel, to withstand the chemical properties of ammonium bicarbonate and ensure long-term durability. The design also incorporates safety features, including pressure relief valves and emergency shut-off mechanisms, to protect both personnel and equipment during operation.
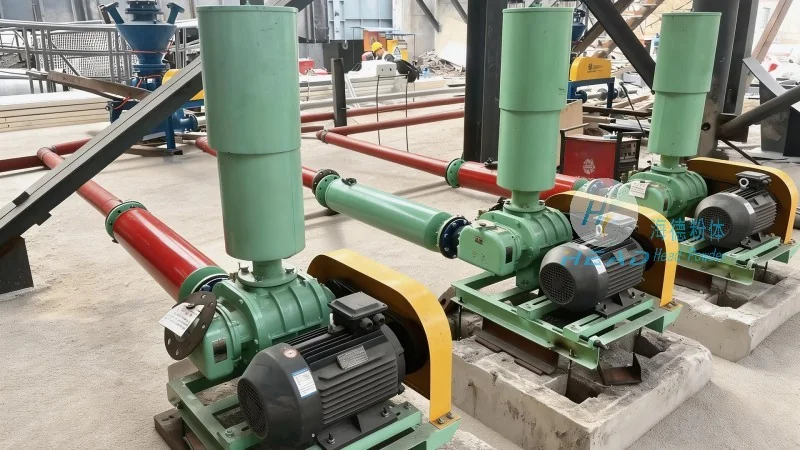
Application and Industry Benefits
The ammonium bicarbonate pneumatic conveying system is widely used in industries such as fertilizer production, food processing, and chemical manufacturing. By utilizing this system, companies can achieve significant improvements in operational efficiency, including reduced labor costs, minimized material loss, and enhanced process control. The system’s ability to handle bulk materials in a dust-free environment also contributes to better workplace safety and compliance with environmental standards. Furthermore, the modular design of the equipment allows for easy integration into existing production lines, providing flexibility and scalability for growing businesses.
Conclusion and Contact Information
Shandong HeadPowder Engineering Co., Ltd. offers a comprehensive range of ammonium bicarbonate pneumatic conveying solutions that are tailored to meet the specific needs of industrial applications. With a focus on quality, innovation, and customer satisfaction, HeadPowder provides reliable and efficient material handling systems that enhance productivity and reduce operational costs. For more information or to discuss customized solutions, please contact HeadPowder at their address in Shandong, China.




