Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced air-pneumatic conveying solutions tailored for the safe and efficient bulk transportation of sodium hydroxide. With a focus on industrial applications, our systems are designed to meet the demanding requirements of chemical processing and material handling in various sectors. This article explores the application of air-pneumatic conveying in the context of sodium hydroxide bulk handling, highlighting the technical advantages and operational benefits of such systems.
Understanding Sodium Hydroxide and Its Handling Challenges
Sodium hydroxide, commonly known as caustic soda, is a highly caustic and reactive chemical widely used in industries like paper manufacturing, textile processing, and chemical synthesis. Its bulk handling requires specialized equipment due to its corrosive nature and the need for precise control during transportation. Traditional methods such as belt conveyors or manual handling pose significant risks, including material degradation, safety hazards, and inefficiencies. Air-pneumatic conveying offers a solution by eliminating the need for direct contact with the material, reducing contamination risks and enhancing process reliability.
How Air-Pneumatic Conveying Works
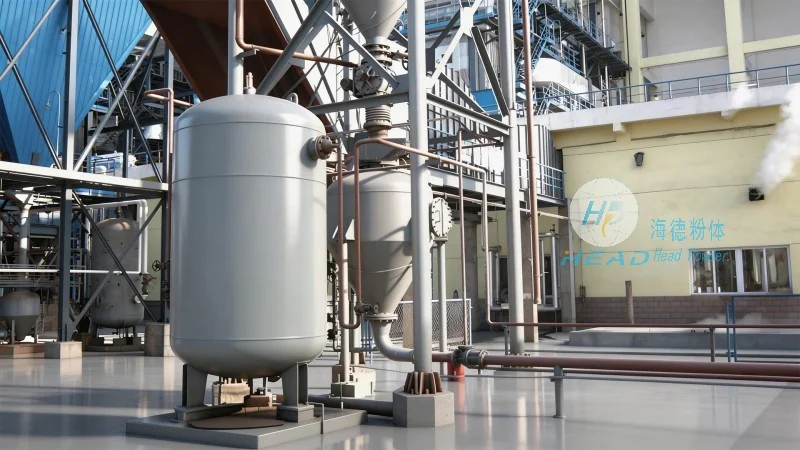
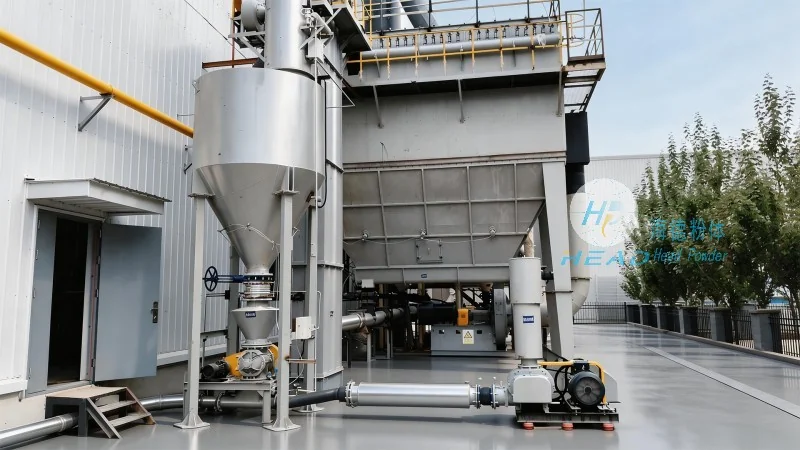
At its core, air-pneumatic conveying uses a combination of air pressure and vacuum to transport bulk materials through a network of pipes. The system typically consists of a hopper, a rotary airlock, a conveying line, and a receiver. For sodium hydroxide, the process involves feeding the material into the hopper, where it is mixed with air under controlled pressure. The air and material mixture is then propelled through the pipeline to the destination, such as a storage tank or processing unit. The system can operate in both positive pressure (blowing air) and negative pressure (suction) modes, providing flexibility for different application scenarios. The use of inert gases or filtered air ensures that the material remains dry and free from contaminants, which is crucial for maintaining the quality of sodium hydroxide.
Key Advantages of Air-Pneumatic Conveying for Sodium Hydroxide
One of the primary benefits of air-pneumatic conveying in sodium hydroxide handling is its ability to maintain material integrity. Unlike mechanical conveyors that can cause abrasion or degradation, pneumatic systems minimize physical contact, preserving the chemical's purity and reducing the risk of caking or agglomeration. This is particularly important for sodium hydroxide, which can become clumpy if not handled carefully, affecting downstream processes. Additionally, the system offers superior dust control, as the material is contained within the pipeline, preventing airborne particles from spreading and creating health hazards. This is a critical advantage in industrial environments where safety and compliance with regulations are paramount.
Customization and Scalability
Shandong HeadPowder Engineering Co., Ltd. understands that each industrial facility has unique requirements. Our air-pneumatic conveying systems are highly customizable to accommodate different capacities, material types, and operational conditions. Whether a small-scale application in a laboratory setting or a large-scale system for a chemical plant, our solutions can be tailored to meet specific needs. The systems are designed to be scalable, allowing for easy expansion as production demands grow. This flexibility ensures that clients can invest in a solution that grows with their business, avoiding the need for costly replacements or upgrades in the future.
Operational Efficiency and Cost Savings
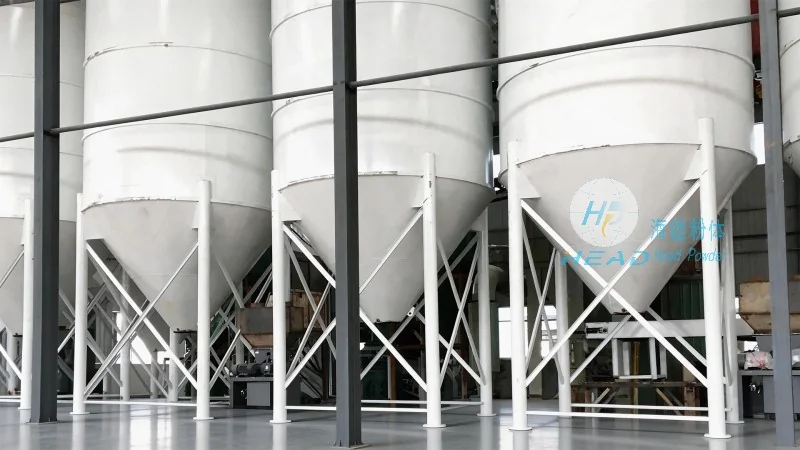
Implementing air-pneumatic conveying for sodium hydroxide handling can lead to significant operational efficiencies and cost savings. By automating the material transport process, the system reduces labor costs and minimizes human error. The continuous flow of material ensures consistent production rates, improving overall throughput. Additionally, the reduced need for maintenance compared to mechanical conveyors lowers long-term operational expenses. The system's ability to handle large volumes of material in a single operation further enhances productivity, making it an attractive option for businesses looking to optimize their supply chain and reduce downtime.
Safety and Compliance
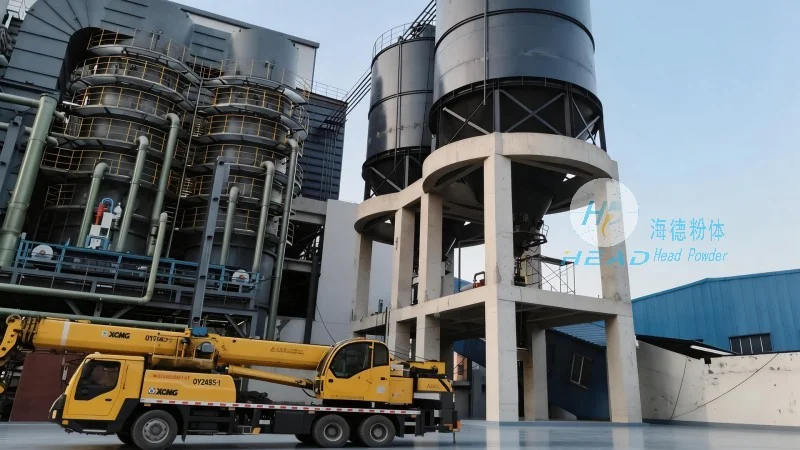
Safety is a top priority in the handling of sodium hydroxide, and air-pneumatic conveying systems are designed with this in mind. The enclosed pipeline system prevents accidental spills or leaks, minimizing environmental risks. The use of filtered air and inert gases ensures that the material is handled in a controlled environment, reducing the risk of exposure to workers. Compliance with industry regulations, such as those from OSHA and EPA, is a key consideration, and our systems are engineered to meet or exceed these standards. This not only protects the workforce but also helps businesses avoid costly penalties and maintain their reputation.
Conclusion
For industries dealing with sodium hydroxide, air-pneumatic conveying offers a reliable, efficient, and safe solution for bulk handling. Shandong HeadPowder Engineering Co., Ltd. provides expertly designed systems that address the unique challenges of this chemical, ensuring optimal performance and longevity. By leveraging the advantages of pneumatic transport, businesses can enhance their operational efficiency, reduce costs, and maintain compliance with safety regulations. As a leader in engineering solutions, we are committed to delivering high-quality air-pneumatic conveying systems that meet the evolving needs of the chemical industry.




