Calcium nitrite is a critical chemical compound widely used in various industrial applications, including water treatment, corrosion inhibition, and as a component in certain construction materials. The efficient and safe handling of this substance in bulk quantities is essential for industrial operations. Air-pneumatic conveying systems have emerged as a reliable solution for transporting calcium nitrite, offering advantages such as reduced dust generation, improved safety, and enhanced process control. This article explores the application of air-pneumatic conveying in the bulk handling of calcium nitrite, highlighting the technical aspects, benefits, and practical considerations for industrial users.
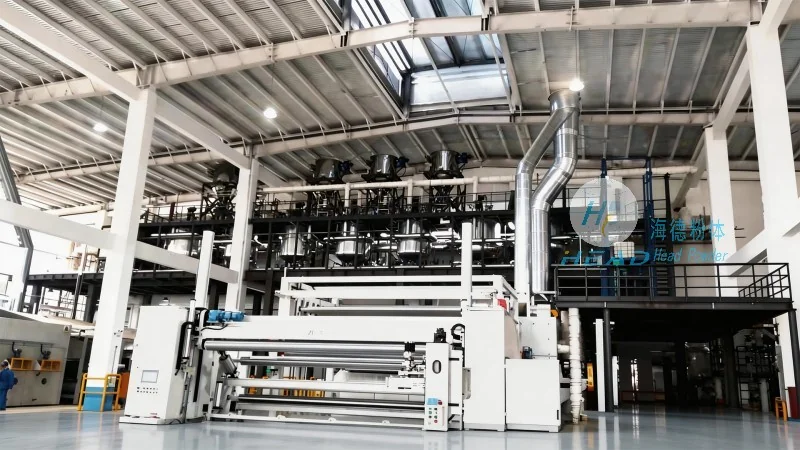
HeadPowder Engineering: A Leader in Bulk Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a specialized engineering company based in Shandong, China. With a strong focus on providing innovative and efficient bulk material handling solutions, HeadPowder has established itself as a trusted partner for industries requiring reliable transport systems for chemical powders. The company's expertise lies in designing and implementing air-pneumatic conveying systems tailored to the unique properties of materials like calcium nitrite. By leveraging advanced engineering principles and years of industry experience, HeadPowder ensures that its solutions meet the highest standards of performance, safety, and durability.
Key Features of Air-Pneumatic Conveying for Calcium Nitrite
When transporting calcium nitrite via air-pneumatic conveying, several key features contribute to the system's effectiveness. First, the system utilizes compressed air to move the material through a pipeline network, eliminating the need for mechanical components that might cause wear or contamination. This pneumatic approach significantly reduces the risk of product degradation and cross-contamination, which is particularly important for calcium nitrite due to its sensitivity to moisture and other environmental factors. Additionally, the conveying process can be precisely controlled, allowing for adjustable flow rates and pressure settings to match the specific requirements of the application. This flexibility ensures optimal performance while minimizing energy consumption and operational costs.
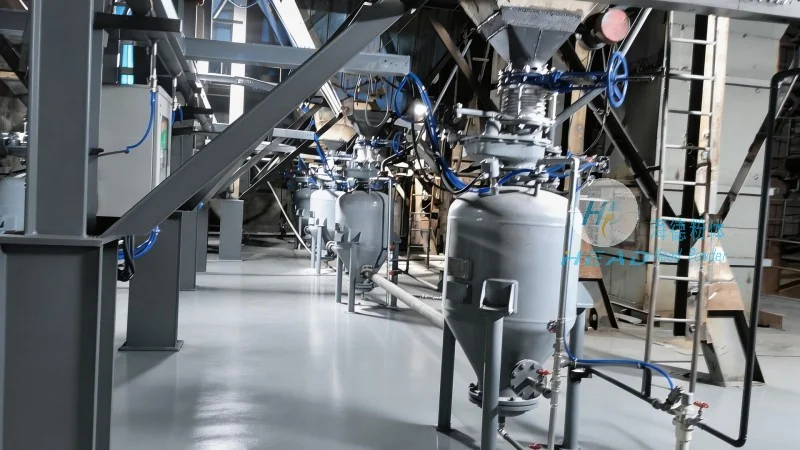
Benefits of Using Air-Pneumatic Conveying for Calcium Nitrite Handling
The adoption of air-pneumatic conveying for calcium nitrite offers numerous benefits that enhance overall operational efficiency and safety. One of the primary advantages is the reduction in dust exposure for personnel, as the enclosed system prevents the release of fine particles into the environment. This not only improves workplace safety but also complies with environmental regulations regarding dust emissions. Furthermore, the system's ability to handle calcium nitrite in bulk quantities reduces material handling costs and increases throughput, leading to higher productivity. The enclosed nature of the conveying system also minimizes product loss and spillage, contributing to better inventory management and cost savings. Another significant benefit is the improved process control, as the system allows for real-time monitoring and adjustment of flow rates, ensuring consistent quality and performance in downstream processes.
Technical Considerations for Air-Pneumatic Conveying Systems
Implementing an air-pneumatic conveying system for calcium nitrite requires careful consideration of several technical factors to ensure optimal performance and longevity. The first consideration is the material's physical properties, such as particle size, density, and moisture content. Calcium nitrite typically consists of fine particles, which can affect the system's flow characteristics and require specific design adjustments. The system's design must account for these properties to prevent blockages or uneven flow. Additionally, the choice of air pressure and flow rate is critical, as excessive pressure can lead to system wear and energy inefficiency, while insufficient pressure may result in incomplete material transport. HeadPowder engineers carefully evaluate these factors to design a system that matches the specific needs of the application, ensuring reliable and efficient operation.
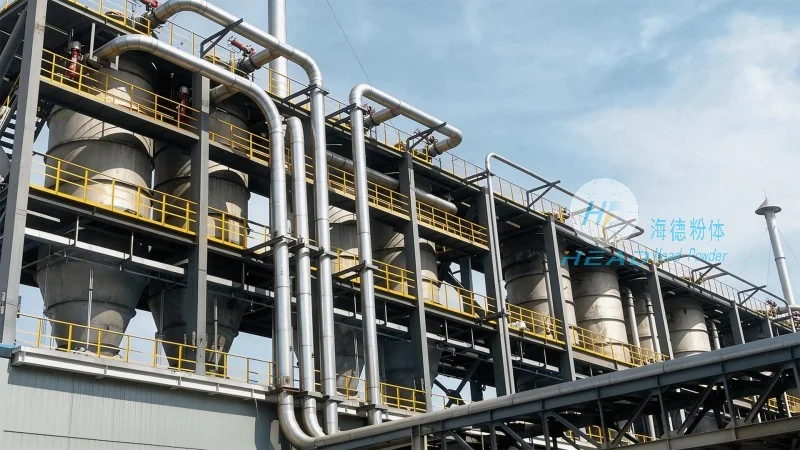
Application Examples and Case Studies
Air-pneumatic conveying systems have been successfully applied in various industrial settings for calcium nitrite handling. For instance, in water treatment facilities, the system efficiently transports calcium nitrite to dosing points, ensuring consistent dosing rates and improving water treatment efficiency. In construction material manufacturing, the system delivers calcium nitrite to mixing plants, maintaining consistent material quality and reducing downtime. These applications demonstrate the versatility and effectiveness of air-pneumatic conveying in handling calcium nitrite in bulk. HeadPowder has provided customized solutions for numerous clients, each tailored to their specific operational requirements and material handling challenges.
Conclusion and Future Outlook
Air-pneumatic conveying represents a highly effective and reliable method for the bulk handling of calcium nitrite. The technology offers significant advantages in terms of safety, efficiency, and process control, making it an ideal choice for industries requiring consistent and high-quality material transport. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industries can leverage advanced air-pneumatic conveying systems to enhance their operational performance and meet the demands of modern industrial processes. As the demand for efficient bulk material handling solutions continues to grow, air-pneumatic conveying is poised to remain a key technology in the chemical and industrial sectors, ensuring the safe and effective transport of critical materials like calcium nitrite.




