Understanding the classification and application of sintered fly ash pneumatic conveying systems is crucial for optimizing industrial material handling processes, especially in the context of environmental management and resource utilization. Sintered fly ash, a byproduct of cement and steel production, requires efficient and reliable transport solutions to meet modern industrial demands.
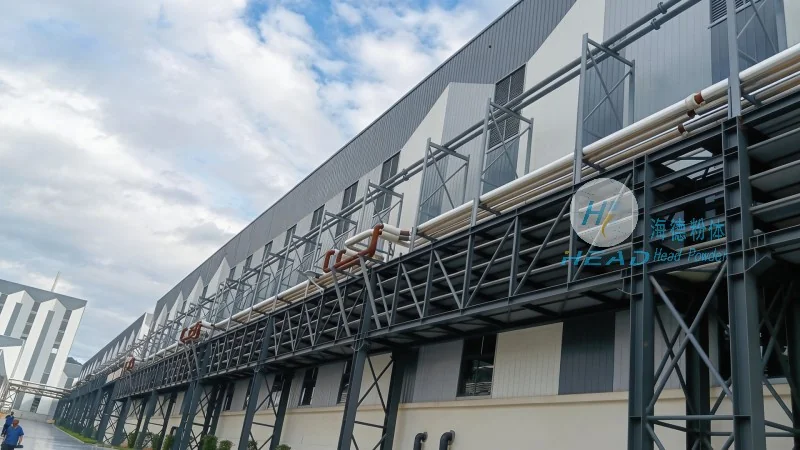
Classification of Pneumatic Conveying Systems for Sintered Fly Ash
Pneumatic conveying systems for sintered fly ash can be broadly categorized into three main types based on pressure differentials and operational principles: positive pressure, negative pressure, and mixed pressure systems. Each type offers distinct advantages and is suitable for different operational conditions and material characteristics.
Positive pressure systems operate by blowing air or gas into the conveying line, creating a pressure higher than the ambient air. This method is effective for transporting sintered fly ash over long distances and through complex pipe networks. The high pressure ensures consistent material flow and reduces the risk of blockages, making it ideal for large-scale industrial applications where high throughput is required.
Negative pressure systems, on the other hand, create a vacuum in the conveying line, drawing sintered fly ash into the system. This approach is often preferred for applications where dust control and environmental compliance are critical, as it minimizes the release of fine particles into the atmosphere. Negative pressure systems are commonly used in environments where air quality regulations are stringent, such as in urban or residential areas near industrial facilities.
Mixed pressure systems combine elements of both positive and negative pressure, offering flexibility in handling a wide range of material properties and operational requirements. These systems can adjust pressure differentials dynamically to optimize conveying efficiency and reduce energy consumption. For sintered fly ash, which can vary in moisture content and particle size, mixed pressure systems provide a balanced solution that ensures reliable transport while maintaining cost-effectiveness.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for industrial applications. With a focus on sustainability and efficiency, the company leverages cutting-edge technology to address the unique challenges of handling sintered fly ash, a material that demands precise control and minimal environmental impact.
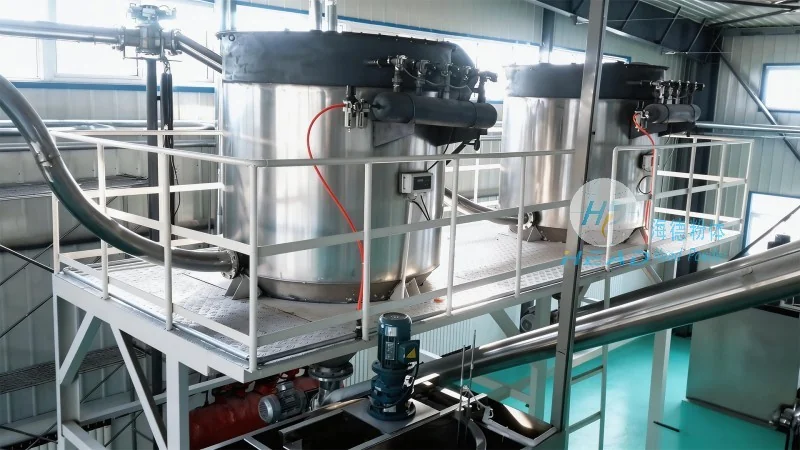
headpowder's expertise lies in customizing pneumatic conveying solutions to meet the specific needs of clients, whether for small-scale or large-scale operations. The company's team of engineers and technicians work closely with clients to understand their operational requirements, material characteristics, and environmental constraints, ensuring that the final system is optimized for performance, reliability, and compliance with industry standards.
Applications of Sintered Fly Ash Pneumatic Conveying Systems
The application of sintered fly ash pneumatic conveying systems spans multiple industries, primarily in the cement, steel, and power generation sectors. These systems are integral to the process of transporting sintered fly ash from storage silos to processing facilities, such as cement kilns or waste-to-energy plants. By eliminating the need for traditional bulk handling methods like trucks or conveyor belts, pneumatic systems reduce labor costs, minimize material handling time, and improve overall operational efficiency.
In the cement industry, sintered fly ash is often used as a supplementary cementitious material (SCM) to replace a portion of Portland cement. The efficient transport of fly ash to the cement production line is critical for maintaining consistent product quality and reducing raw material costs. Pneumatic conveying systems ensure that fly ash is delivered in a controlled manner, preventing clumping and ensuring uniform mixing with other raw materials.
In the steel industry, sintered fly ash may be used as a fuel or as a component in the production of iron ore pellets. The ability to transport fly ash over long distances without degradation is essential for maintaining the quality of the final product. headpowder's systems are designed to handle the high temperatures and abrasive properties of sintered fly ash, ensuring long-term durability and minimal maintenance.
Additionally, in power generation facilities, sintered fly ash can be utilized as a fuel in combined heat and power (CHP) plants. The pneumatic conveying systems used in these applications must be capable of handling large volumes of material and operating under high-temperature conditions. headpowder's solutions are engineered to meet these demanding requirements, providing reliable and cost-effective transport solutions that support the sustainability goals of modern power plants.
Advantages of Advanced Pneumatic Conveying Systems
Modern sintered fly ash pneumatic conveying systems offer several key advantages over traditional handling methods. One of the primary benefits is the reduction in dust emissions and environmental impact. By using enclosed systems with controlled air flow, these solutions minimize the release of fine particles into the atmosphere, helping facilities comply with stringent air quality regulations and reduce their carbon footprint.
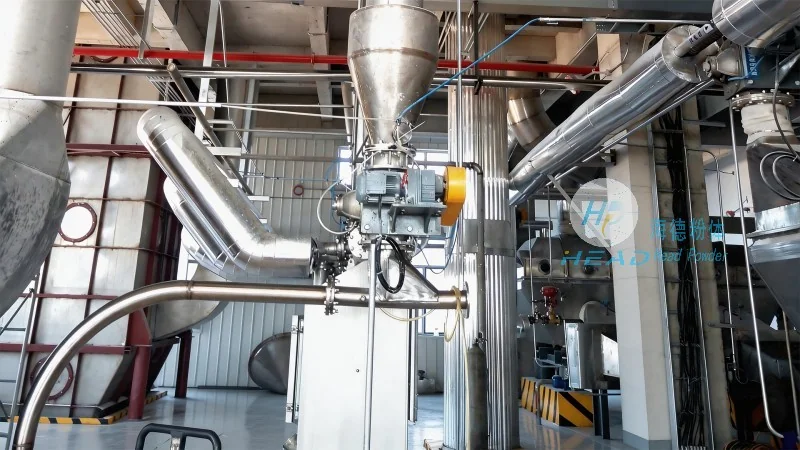
Another significant advantage is the improvement in operational efficiency and safety. Pneumatic systems eliminate the need for manual handling of bulk materials, reducing the risk of workplace accidents and labor costs. The automated nature of these systems ensures consistent material flow, reducing downtime and increasing overall productivity. For sintered fly ash, which can be abrasive and potentially hazardous, the enclosed design of pneumatic systems provides an additional layer of safety for operators and the surrounding environment.
Energy efficiency is also a critical factor in the design of modern pneumatic conveying systems. Advanced systems use variable frequency drives (VFDs) and optimized air flow control to minimize energy consumption while maintaining high conveying rates. This not only reduces operational costs but also aligns with the sustainability goals of industrial facilities. headpowder's systems are equipped with energy-saving features that help clients achieve significant reductions in their energy usage, contributing to lower operational expenses and a smaller environmental impact.
Furthermore, the flexibility of pneumatic conveying systems allows for easy integration with existing industrial infrastructure. Whether retrofitting an existing facility or designing a new plant, headpowder's solutions can be customized to fit the available space and operational constraints. The modular design of these systems enables quick installation and commissioning, minimizing project timelines and ensuring a smooth transition to the new material handling process.
Conclusion
Classification and application analysis of sintered fly ash pneumatic conveying systems highlight the importance of choosing the right technology for efficient and sustainable material handling. From positive to negative to mixed pressure systems, each approach offers unique benefits tailored to specific operational needs. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing customized solutions that address the challenges of handling sintered fly ash, ensuring that industrial facilities can meet their production goals while adhering to environmental regulations and sustainability objectives.
As the demand for efficient and eco-friendly material transport solutions continues to grow, the role of pneumatic conveying systems in the handling of sintered fly ash will become increasingly critical. By leveraging advanced technology and expert engineering, companies like headpowder are helping industrial clients optimize their operations, reduce costs, and contribute to a more sustainable future.




