HeadPowder, a leading enterprise in the field of dust collection and material handling, specializes in the design, manufacturing, and application of dust gas conveying systems. These systems are crucial for efficiently transporting dust and fine particles from industrial processes to designated disposal or treatment facilities. This article provides an in-depth classification of such systems and explores their practical applications.
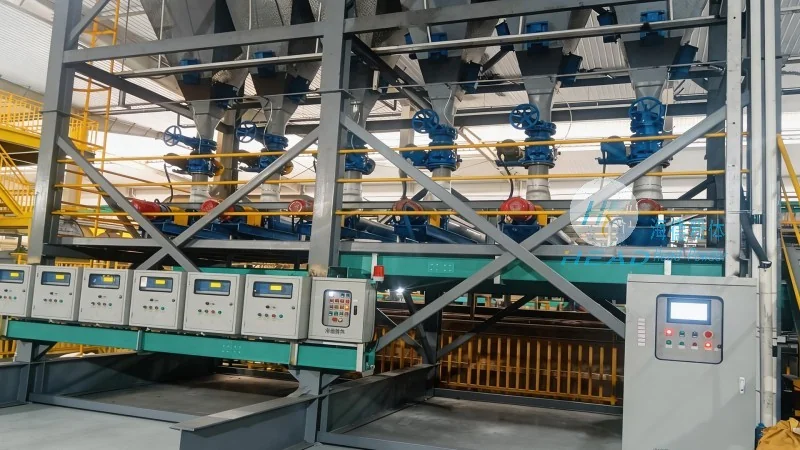
Classification of Dust Gas Conveying Systems
Dust gas conveying systems can be broadly categorized based on the pressure within the conveying pipeline. The primary classifications include positive pressure systems and negative pressure systems, each with distinct operational principles and suitability for different scenarios.
Positive pressure systems operate by generating a higher pressure inside the pipeline compared to the ambient air. This is typically achieved through a blower or fan that forces air (or a gas mixture) through the pipeline, carrying the dust particles along. The key advantages of positive pressure systems include their ability to handle abrasive materials, their suitability for long-distance conveying, and their relatively simple maintenance. However, they may require more energy and can pose higher safety risks due to the pressurized air.
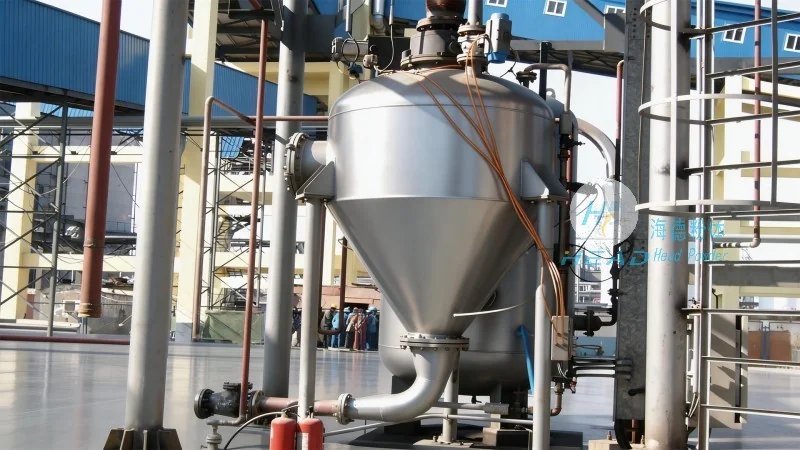
Negative pressure systems, on the other hand, create a lower pressure inside the pipeline than the surrounding environment. This is accomplished by drawing air and dust particles into the system using a vacuum pump or fan. Negative pressure systems are often preferred for applications where dust is generated in a confined space or where the risk of dust leakage is a concern. They are generally more energy-efficient for short to medium distances and are easier to install in existing facilities. Nonetheless, they may struggle with conveying highly abrasive or sticky materials and can be more prone to clogging.
Key Components of Dust Gas Conveying Systems
Regardless of the classification, dust gas conveying systems typically consist of several core components that work in tandem to ensure efficient operation. These components include a dust collection device (such as a cyclone separator or bag filter), a conveying pipeline, a blower or vacuum pump, and a dust discharge unit. The dust collection device is responsible for separating the dust particles from the air stream, while the blower or pump provides the necessary air flow to move the material. The pipeline transports the dust and air mixture to the discharge point, where the dust is collected and the air is either recirculated or released.
HeadPowder's dust gas conveying systems are engineered with high-quality materials and advanced technology to ensure durability and reliability. For example, our systems may incorporate stainless steel or corrosion-resistant materials for the pipeline to handle harsh environments, and advanced filtration systems to maintain air quality standards. The blower units are designed to deliver consistent airflow, even under varying load conditions, ensuring stable conveying performance.
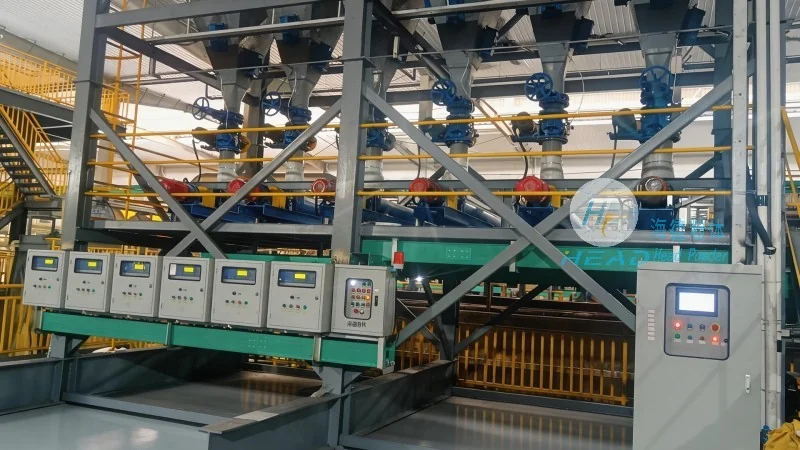
Applications of Dust Gas Conveying Systems
The versatility of dust gas conveying systems makes them applicable across a wide range of industries. In the cement industry, these systems are used to transport raw materials and finished products, such as cement powder, from storage silos to production lines. In the power generation sector, they are employed to convey fly ash from boilers to disposal sites or to re-use it as a raw material. The mining industry also utilizes dust gas conveying systems to transport coal dust or other mineral powders, improving safety and efficiency in mining operations.
In the chemical and pharmaceutical industries, dust gas conveying systems are essential for handling fine powders, such as chemicals or pharmaceuticals, which require precise control to prevent contamination or loss. The systems help maintain a clean and controlled environment, reducing the risk of dust explosions and ensuring product quality. Additionally, in the food processing industry, dust gas conveying systems are used to transport flour, sugar, or other food powders, adhering to strict hygiene standards.
Advantages of HeadPowder's Dust Gas Conveying Systems
HeadPowder, with its extensive experience and technical expertise, offers dust gas conveying systems that combine efficiency, reliability, and cost-effectiveness. Our systems are designed to meet the specific needs of each application, ensuring optimal performance and minimal downtime. The positive pressure systems from HeadPowder are known for their robust construction and ability to handle high-temperature or abrasive materials, making them suitable for demanding industrial environments. The negative pressure systems, meanwhile, provide a clean and safe solution for applications where dust containment is critical.
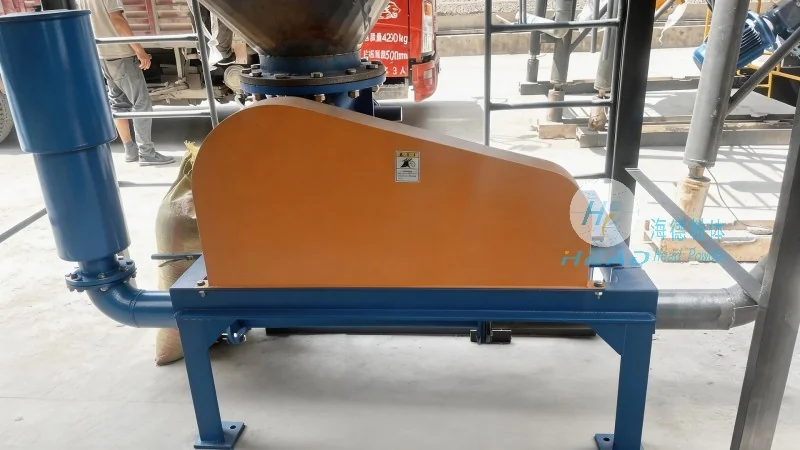
Furthermore, HeadPowder's dust gas conveying systems are equipped with advanced monitoring and control features. These features allow for real-time monitoring of airflow, pressure, and dust concentration, enabling operators to adjust the system parameters as needed. This not only improves operational efficiency but also extends the lifespan of the equipment by preventing excessive wear and tear.
Conclusion
Dust gas conveying systems are indispensable tools in modern industrial operations, providing efficient and safe methods for transporting dust and fine particles. The classification of these systems—positive pressure versus negative pressure—allows for selection based on specific operational requirements, such as material type, conveying distance, and safety considerations. HeadPowder, as a trusted provider in this field, offers high-quality dust gas conveying systems that are tailored to meet the diverse needs of various industries. By leveraging advanced technology and robust engineering, HeadPowder ensures that its systems deliver reliable performance, contributing to improved productivity and environmental compliance.




