Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in pneumatic conveying systems for solid powders. Our company, commonly known as HeadPowder, is headquartered in Shandong, China, and has established itself as a trusted provider of efficient and reliable equipment for the powder handling industry. This article aims to provide a comprehensive overview of solid powder pneumatic conveying equipment, detailing its structure and operational principles to help users understand its functionality and applications.
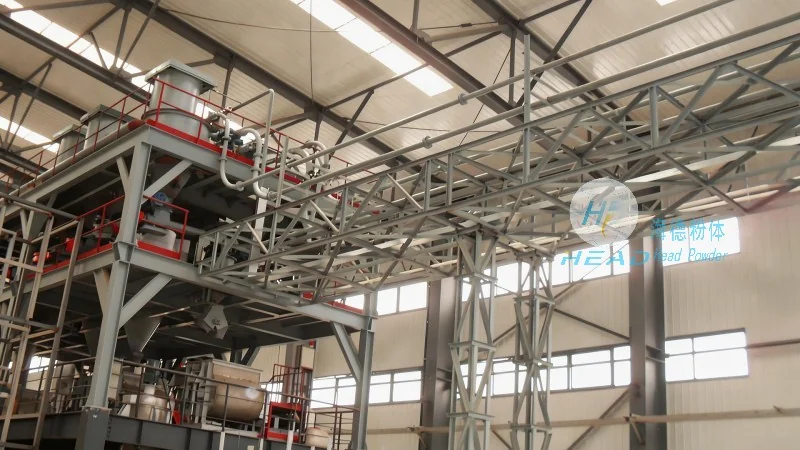
Understanding Pneumatic Conveying Systems for Solid Powders
Pneumatic conveying equipment is a critical component in industries that handle bulk solid powders, such as food processing, pharmaceuticals, chemicals, and minerals. Unlike traditional mechanical conveyors, which rely on physical contact and friction to move materials, pneumatic systems utilize compressed air or other gases to transport powders through a pipeline. This method offers several advantages, including reduced product contamination, improved safety by eliminating moving parts, and the ability to handle materials with high moisture content or sensitive characteristics.
Key Components of Solid Powder Pneumatic Conveying Equipment
The structure of a typical solid powder pneumatic conveying system consists of several essential components that work in tandem to ensure efficient material transport. The primary components include the hopper, feeder, air compressor, conveying line, and receiver. Each component plays a vital role in the overall operation of the system:
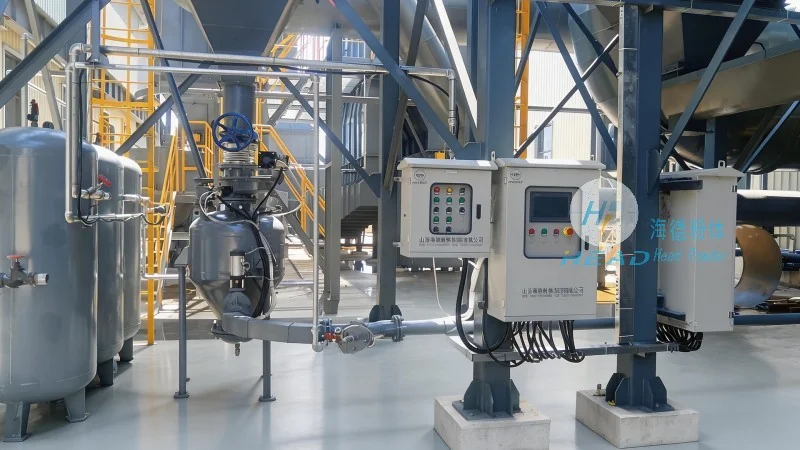
1. Hopper: The hopper is the storage container where the solid powder is held before it is fed into the system. It is designed to maintain a consistent material level and prevent clogging, often equipped with a discharge valve to control the flow rate. The design of the hopper, including its shape and internal surfaces, is crucial for preventing material buildup and ensuring smooth feeding.
2. Feeder: The feeder is responsible for controlling the flow of powder from the hopper into the conveying line. Common types of feeders include rotary valves, screw feeders, and vibratory feeders. The feeder must be able to handle the specific characteristics of the powder, such as particle size, density, and flowability, to maintain a consistent and controlled feed rate. This component is critical for preventing surges or blockages in the system.
3. Air Compressor: The air compressor generates the necessary pressure and volume of air to move the powder through the pipeline. The choice of compressor depends on the system's requirements, including the distance to be conveyed, the material's properties, and the desired flow rate. Compressors can be either positive displacement or centrifugal types, each with its own advantages and limitations. Proper maintenance of the compressor is essential to ensure consistent performance and minimize downtime.
4. Conveying Line: The conveying line is the pipeline through which the powder and air mixture travels. It is typically made of materials such as stainless steel, plastic, or metal, depending on the application and the properties of the powder. The line is equipped with bends, elbows, and other fittings to direct the flow and maintain the velocity of the material. The design of the line, including its diameter and length, is critical for achieving the desired conveying efficiency and preventing pressure losses.
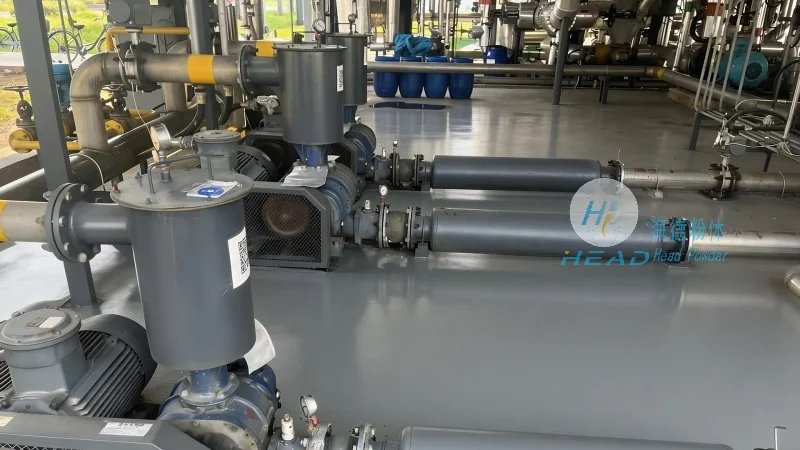
5. Receiver: The receiver is the final container where the conveyed powder is deposited. It is designed to collect the material and prevent it from escaping or being contaminated. The receiver may include a discharge valve or a hopper to control the outflow of the material. Proper sealing and maintenance of the receiver are essential to maintain the integrity of the system and prevent product loss.
Working Principle of Pneumatic Conveying for Solid Powders
The operation of a solid powder pneumatic conveying system involves several steps, each contributing to the efficient transport of the material. The process typically begins with the powder being fed from the hopper into the conveying line through the feeder. Simultaneously, the air compressor supplies compressed air to the line, creating a pressure differential that propels the powder forward. The powder particles are suspended in the air stream, forming a dense phase or dilute phase flow, depending on the system design and operating conditions.
In the dense phase conveying mode, the powder is transported as a slurry, with a higher concentration of particles in the air stream. This mode is suitable for short distances and materials that are prone to segregation or degradation. The dense phase system maintains a higher pressure and lower velocity, ensuring that the powder remains intact and prevents caking or agglomeration.
In the dilute phase conveying mode, the powder is transported as a suspension, with a lower concentration of particles in the air stream. This mode is suitable for longer distances and materials that are less sensitive to pressure changes. The dilute phase system operates at higher velocities and lower pressures, allowing for more efficient transport over greater distances.
The choice between dense and dilute phase conveying depends on factors such as the material's properties, the distance to be conveyed, and the desired flow rate. Both modes are widely used in the industry, and the selection is based on the specific requirements of the application.
Advantages and Applications of Solid Powder Pneumatic Conveying Equipment
Solid powder pneumatic conveying equipment offers numerous advantages over traditional mechanical conveyors, making it a preferred choice in many industries. Some of the key advantages include:
1. Reduced Product Contamination: Pneumatic systems minimize contact between the material and the conveyor components, reducing the risk of contamination from metal particles, dust, or other contaminants. This is particularly important in industries such as food, pharmaceuticals, and cosmetics, where product purity is critical.
2. Improved Safety: The absence of moving parts and the enclosed pipeline design reduces the risk of accidents and injuries. Additionally, the system can be designed to handle hazardous materials safely, with proper ventilation and explosion-proof features.
3. Flexibility and Versatility: Pneumatic conveying systems can be easily modified or expanded to accommodate changing production needs. The equipment can handle a wide range of materials, including fine powders, granules, and bulk solids, with varying particle sizes and flow properties.
4. Efficient Material Handling: The system can transport materials over long distances with minimal energy consumption and maintenance. The ability to handle high volumes of material efficiently makes it suitable for large-scale production operations.
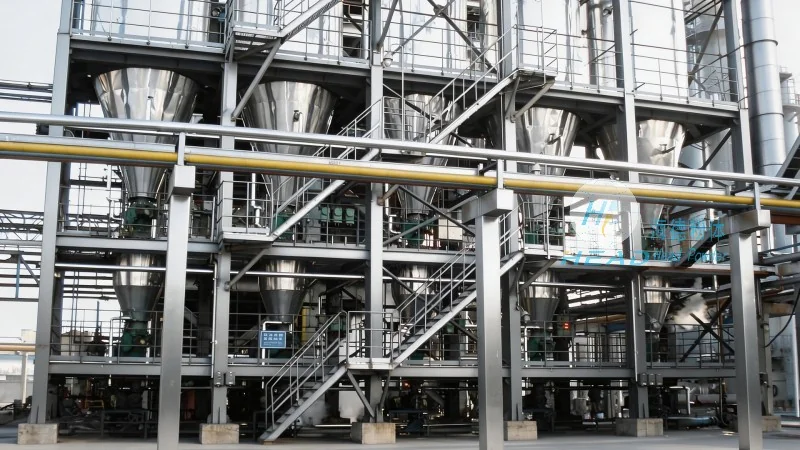
Applications of solid powder pneumatic conveying equipment are diverse and include:
1. Food and Beverage Industry: Conveying ingredients such as flour, sugar, and spices in food processing plants. The system ensures that the products remain fresh and free from contamination.
2. Pharmaceutical Industry: Transporting active pharmaceutical ingredients (APIs), excipients, and finished products in pharmaceutical manufacturing. The system maintains the purity and integrity of the materials.
3. Chemical Industry: Handling chemicals, pigments, and other powders in chemical processing plants. The system ensures safe and efficient transport of potentially hazardous materials.
4. Mineral and Mining Industry: Conveying minerals, ores, and other bulk solids in mining operations. The system can handle materials with high moisture content or abrasive properties.
Conclusion
Solid powder pneumatic conveying equipment is a sophisticated and efficient solution for handling bulk solid powders in various industries. The system's structure, which includes components such as the hopper, feeder, air compressor, conveying line, and receiver, works together to ensure reliable and safe material transport. The working principle, which involves the suspension of powder particles in an air stream, allows for the efficient movement of materials over long distances. The advantages of reduced contamination, improved safety, and flexibility make it a preferred choice for many applications. As a leading manufacturer, Shandong HeadPowder Engineering Co., Ltd. offers high-quality pneumatic conveying systems tailored to meet the specific needs of our clients, ensuring optimal performance and reliability in their operations.




