

What is an Automatic Quantitative Powder Bulk Material Pneumatic Conveying Equipment? What Are Its D
Automatic quantitative powder bulk material pneumatic conveying equipment is a specialized industrial system designed to transport and meter powders and bulk materials through an air-driven process. This technology plays a crucial role in various manufacturing and processing industries, ensuring precise and efficient material handling. The equipment integrates advanced control mechanisms and robust construction to meet the demands of modern production lines.
Key Components and Working Principle
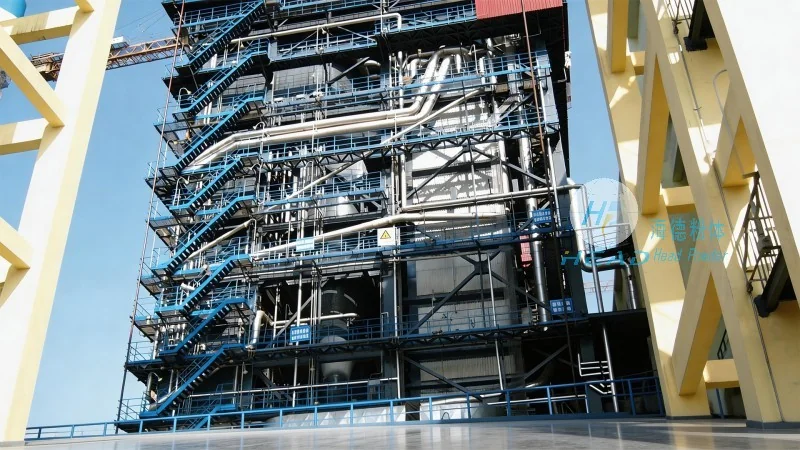
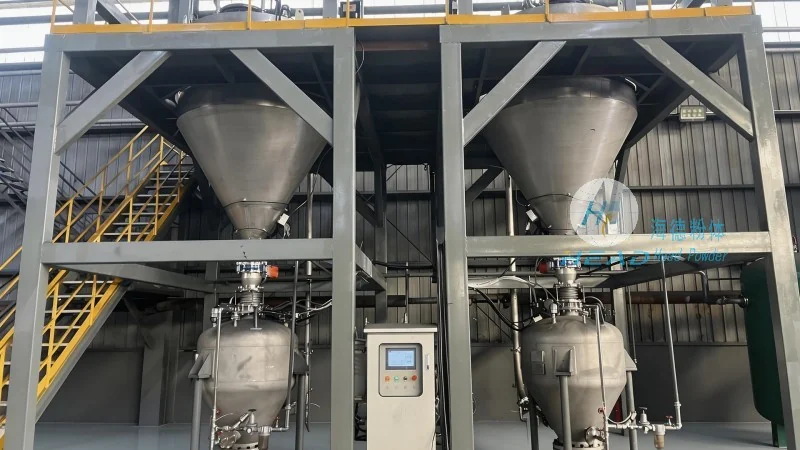
The core of this equipment lies in its integrated components, which work in synergy to achieve accurate material transfer. A typical system includes a hopper for material storage, a pneumatic conveying line, a rotary valve or feeder for controlled discharge, and a control unit for regulating air pressure and flow. The design principle revolves around creating a pressure differential between the material hopper and the receiving vessel, using compressed air to entrain the powder particles and transport them through the pipeline. The quantitative control is achieved through precise adjustment of air volume and pressure, ensuring consistent and repeatable dosing rates. This mechanism eliminates the need for manual intervention, reducing human error and enhancing operational efficiency.
The Role of HeadPowder in Design and Application
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design, development, and implementation of such pneumatic conveying systems. With a focus on innovation and customer-centric solutions, HeadPowder leverages years of industry experience to tailor equipment to specific client needs. The company’s headquarters is located in Shandong, China, where its engineering team employs cutting-edge technology and rigorous quality standards to produce reliable and durable equipment. By collaborating closely with clients, HeadPowder ensures that the final product aligns with operational requirements, process specifications, and safety regulations. The company’s commitment to excellence is reflected in its ability to deliver customized solutions that enhance productivity and reduce downtime in material handling operations.
Practical Applications and Industry Impact
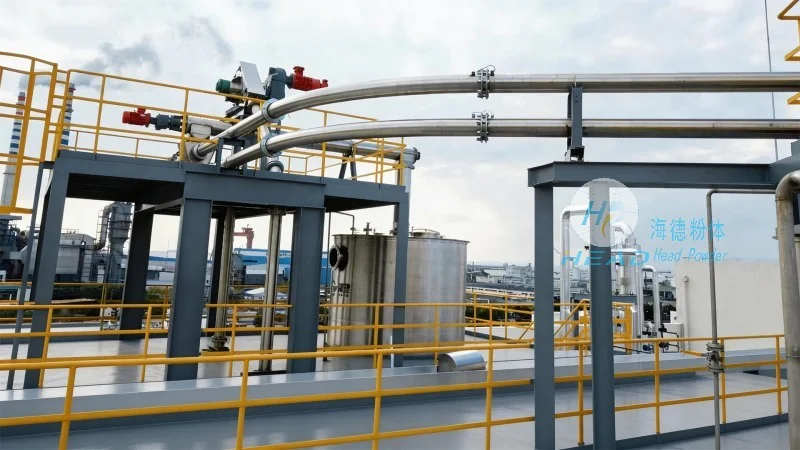
Automatic quantitative powder pneumatic conveying equipment finds widespread application across multiple sectors, including chemical processing, food and beverage, pharmaceuticals, and mining. In the chemical industry, it is used for transporting raw materials like powders and granules, ensuring precise dosing in reaction processes. The food and beverage sector benefits from its ability to handle ingredients such as flour, sugar, and spices, maintaining hygiene standards and preventing contamination. In pharmaceutical manufacturing, the equipment’s accuracy and cleanliness are critical for producing high-quality medications, adhering to stringent regulatory requirements. The mining industry utilizes it for transporting bulk materials like ore and coal, improving operational efficiency and reducing labor costs. Overall, the equipment’s design principles and functionality contribute significantly to process optimization, cost reduction, and improved product quality across diverse industrial applications.