

Working Principle and Features of Coal Ash Particle Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer based in Shandong, China. The company specializes in the design, development, and production of advanced pneumatic conveying equipment, particularly for handling coal ash particles. This article aims to provide a detailed explanation of the working principle and key features of coal ash particle pneumatic conveying equipment, highlighting the technical aspects and practical applications of such systems.
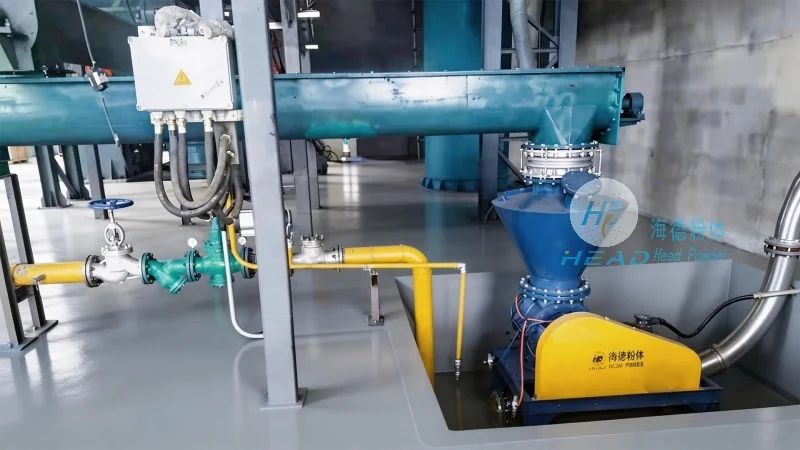
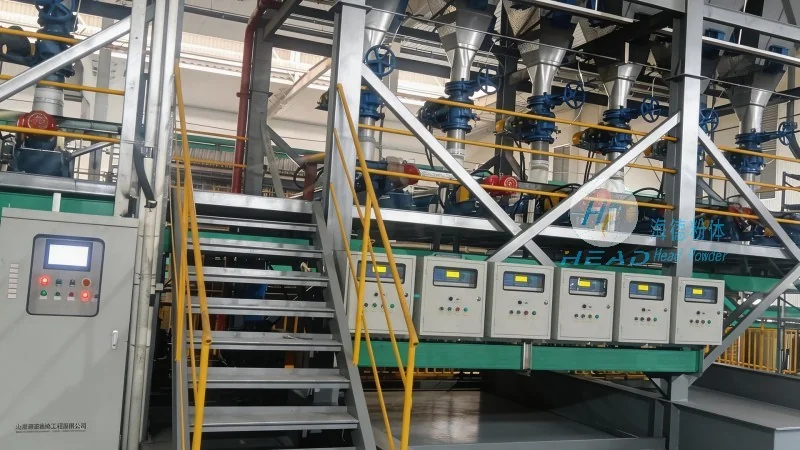
Working Principle of Coal Ash Particle Pneumatic Conveying Equipment
The core working principle of coal ash particle pneumatic conveying equipment is based on the fundamental concept of pneumatic transport, which involves the movement of solid particles through a pipeline using a gas stream. In the case of coal ash granule systems, the equipment typically operates using either an aspirating (suction) or pressurized (pressure) mode. The aspirating system draws the coal ash particles into the pipeline by creating a negative pressure at the inlet, while the pressurized system forces the particles through the pipeline by generating positive pressure from a blower or compressor. The process begins with the coal ash being fed into the inlet hopper, where it is then entrained by the high-velocity air stream. The air and particles travel through the pipeline, and the system includes components such as a separator, a filter, and a silencer to ensure efficient separation of the particles from the air and proper noise control. The separator typically uses a cyclone or bag filter to separate the coal ash from the air, while the silencer reduces the noise generated by the air movement. The entire system is designed to maintain a consistent flow rate and particle size distribution, ensuring reliable and continuous operation.
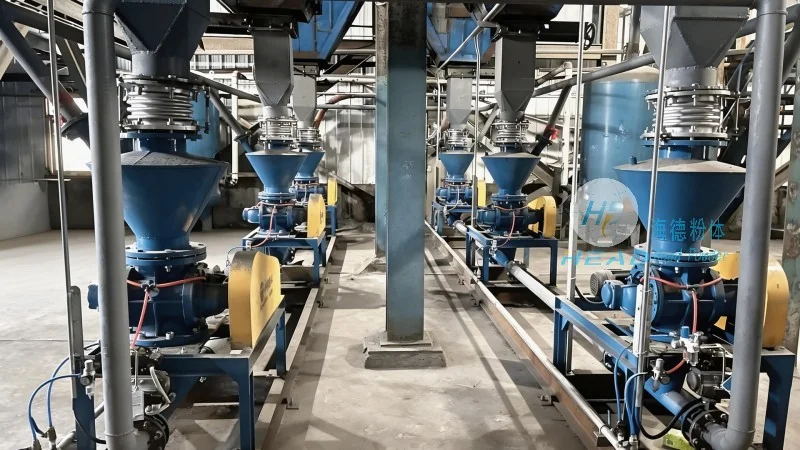
Key Features of Coal Ash Particle Pneumatic Conveying Equipment
Coal ash particle pneumatic conveying equipment offers several distinct advantages that make it an ideal solution for handling coal ash in industrial applications. Firstly, it provides a highly efficient and continuous method of transporting coal ash particles over long distances, with minimal manual intervention required. The system is capable of handling a wide range of particle sizes and moisture contents, making it versatile for various coal ash processing scenarios. Secondly, the equipment is designed with environmental considerations in mind, as it minimizes dust emissions and noise pollution compared to traditional methods like bucket elevators or belt conveyors. The enclosed pipeline system ensures that dust is contained and filtered, reducing the risk of air pollution and improving workplace safety. Thirdly, the system is relatively compact and easy to install, with modular components that can be customized to fit specific site requirements. This flexibility allows for easy integration into existing coal ash handling facilities or new construction projects. Additionally, the equipment is known for its low maintenance requirements and long service life, contributing to cost-effective operation over time. The use of high-quality materials and advanced manufacturing techniques ensures durability and reliability, even under harsh operating conditions. Finally, the system can be integrated with other processing equipment, such as storage silos or mixing systems, to form a complete coal ash handling solution, enhancing overall operational efficiency.
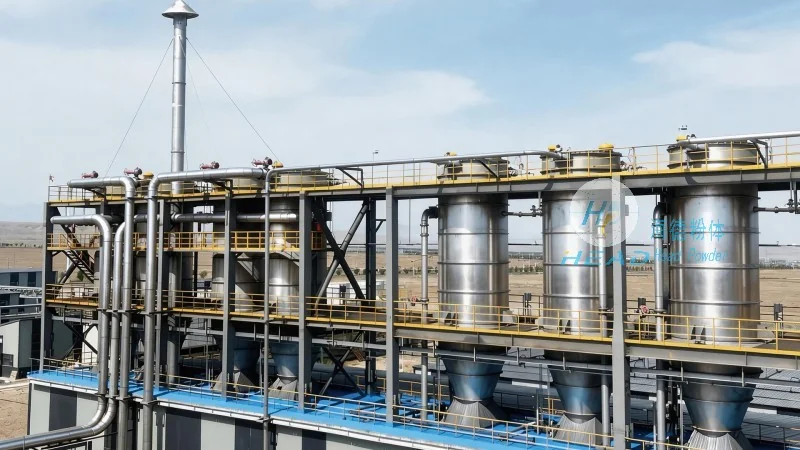
Technical Specifications and Application Examples
Shandong HeadPowder Engineering Co., Ltd. offers a range of coal ash particle pneumatic conveying equipment with varying technical specifications to meet different industrial needs. The systems can be customized in terms of pipeline length, particle size range, and flow rate, with options for both aspirating and pressurized operation. For example, a typical aspirating system may handle coal ash particles with a size range of 0.1 to 5 mm and a flow rate of 0.5 to 10 tons per hour, depending on the specific application. The pressurized system can handle higher flow rates and longer distances, making it suitable for large-scale coal ash disposal projects. The company's equipment has been successfully applied in power plants, cement factories, and other industrial facilities where coal ash needs to be transported from storage silos to processing or disposal areas. The systems have demonstrated high reliability and performance in real-world scenarios, with minimal downtime and maintenance costs. Clients have reported significant improvements in operational efficiency and environmental compliance after implementing headpowder's coal ash particle pneumatic conveying equipment.