Grain silo pneumatic conveying systems are crucial for efficient bulk material handling in agricultural and food processing sectors. These systems leverage air to transport grains, seeds, and powders, offering a reliable and flexible solution for moving materials from storage silos to processing facilities or other destinations.
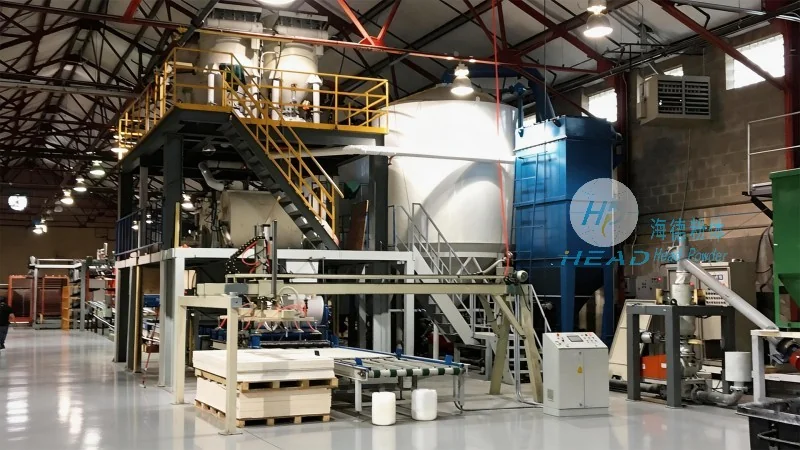
Working Principle of Pneumatic Conveying Systems
The fundamental operation of a grain silo pneumatic conveying system involves generating airflow using a blower or fan. This air is channeled through a pipeline network connecting the grain silo to the discharge point. As the air flows, it draws grain particles into the pipeline via a hopper or inlet. The air velocity is precisely controlled to ensure smooth material movement without causing excessive wear or degradation. The system typically comprises components like a silo, conveying line, receiver, and a control unit. The control unit manages airflow and pressure to optimize the conveying process, ensuring consistent and efficient material transfer.
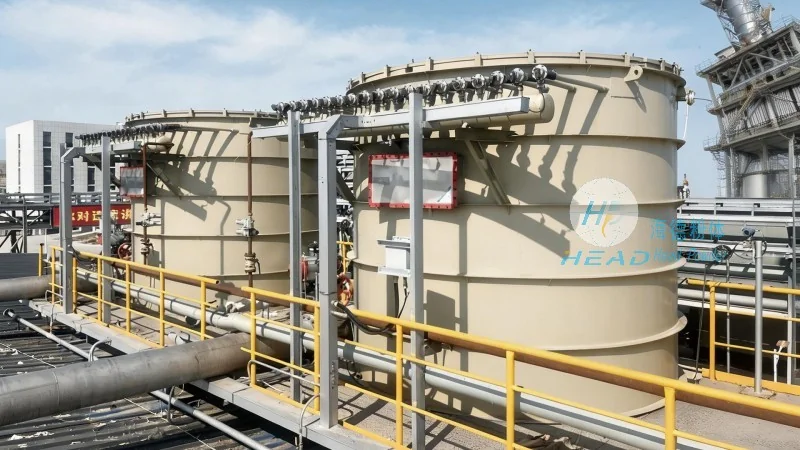
Key Features of Grain Silo Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, provides advanced pneumatic conveying systems with notable features. These systems are engineered for high efficiency, capable of handling large grain volumes with low energy consumption. The equipment is constructed from durable materials such as stainless steel and high-quality plastics to withstand the corrosive and abrasive nature of grain materials, ensuring long-term reliability and minimal maintenance. Additionally, the systems feature advanced control technologies for precise airflow and pressure regulation, enabling operators to adjust conveying speed and volume as needed for enhanced flexibility and operational efficiency. Safety features like pressure relief valves and overload protection are also integrated to prevent accidents and ensure safe operation.
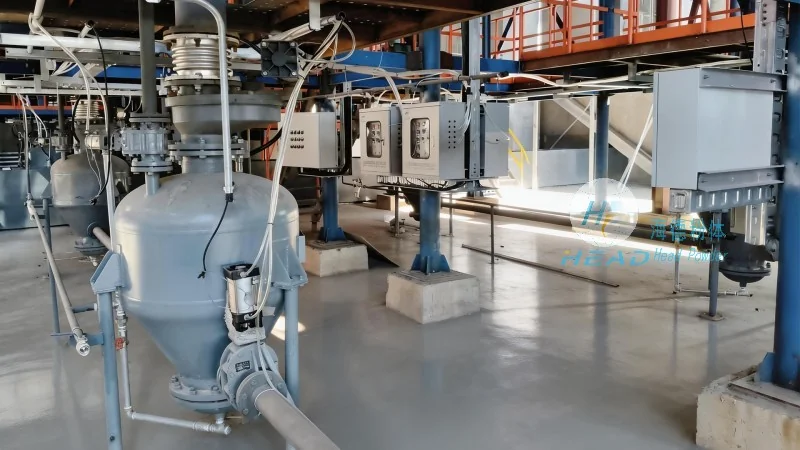
Benefits of Pneumatic Conveying in Grain Storage
Implementing a pneumatic conveying system in grain silos offers significant advantages for agricultural operations. First, it reduces labor costs by automating material handling, eliminating the need for manual grain transport which is labor-intensive and risky. Second, the system enhances hygiene and food safety by minimizing direct human contact with the grain, preserving product quality and integrity—critical for food-grade grains. Third, it improves storage efficiency by enabling continuous, controlled discharge from the silo, preventing pressure buildup and reducing spoilage or pest risks. Furthermore, the systems are adaptable to various grain types and sizes, suitable for diverse agricultural applications without frequent system modifications.
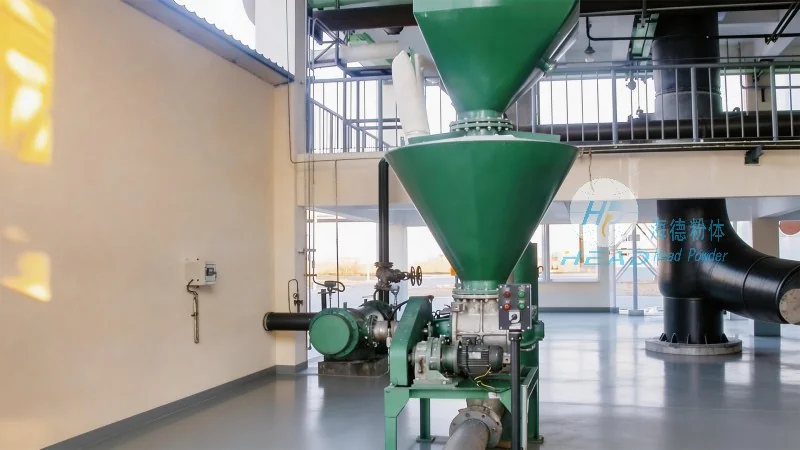
Customization and Application Scope
HeadPowder Engineering Co., Ltd. specializes in customized pneumatic conveying solutions tailored to client needs. Engineers collaborate with customers to assess operational requirements, including grain type, volume, transport distance, and discharge location. Based on these assessments, systems are designed and manufactured to exact specifications. The company’s product line includes both positive and negative pressure systems: positive pressure is ideal for short-distance vertical lifting, while negative pressure suits long-distance horizontal transport. Systems can integrate with existing silo infrastructure or be installed as new setups. HeadPowder also offers after-sales support, including maintenance and technical assistance, ensuring optimal performance throughout the system's lifespan.




