For industrial applications involving the handling of fly ash, efficient and reliable material transport is crucial. The fly ash silo pneumatic conveying system equipment, offered by Shandong HeadPowder Engineering Co., Ltd., is designed to meet these demands by providing a robust solution for transporting fly ash from storage silos to processing or disposal units. This article explores the working principle and key features of this system, highlighting its advantages in modern industrial operations.
Working Principle of the Pneumatic Conveying System
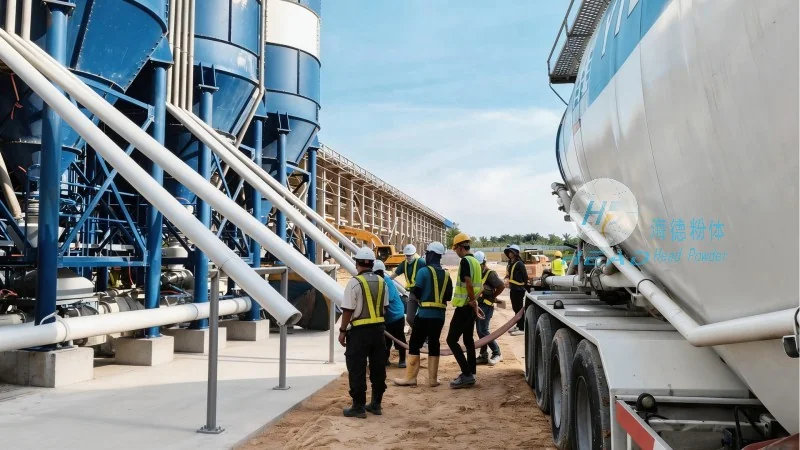
The core of the fly ash silo pneumatic conveying system lies in its pneumatic transport mechanism. The system operates by creating a pressure differential between the silo and the discharge point. Compressed air is introduced into the silo, which lifts the fly ash particles and propels them through a pipeline network to the destination. The process involves several key components: the fly ash silo, a blower or air compressor, a conveying line, and a receiver or discharge unit. The blower generates the necessary airflow to move the fly ash, while the pipeline ensures the material is transported in a controlled manner. The system typically uses positive pressure or negative pressure depending on the specific application requirements. Positive pressure systems push the material through the pipeline, while negative pressure systems draw it from the silo. This flexibility allows the system to be adapted to various industrial settings, ensuring optimal performance for different fly ash handling scenarios.
Key Features of the Fly Ash Silo Pneumatic Conveying System
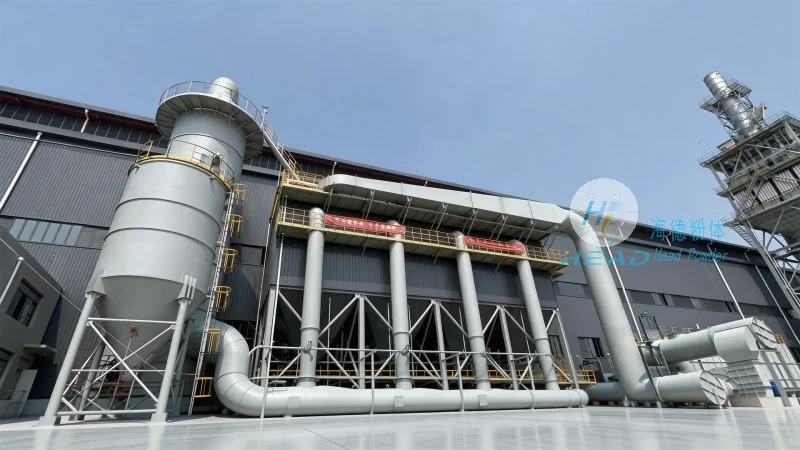
Shandong HeadPowder Engineering Co., Ltd. has integrated several advanced features into their fly ash silo pneumatic conveying system to enhance efficiency and reliability. One of the primary features is the use of high-quality materials for the conveying line and components, which ensures durability and resistance to corrosion from fly ash particles. The system is equipped with a sophisticated control panel that allows for real-time monitoring and adjustment of the airflow and pressure, enabling operators to maintain optimal conditions for fly ash transport. Additionally, the system includes safety features such as pressure relief valves and overcurrent protection to prevent accidents and equipment damage. The design of the system also minimizes material loss and contamination, as the conveying process is enclosed and controlled, reducing the risk of dust emissions and environmental impact. Another notable feature is the modular construction, which allows for easy installation and maintenance. The system can be customized to fit specific silo sizes and conveying distances, ensuring a tailored solution for each client's needs. This adaptability is a significant advantage, as it allows the system to be integrated seamlessly into existing industrial facilities without major modifications.
Advantages in Industrial Applications
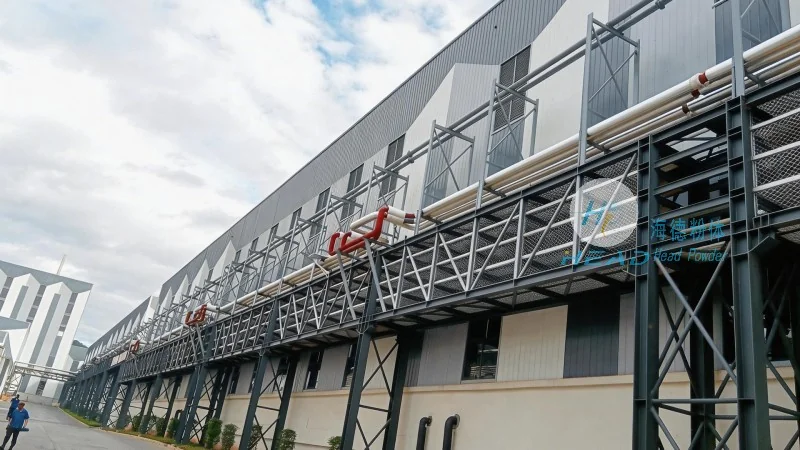
The fly ash silo pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers several advantages that make it a preferred choice for industrial applications. Firstly, the system provides a dust-free and clean transport process, which is essential for maintaining a safe working environment and complying with environmental regulations. Unlike traditional mechanical conveying methods, which can generate significant dust and require additional dust control measures, the pneumatic system minimizes airborne particles, reducing the risk of respiratory issues and contamination. Secondly, the system is highly efficient in terms of energy consumption and material transport speed. The use of compressed air allows for rapid movement of fly ash, reducing downtime and increasing overall productivity. This efficiency is particularly beneficial in high-volume industrial operations where continuous material flow is critical. Thirdly, the system is low-maintenance, with components designed for long-term operation and minimal wear. The use of robust materials and advanced engineering reduces the need for frequent repairs and replacements, resulting in lower operational costs over the system's lifespan. Finally, the system is versatile and can be adapted to various fly ash types and handling requirements. Whether dealing with dry or slightly moist fly ash, the system can be adjusted to ensure optimal performance, making it suitable for a wide range of industrial applications.
Conclusion
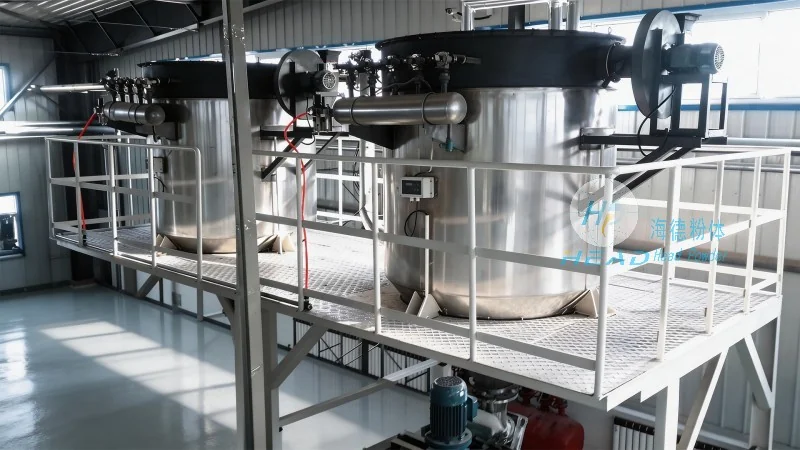
In conclusion, the fly ash silo pneumatic conveying system equipment from Shandong HeadPowder Engineering Co., Ltd. is a reliable and efficient solution for transporting fly ash in industrial settings. The system's working principle, based on pneumatic transport, ensures effective material movement from the silo to the discharge point. Key features such as durable components, advanced control systems, and safety features enhance its performance and longevity. The advantages of this system, including dust-free operation, high efficiency, low maintenance, and adaptability, make it an ideal choice for various industrial applications. By providing a tailored solution that meets specific client needs, Shandong HeadPowder Engineering Co., Ltd. continues to be a leader in the development and implementation of advanced fly ash handling systems.




