Working Principle and Features of Flake Graphite Powder Pneumatic Conveying System Equipment
Release time:2026-09-17 09:01:23
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for flake graphite powder. This article delves into the operational principles and key characteristics of such systems, providing a comprehensive overview for industry professionals.
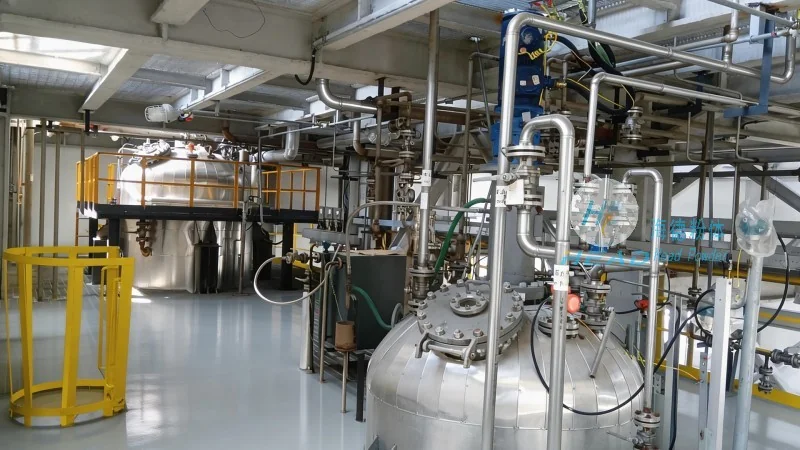
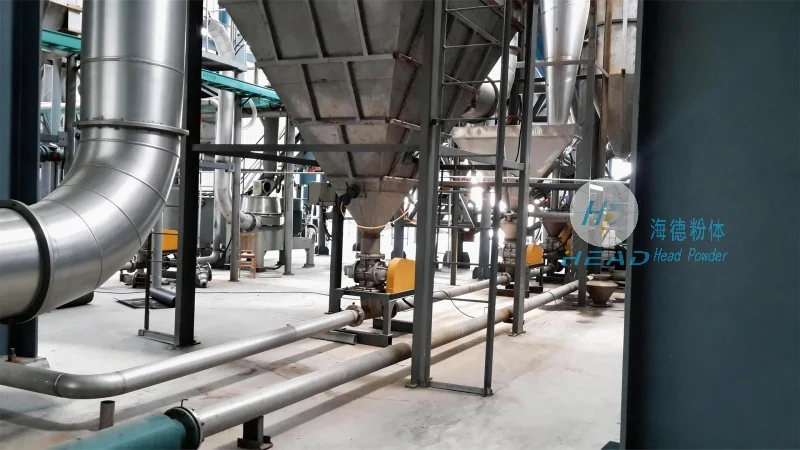
Company Overview
HeadPowder Engineering Co., Ltd. is a reputable enterprise dedicated to delivering high-quality industrial solutions. With a strong presence in Shandong, China, the company leverages its expertise to develop efficient and reliable equipment for material handling, particularly in the processing of flake graphite powder. The company's commitment to innovation and precision ensures that its products meet the stringent demands of modern industrial applications.
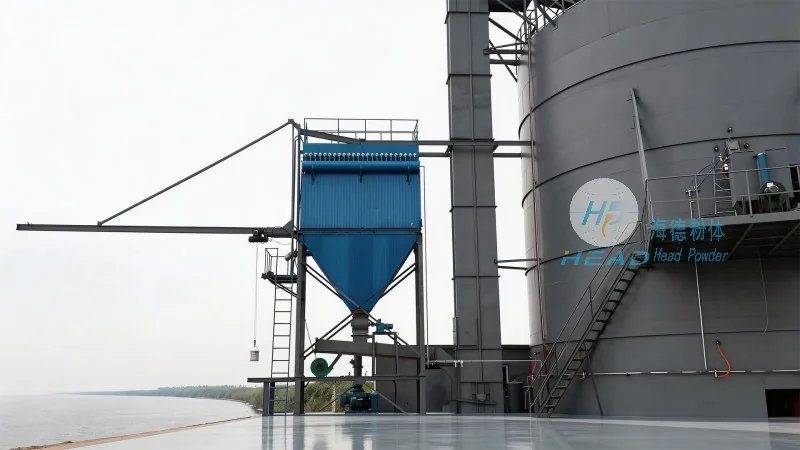
Working Principle of Flake Graphite Powder Pneumatic Conveying Systems
The pneumatic conveying system for flake graphite powder operates on the principle of transporting bulk materials through a pressurized or vacuumed air stream. In a typical setup, the system consists of a hopper, a conveyor line, and a receiver. The process begins with the graphite powder being fed into the hopper, where it is then drawn into the conveyor line by the moving air. The air, often under pressure, propels the powder particles through the pipeline, ensuring a smooth and continuous flow. Key components include the air compressor, which generates the necessary pressure, and the control valves that regulate the airflow and material transport. The system is designed to handle the unique properties of flake graphite, such as its low density and fine particle size, by optimizing the air velocity and pipeline design to prevent particle degradation and blockages.
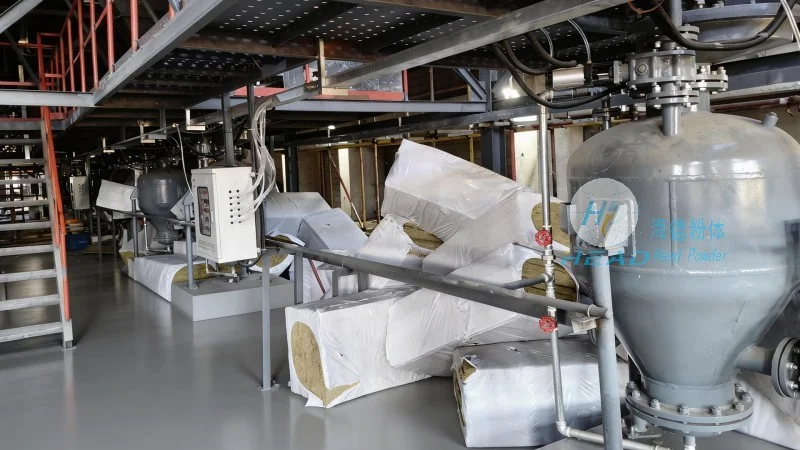
Key Features of the Pneumatic Conveying System
Several notable features distinguish the flake graphite powder pneumatic conveying system from conventional methods. Firstly, it offers a dust-free and hygienic transport solution, which is crucial for maintaining product purity and compliance with industry standards. The system's ability to handle fine and delicate particles without causing attrition or damage is another significant advantage. Additionally, the design allows for flexible and modular installation, enabling customization to fit various production environments and scale requirements. Energy efficiency is also a key aspect, as the system minimizes power consumption by optimizing air usage and reducing unnecessary losses. Furthermore, the system provides real-time monitoring capabilities, allowing operators to track the flow rate and identify any potential issues promptly, thereby enhancing overall operational reliability.




