For industries dealing with bulk powders, efficient and reliable handling systems are crucial. Tote bag unpacking powder conveying systems offer a solution that streamlines the process of transferring materials from large tote bags into processing lines. This article explores the working principle and key features of such systems, highlighting how they enhance operational efficiency and safety in powder handling applications.
Working Principle of the System
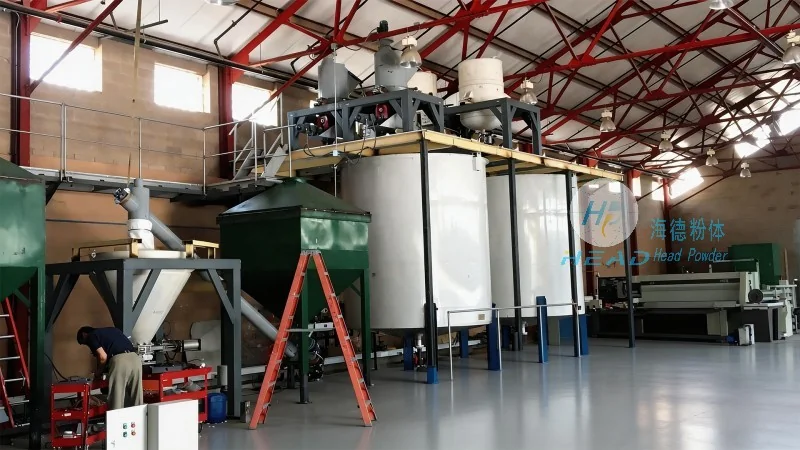
The core working principle of a tote bag unpacking powder conveying system involves several integrated steps. First, the system uses a tote bag unloader to open and empty the bulk material from the tote bag into a hopper or storage tank. This is typically achieved through mechanisms like vacuum or pressure-assisted unloading, which ensure complete material transfer with minimal waste. Next, the material is fed into a conveyor system, such as a screw conveyor or pneumatic conveyor, which transports the powder to the next stage of processing. The system may also include components like a dust collection unit to manage airborne particles and maintain a clean working environment. Overall, the process is automated, reducing manual labor and the risk of contamination.
Key Features and Advantages
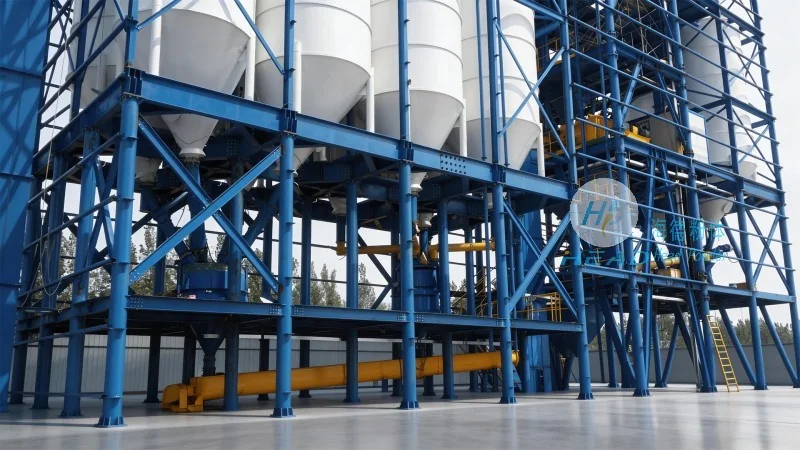
One of the primary features of these systems is their ability to handle a wide range of powder types, from fine powders to bulkier granules, without clogging or degradation. The design incorporates robust materials and components that resist corrosion and wear, ensuring long-term durability. Another key feature is the integration of safety measures, including dust suppression systems and emergency stop buttons, which protect operators and comply with industrial safety standards. Additionally, the systems are often modular, allowing for easy installation and integration into existing production lines. The advantages of using a tote bag unpacking powder conveying system include increased throughput, reduced labor costs, and improved product quality by minimizing material loss and contamination.
Application Scenarios and Benefits
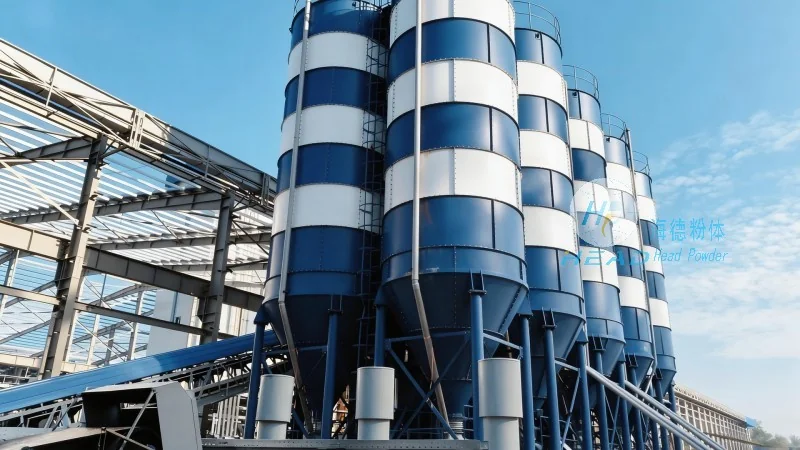
These systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, for example, they are used to handle ingredients like flour, sugar, and spices, ensuring hygienic and efficient transfer. In the pharmaceutical sector, the systems maintain strict contamination control, which is critical for drug manufacturing. The benefits extend to improved workplace safety, as the automated process reduces the need for manual handling of heavy tote bags and reduces exposure to dust and airborne particles. Furthermore, the systems contribute to operational efficiency by minimizing downtime and maintenance requirements, as their components are designed for easy access and maintenance.
Technical Specifications and Customization Options
Technical specifications of tote bag unpacking powder conveying systems vary based on the application and material being handled. Common specifications include the capacity of the system (measured in tons per hour), the type of conveyor (screw, pneumatic, or belt), and the dimensions of the tote bag unloader. For example, a system designed for a food processing plant might have a capacity of 5-10 tons per hour and use a stainless steel screw conveyor to ensure food-grade compliance. Customization options are available to meet specific needs, such as adding a material dryer or a mixing unit to the system. The systems can also be equipped with sensors and controls to monitor performance and alert operators to any issues, enhancing overall system reliability.
Conclusion and Company Profile
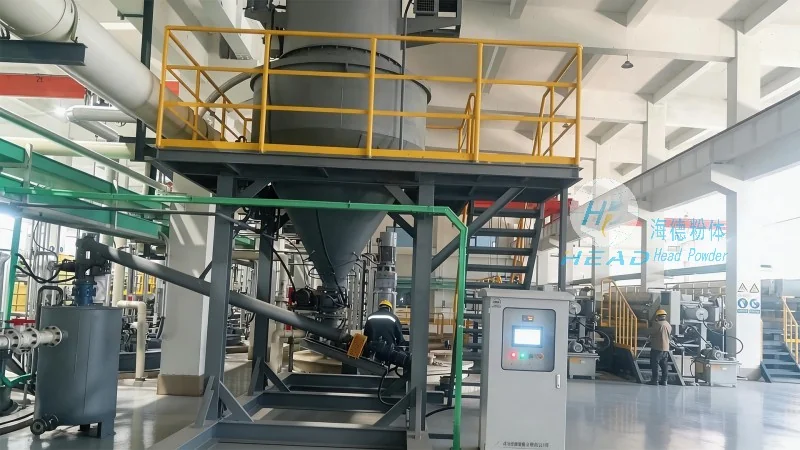
Tote bag unpacking powder conveying systems are essential equipment for industries that rely on bulk powder handling. By combining efficient unloading, reliable conveying, and safety features, these systems improve operational efficiency and product quality. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in designing and manufacturing such systems tailored to the specific needs of their clients. With a focus on quality and innovation, HeadPowder provides solutions that enhance productivity and safety in powder handling applications. Whether for food, pharmaceutical, or chemical industries, these systems offer a reliable and cost-effective way to manage bulk materials.




